Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Application
Aluminum Intake Manifold Casting
An intake manifold casting RFQ should define the runners, core geometry, flange datums and finished ports together. Bohua has 10 hot-box core shooting machines and 16 vertical machining centers. Use those manufacturing capabilities as the starting point for a drawing review, with machining, cleanliness and approval requirements stated separately. Bohua's quality management system is certified to IATF 16949:2016 by NQA.
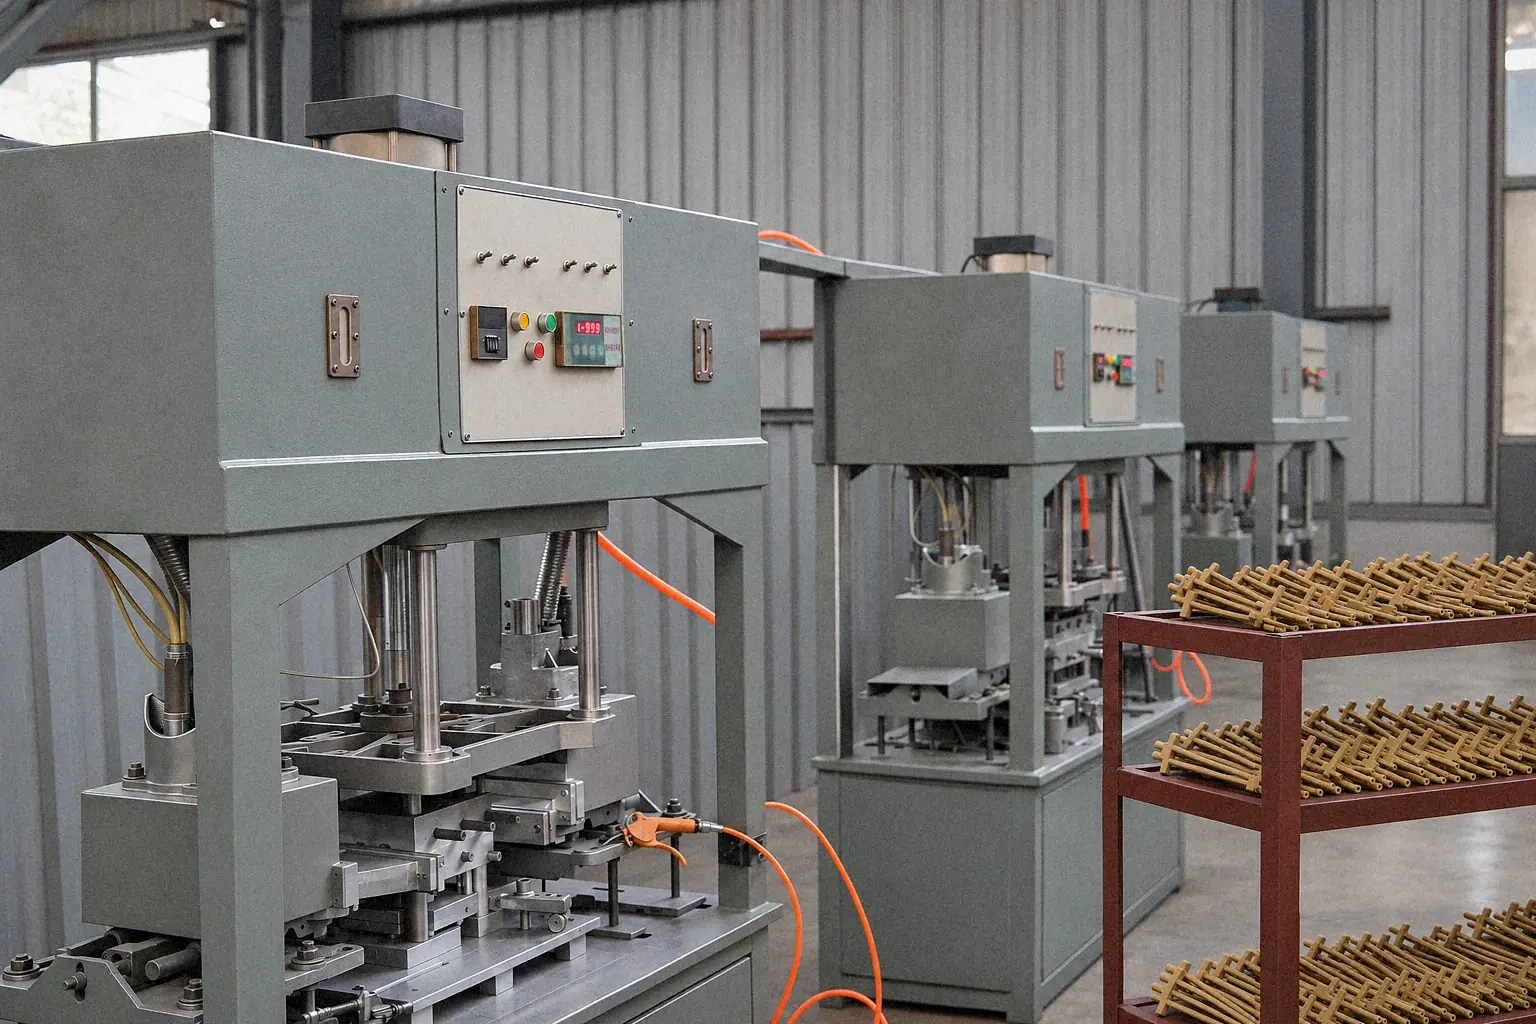
Connect the manifold drawing to factory capabilities
Define the internal passages and finished interfaces before selecting the casting route. Include the manifold's assembly context, mating parts and required delivery condition.
At Bohua
Our factory operates 32 tilt-pour machines and 10 vertical gravity casting machines. Bohua has 10 hot-box core shooting machines, and some tilt-pour castings use sand cores for internal cavities. Our machining equipment includes 16 vertical machining centers.
Bohua works with A356 and ZL114 for gravity and tilt-pour casting. T5 and T6 heat treatment are completed in-house. The material and temper for your manifold must follow its approved specification.
Review our gravity casting manufacturing scope against the runner layout, core-access constraints, machining stock and annual demand. Send your finished manifold specification so we can confirm how these operations fit your drawing.

Specify runner geometry and core risks
Provide sections through the runners so the passage geometry and wall requirements can be reviewed together.
- Mark long passages, sharp turns, intersections and walls where core movement would affect function.
- Identify minimum wall requirements and areas where thinning is unacceptable. State the dimension units.
- Show core-access and removal constraints, plus any areas that cannot be reached for cleaning or inspection.
- State which internal discontinuities would affect sealing, flow or mechanical function.
- Request a proposed wall and core-position verification method, with the inspection locations, sampling plan and acceptance criteria.
If flow or pressure validation is required, define the test conditions and who supplies the evidence. Keep dimensional inspection and functional validation as separate items, with the required evidence and responsibility defined for each.
Separate flanges, ports and threaded interfaces
Mark each machined feature and its inspection datum. State whether a requirement applies as cast, after heat treatment, after rough machining or after final machining.
| Feature | Drawing input | Evidence to request |
|---|---|---|
| Flanges and gasket faces | Flatness, surface finish, mating seal, machining stock and measurement condition | Named flatness or profile checks tied to the final datum scheme |
| Ports and mounting holes | Position, bore requirements, bolt pattern and relationship to primary, secondary and tertiary datums | Feature-specific dimensional report and agreed fixture setup |
| Sensor bosses | Location, height, depth, sealing detail and machining access | Separate checks for the boss, bore and sealing interface |
| Threads | Standard and edition, designation, class, full thread depth, sealing method and any coating allowance | Gauge type and class, go/no-go rule, inspection frequency and result summary |
| Runner interfaces | Cast-to-size or machined condition, stock allowance and core-position relationship | Agreed checks linking casting geometry to the finished interface |
Separate sealing threads from fastener threads. State whether inserts are required. Define the disposition of damaged threads and any permitted rework. Ask for clamping assumptions where a fixture could distort the flange.
At Bohua
Dimensional inspection equipment includes Hexagon Global S and NANO Metrology coordinate measuring machines.
For the wider machining scope, see aluminum casting and CNC machining.

Define burr removal and internal cleanliness
State what must be removed from the passages after machining and how cleanliness will be accepted.
- Define edge breaks and permitted burr condition at ports, threads and internal intersections.
- State whether washing and drying are required, with the cleanliness method, limits and sampling plan.
- Specify how loose chips and core residue are assessed. Request the proposed method if the cleaning process is not prescribed.
- Define caps, plugs, separators or sealed packaging needed to protect clean passages and machined faces.
- Include lot and revision labeling requirements, plus any corrosion-protection restrictions.
Keep the cleaning method, verification records and packaging scope visible in the quotation. Ask us to confirm which cleaning, verification and packaging requirements are included before you approve the quotation.
Agree the inspection and approval package
Specify the records needed to accept the manifold, including the features measured and the condition in which they are measured.
At Bohua
Inspection equipment includes an Oxford optical emission spectrometer and Unicomp UNC-160 and Y.MU2000-D X-ray systems. PPAP submissions are available up to Level 5 according to project requirements.
- Material: alloy, temper, governing specification and edition, plus required chemistry and heat-treatment records.
- Dimensions: flange flatness, port relationships, sensor boss locations, mounting pattern and datum relationships.
- Internal quality: critical zones, method, acceptance reference and inspection frequency.
- Approval: first-article inspection (FAI) scope, sample quantity, PPAP level if required, record format and release authority.
State whether leak testing is required. If it is, provide the medium, pressure, hold time, acceptance rule and test stage. Define flow-validation responsibility separately. Review the factory inspection equipment and quality-control scope before selecting the required checks.
Use one checklist for truck and passenger manifolds
Truck, diesel, and passenger-vehicle intake manifolds use this same input list. Name the engine interface on the drawing. A catalog alloy and temper is a reference until the approved drawing and its specification edition replace it.
State whether the quote is for a prototype, a pilot build, serial production, or a second source. Ask the quote to separate mold or core-box corrections from CNC-program corrections, and to list the stock allowance assumed on flange faces and ports.
For a coolant passage, use the coolant water outlet review.
Send one complete manifold RFQ package
Send the same drawing revision and delivery scope to each supplier so the manufacturing proposals can be compared.
- Files and purpose. Provide the 2D PDF, 3D model, separate casting and machining drawings if available, and whether the request concerns samples, a new program or a second source.
- Tooling and fixtures. Identify new, duplicate or transferred tooling. Include core boxes, ownership, fixture timing, sample quantities, correction responsibility and approval stages.
- Delivery requirements. State annual demand, batch pattern, target sample and launch timing, destination, delivery terms and protective packaging.
- Quote assumptions. Ask for separate casting, machining, cleaning, inspection and tooling scope. Require exclusions and unresolved drawing inputs to be listed.
Use the casting RFQ form for your package. For general qualification criteria, use the casting supplier evaluation checklist. Browse aluminum casting applications for another component family.
Send your manifold drawing for a passage and flange review
Share the passage geometry, flange interfaces, machining scope and annual volume. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →