Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering resource
Aluminum Casting RFQ Checklist
A useful aluminum casting RFQ defines one controlled part, one supply boundary, and the evidence needed for acceptance. Send the current drawing and model revisions, annual volume, material and temper, casting and machining scope, critical features, inspection requirements, packaging, and approval milestones. Mark every unresolved input as an open assumption with an owner.
On this page
- Start with the minimum package
- Complete one scope worksheet before comparing quotes
- Separate the casting boundary from the finished-part boundary
- Define the evidence, not just the test name
- State what kind of quotation the package can support
- Use Bohua-specific facts when screening fit
- Protect machined surfaces in the packing plan
- Remove these common RFQ gaps
Start with the minimum package
A supplier can begin a useful review when the package identifies the controlled geometry, the required material or performance, and the expected demand. Everything else should either be defined or listed as an open assumption.
- Controlled files. List the 2D drawing, 3D model, revision, issue date, and which file controls if they do not match.
- Part function. State whether the part carries pressure, locates bearings, transfers structural load, manages heat, provides a cosmetic surface, or forms a sealing interface.
- Material basis. Name the alloy, governing specification and version, temper or delivery condition, permitted equivalents, and required evidence.
- Demand. Give annual volume, first order quantity, program stage, and expected ramp pattern. A range is acceptable if the forecast is not fixed.
- Supply boundary. Say whether the quote is for an as-cast blank, a semi-machined casting, or a finished part with treatment, inspection, and packing.
For file-level guidance, use the casting drawing requirements. If the manufacturing route is open, attach the same inputs and use the casting process selection guide.
Save or forward this checklist: Aluminum casting RFQ checklist (PDF).
Download the fillable aluminum casting RFQ checklist (CSV) and enter your project details in the blank Buyer input column, using the instructions and examples for each field.
Complete one scope worksheet before comparing quotes
Use the worksheet to ask every supplier to quote the same delivered scope. Put unclear items in an open-assumption list rather than allowing different defaults to remain hidden.
| RFQ field | Buyer input | Why it changes the quote |
|---|---|---|
| Part and revision | Part name, drawing revision, model revision, issue date, design status | Fixes the geometry and notes being reviewed |
| Function and risks | Load path, fluid or pressure boundary, sealing faces, bearing seats, thermal or cosmetic zones | Directs DFM and inspection attention to functional features |
| Material | Alloy, governing standard and edition, temper, allowed equivalent, certificate needs | Defines chemistry, condition, and evidence |
| Quantity | First order, annual volume range, program stage, ramp assumptions | Influences process and tooling decisions |
| Casting scope | Preferred route or supplier recommendation, cores, heat treatment, cleaning | Prevents unlike process assumptions from being compared |
| Machining scope | Datums, bores, ports, threads, faces, grooves, stock, fixture ownership | Defines operations, setups, and dimensional evidence |
| Surface and assembly | Coating, masked zones, finish state, inserts, cleaning, protection | Fixes the delivered condition |
| Inspection | Method, acceptance basis, sampling, report format, approval owner | Defines the evidence included in the quote |
| Delivery | Destination, Incoterm, packing, labeling, shipment documentation | Makes logistics assumptions visible |
Separate the casting boundary from the finished-part boundary
A raw-casting quote and a finished-part quote are not comparable. Mark every machined feature and state the inspection condition: as cast, after heat treatment, after machining, after coating, or at final delivery.
- Identify primary, secondary, and tertiary datums on the controlled drawing.
- Mark bearing seats, sealing lands, gasket faces, O-ring grooves, bores, ports, and threads.
- State machining stock where it is controlled and identify dimensions checked before and after CNC.
- Define whether tooling, casting fixtures, CNC fixtures, gauges, and checking fixtures are included and who owns them.
- List heat treatment, impregnation, coating, assembly, cleaning, labeling, and packing as separate scope items.
At Bohua
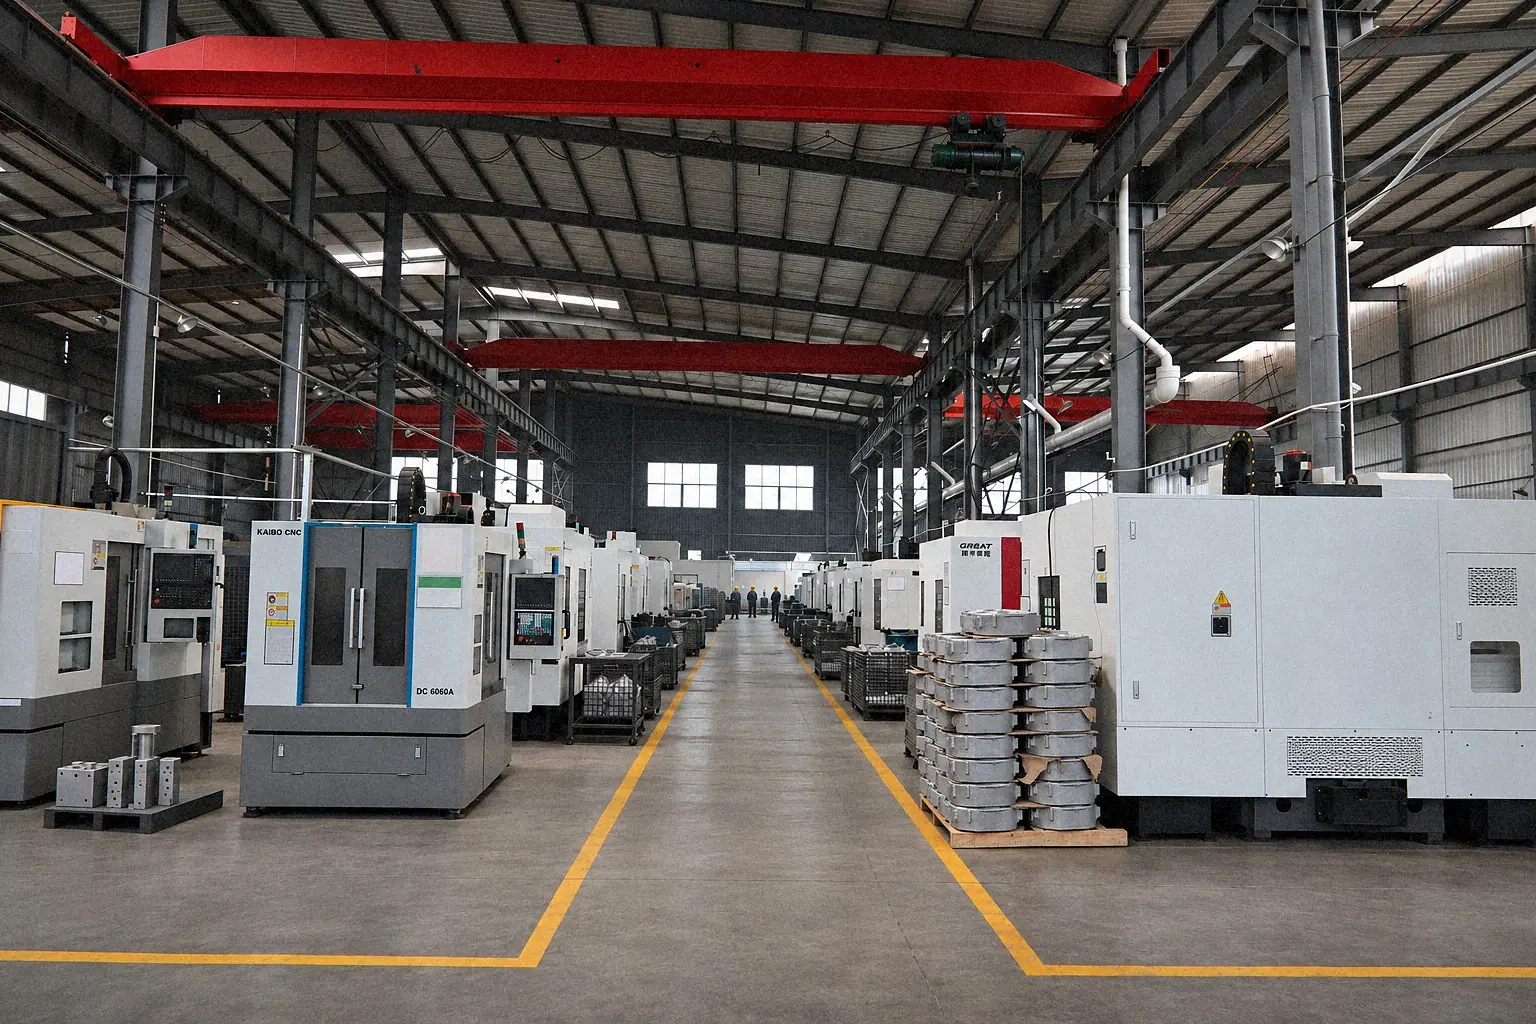
T5/T6 heat treatment and CNC machining are performed in-house. The machining department has 16 vertical machining centers, 2 CNC engraving and milling machines, 22 CNC lathes, and 2 large lathes. List the operations and records you need in the delivered scope so we can review what to include in your quotation.
Define the evidence, not just the test name
Each inspection line needs a risk, method, acceptance basis, stage, sampling rule, record, and disposition authority. List those details under “Inspection report required” so each supplier quotes the same inspection coverage and records.
| Evidence | Buyer should define |
|---|---|
| Material | Alloy and temper specification, lot basis, chemistry or property evidence, and certificate format |
| Dimensional | Drawing revision, datum scheme, ballooned features, method, stage, sampling, and report format |
| Radiography | Drawing zones, governing standard and edition, reference severity, technique, sampling, and disposition |
| Leak or pressure test | Medium, pressure basis, duration or cycle, leakage acceptance, test stage, sampling, and record |
| Surface | Functional and cosmetic zones, finish requirement, coating checks, visual reference, and handling protection |
| Approval package | FAI or PPAP level, customer forms, sample quantity, submission timing, approval owner, and resubmission rule |
At Bohua
PPAP support is available through Level 5. Dimensional inspection equipment includes Hexagon Global S and NANO Metrology CMMs, and internal inspection includes Unicomp UNC-160 and Y.MU2000-D X-ray systems. Air-under-water immersion testing is available at 3 bar or more. The project drawing and customer specification must still define the method, acceptance criteria, and sampling.

Use the Bohua quality control and inspection page to check available methods before writing the evidence list.
State what kind of quotation the package can support
Label a preliminary package for feasibility review and list the decisions still open. Release the production basis after the required approval gates are complete.
- Close quotation questions. Record supplier assumptions and exclusions against the controlled revision.
- Approve process and tooling design. Name the buyer and supplier outputs at the gate.
- Approve first-part evidence. Define samples, reports, deviations, correction, and resubmission.
- Release production. Confirm the approved revision, packaging, labeling, and shipment records.
Use Bohua-specific facts when screening fit
Bohua quotes by annual volume, and small batches are negotiable. For gravity and tilt-pour projects, Bohua works with A356 and ZL114. Mold design and manufacture are in-house, using UG and SolidWorks for design and AnyCasting for simulation.
- Quotation volume basis
- Annual volume
- Gravity and tilt alloys
- A356 and ZL114
- PPAP support
- Up to Level 5
- Confirmed drawing to first part
- 5–6 weeks
The 5–6 week figure applies from confirmed drawing to the first part for Bohua's in-house mold route. It is not a complete production or shipping schedule. Ask the quotation to name dependencies and approval owners.
Protect machined surfaces in the packing plan
For machined castings, mark sealing faces, bores, threads, and open passages that must not be used as stack supports. A part can pass inspection and still arrive damaged if the pack loads those surfaces.
- State whether caps or plugs are required, how they stay in place, and that a transport plug is not a pressure-rated closure unless the drawing says so.
- Record the cleaning and drying state before packing, including residual liquid in internal passages. A wrap does not show that the part is clean.
- Do not treat a sample pack as the production pallet plan. Compare part count, mass, orientation, supports, and stacking before reusing the sample arrangement.
- If oil or a corrosion inhibitor is proposed, require approval for the alloy, the finish, and the next process. Do not add it to every machined order by default.
- Ask how the pack addresses moisture on the planned route. A closed bag alone does not show that moisture is controlled. Put any numerical damage limit on the drawing for that part.
For housings with several openings, map every temporary closure so receiving knows what to remove. Use the pump housing page or the valve body page when the part boundary is a pump or valve housing.
Remove these common RFQ gaps
Before sending the package, check that another reviewer can tell exactly what is controlled and what remains open.
- No annual volume or project stage, leaving tooling and process assumptions unaligned.
- A material family without a governing specification, temper, or evidence requirement.
- A 3D model without a 2D source for tolerances, GD&T, finishes, and acceptance notes.
- Every dimension marked critical, with no priority for functional interfaces.
- No part function, leaving pressure, structural, thermal, sealing, or cosmetic risks invisible.
- Machining, treatment, inspection, or packing added after suppliers have priced different boundaries.
- A test name without method, acceptance basis, sampling, report, or disposition rule.
If a failure mode is already known, such as porosity at a sealing face or distortion after heat treatment, name it so every supplier quotes the same inspection assumption.
If the inspection set is not decided, ask for two named scenarios, such as basic records and an enhanced record set, instead of letting each supplier choose a different default.
For an application-specific example, the automotive suspension bracket RFQ guide shows how manufacturing scope and evidence should follow the part. Return to all aluminum casting buyer resources for drawing, process, and supplier-evaluation guides.
Send a controlled RFQ package
Include the current revision, annual volume, finished-part scope, critical features, and required records. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →