Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Alloy
Aluminum-Silicon-Copper Die Casting Alloy
ADC12 is commonly considered for thin-wall housings and covers made by high-pressure die casting. This page provides general material and RFQ guidance. Bohua uses A356 and ZL114 for gravity and tilt-pour casting. At Bohua, die-casting alloys follow the customer's specification, and ADC12 is a common choice.
Why ADC12 is so widely specified
ADC12 fills thin sections well, reproduces die detail consistently, and supports efficient cycle times. That combination makes it commercially attractive when buyers need stable geometry at high volume.
The trade-off is that ADC12 is not the right alloy for every part. It is usually chosen for non-structural or semi-structural die castings, not for T6 heat-treated safety parts. For material qualification questions, review the ADC12 material evidence and RFQ guide.
This is general ADC12 selection guidance. At Bohua, A356 and ZL114 are used for gravity and tilt-pour casting. Die-casting alloys follow the customer's specification, and ADC12 is a common choice on Bohua's 280 t and 450 t die-casting machines.
The following factors describe conventional high-pressure die-casting selection. Geometry, service requirements and the complete manufacturing scope still need engineering review. A heat-treatable alternative also needs validation against the drawing.
| Decision factor | ADC12 fit |
|---|---|
| Thin-wall geometry | Excellent fluidity helps fill complex die-cast sections. |
| High annual volume | Very good for programs that need fast cycles and low unit cost. |
| Heat treatment requirement | Poor fit; use A356 or ZL114 instead if T6 is required. |
| Weldability | Limited compared with structural casting alloys. |
| Surface finish and repeatability | Strong fit for stable die-cast cosmetic and dimensional performance. |
Typical uses
Automotive covers, motor housings, appliance parts, telecom enclosures, industrial covers.
Buyer caution
Do not specify ADC12 just because it is cheaper if the part truly needs fatigue strength or T6 heat treatment.
Machining logic
ADC12 machines well for threaded holes, sealing faces, and datum cleanup after casting.
Mark machining stock and surfaces where exposed porosity would affect function. Compare alternatives in the A356 versus ADC12 alloy and process guide.
ADC12 composition and material evidence
Use the controlled material specification for acceptance; the two composition ranges below only identify the alloy family.
| Element | Reference range (mass %) |
|---|---|
| Silicon, Si | 9.6–12.0 |
| Copper, Cu | 1.5–3.5 |
Source: JIS H 5302:2006, Table 2.
Use these selected limits to identify the alloy family. For acceptance, request the complete specification and the actual batch analysis. Identify the standard and edition required by the order, all controlled elements and customer amendments. Require lot-linked chemical analysis. Do not approve ADC12Z, A380 or another designation solely from a comparison table.
Keep tensile strength, elongation, hardness and thermal data attached to their material condition, test method and specimen source. Specify whether the required properties apply to a separately prepared specimen, a rib, or a machined wall. Assess pressure tightness through its agreed test, separately from chemical conformance.
Material decision evidence
Resolve the specification, geometry and acceptance plan before releasing tooling.
What to verify before releasing an ADC12 tooling order
Confirm the required JIS, customer, or equivalent alloy specification and do not substitute ADC12 for a heat-treatable structural alloy without engineering approval.
- Confirm annual volume, wall sections, cosmetic zones, draft, and tool-life assumptions.
- Separate as-cast tolerances from machined critical features, sealing faces, threads, and datum requirements.
- Define porosity-sensitive zones, X-ray or leak-test scope, surface finish, and approval records before quotation.
CTQs are critical-to-quality features identified on the drawing. Add nominal and minimum walls, local thick sections, rib transitions and acceptable parting-line locations. Define side actions, undercuts, inserts, ejector-mark restrictions and areas reserved for later tool correction. Ask for main die, slides, inserts and sample-correction scope to be itemized separately.
For machining, identify thread requirements, bores, sealing lands, datums, gate removal and deburring. For finishing, define the coating, masking, cosmetic acceptance zones, surface preparation and packaging protection. Approve a representative finish sample under the agreed acceptance criteria. See the casting surface-finishing requirements for that separate decision.
Factory capability for ADC12 die casting
Use the die-casting and inspection equipment below to prepare your process questions. Die-casting alloys follow the customer's specification, and ADC12 is a common choice.
At Bohua
The factory has two die-casting machines: one rated at 280 t and one at 450 t. Die-casting alloys follow the customer's specification, and ADC12 is a common choice. A356 and ZL114 are used for gravity and tilt-pour casting.
| Approval checkpoint | Available factory evidence and RFQ boundary |
|---|---|
| Alloy identity | Oxford OES capability; require the applicable material certificate and chemistry limits in the RFQ. |
| Internal soundness | Unicomp UNC-160 and Y.MU2000-D X-ray capability; critical zones and acceptance criteria remain project-defined. |
| Machined geometry | Hexagon Global S and NANO Metrology CMM capability; define datums, CTQs, sampling, and report format. |
| Approval records | PPAP documentation can be provided up to Level 5 according to project requirements. |
OES means optical emission spectrometry; CMM means coordinate measuring machine. Request a project-specific inspection plan and actual results for qualification. Include the material certificate and lot-linked analysis in the evidence you request for approval.
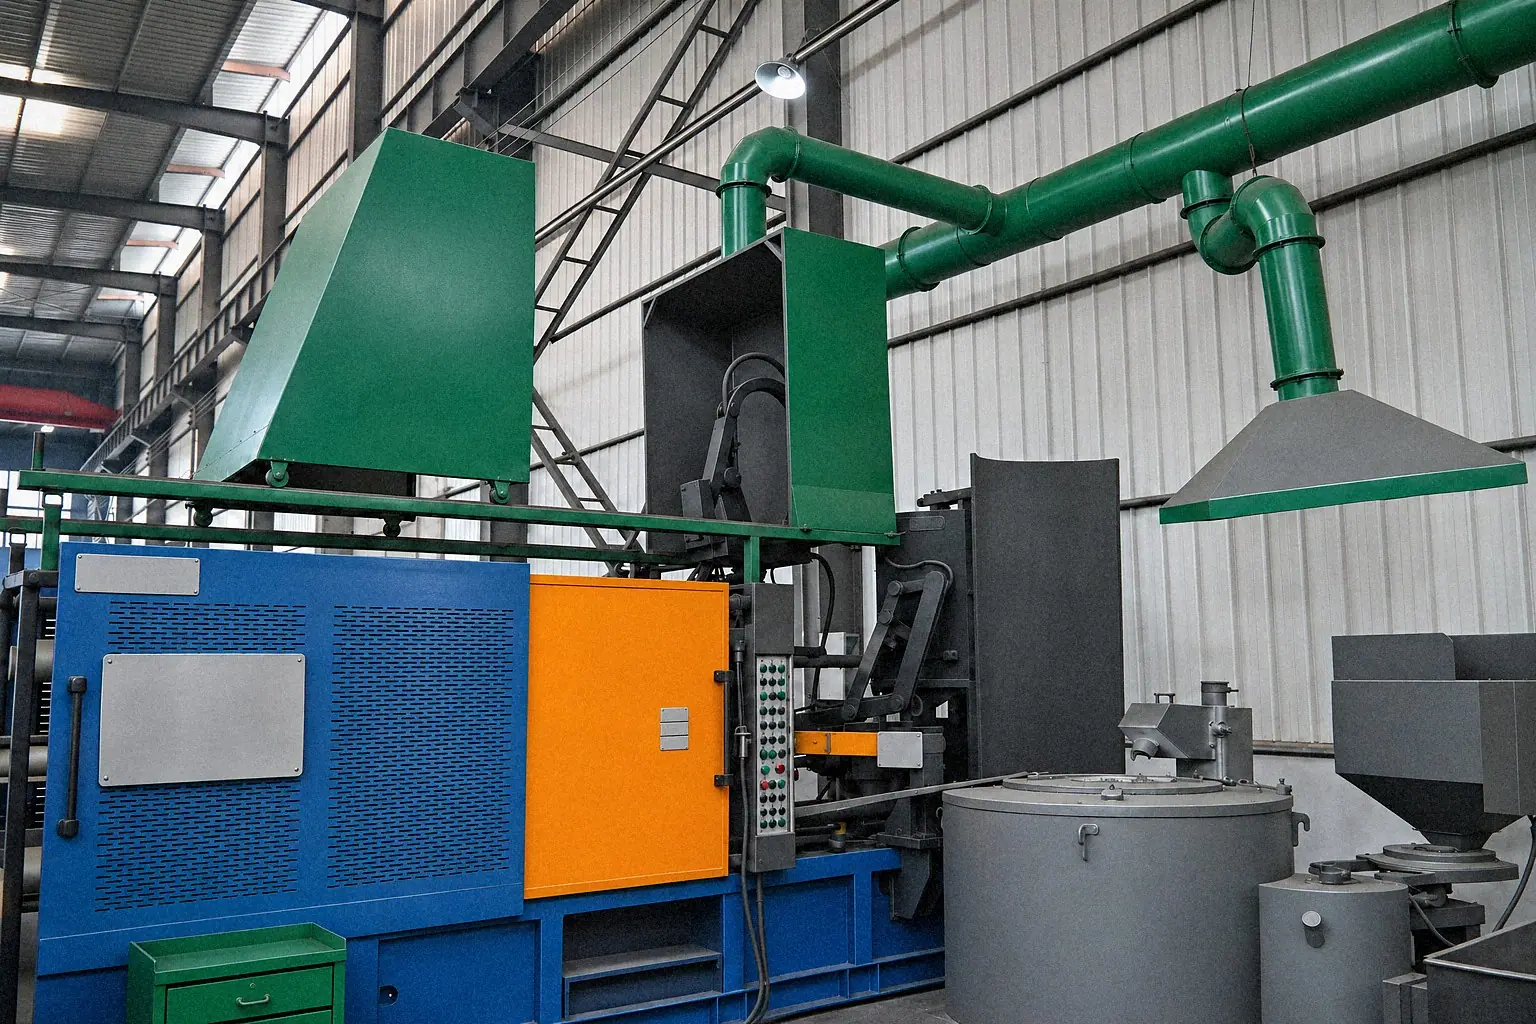

See Bohua die-casting equipment and project inputs, inspection capability and Bohua material scope.
Heat-treatment limits depend on the casting route
Do not specify a conventional ADC12 die casting as though it were an approved A356-T6 casting.
Entrapped gas can expand during solution heat treatment and cause surface blistering. Specialized casting routes and validated thermal cycles can change that constraint. For a Bohua inquiry, confirm whether the proposed alloy and thermal route are available before planning qualification. Require evidence for the exact alloy, casting process and finished-part duty before approval.
Technical basis: Vacuum assisted high pressure die casting of aluminium alloys (2000). The study explains process-dependent porosity and blistering. Use it to frame qualification questions for the proposed ADC12 production route.
For a heat-treatable gravity-casting alternative, review A356 manufacturing and material acceptance requirements. Carry over the required service loads and inspection criteria when evaluating any substitution.
ADC12 FAQ
These answers describe general selection considerations for conventional die casting. Use them to prepare the component validation questions you need to resolve with your supplier.
What is ADC12 aluminum alloy?
ADC12 is a high-silicon aluminum die casting alloy widely used for housings, covers, brackets, and thin-wall parts. It offers strong fluidity, stable die filling, and competitive cost for high-volume production.
When should buyers choose ADC12?
ADC12 is usually the right choice when a part will be high-pressure die cast, annual volume is high, walls are thin, and the part is not a heat-treated structural component.
This is an initial selection rule. Confirm geometry, service duty, tooling, machining and inspection before approving the route. Annual volume alone is not sufficient.
Can ADC12 be T6 heat treated?
ADC12 is generally not suitable for T6 heat treatment because porosity and alloy chemistry make solution treatment risky. If T6 strength is required, A356 or ZL114 with gravity or low-pressure casting is a better route.
This caution applies to conventional die-casting selection. Any alternative still requires approval of its complete material specification and test plan. The route comparison is general engineering guidance, not a statement of Bohua's alloy-specific low-pressure production.
What tolerances and wall thicknesses are realistic for ADC12?
Final tolerance still depends on tool quality, part size, gating, and whether critical features are machined after casting.
Submit the wall map and flow lengths for review. Review the nominal minimum wall together with local thick sections and flow lengths to assess filling across the entire component.
What industries commonly use ADC12?
ADC12 is common in automotive housings, electrical enclosures, appliance parts, telecom housings, and industrial covers where dimensional repeatability and productivity matter.
Prepare an ADC12 material and process review
Provide the material requirement and full manufacturing scope so a supplier can assess feasibility before a tooling commitment.
| Input | Include in the request |
|---|---|
| Files and material | Matching PDF/STEP revisions, full alloy designation, standard edition, delivery condition and substitution rules |
| Tooling | Wall map, draft, slides, inserts, ownership, sample corrections and approval milestones |
| Machining and finish | Threads, bores, sealing surfaces, datums, cleanup, coating, masking and cosmetic acceptance |
| Validation | Material analysis, first-article dimensions, functional tests, sampling and report formats; X-ray only where justified |
| Supply plan | Sample quantities, annual demand, release pattern, packaging, destination and delivery terms |
Use the full casting RFQ checklist to organize your files, then request a drawing-based casting review. If the drawing names ADC12, treat that callout as the buyer's specification; Bohua die-casts to the specified alloy.
Send your drawing and material specification
Include the required alloy, delivery condition, annual demand and acceptance criteria.
Send your drawing →