Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Casting process
Low-Pressure Casting
Bohua has performed low-pressure aluminum casting in-house since 2014. Send the drawing, material requirements, annual volume and acceptance criteria to assess the route for your part. Include internal passages, sealing interfaces and machining requirements. We review the geometry and required evidence together. Specify the leak-test conditions and acceptance criteria to verify pressure tightness.
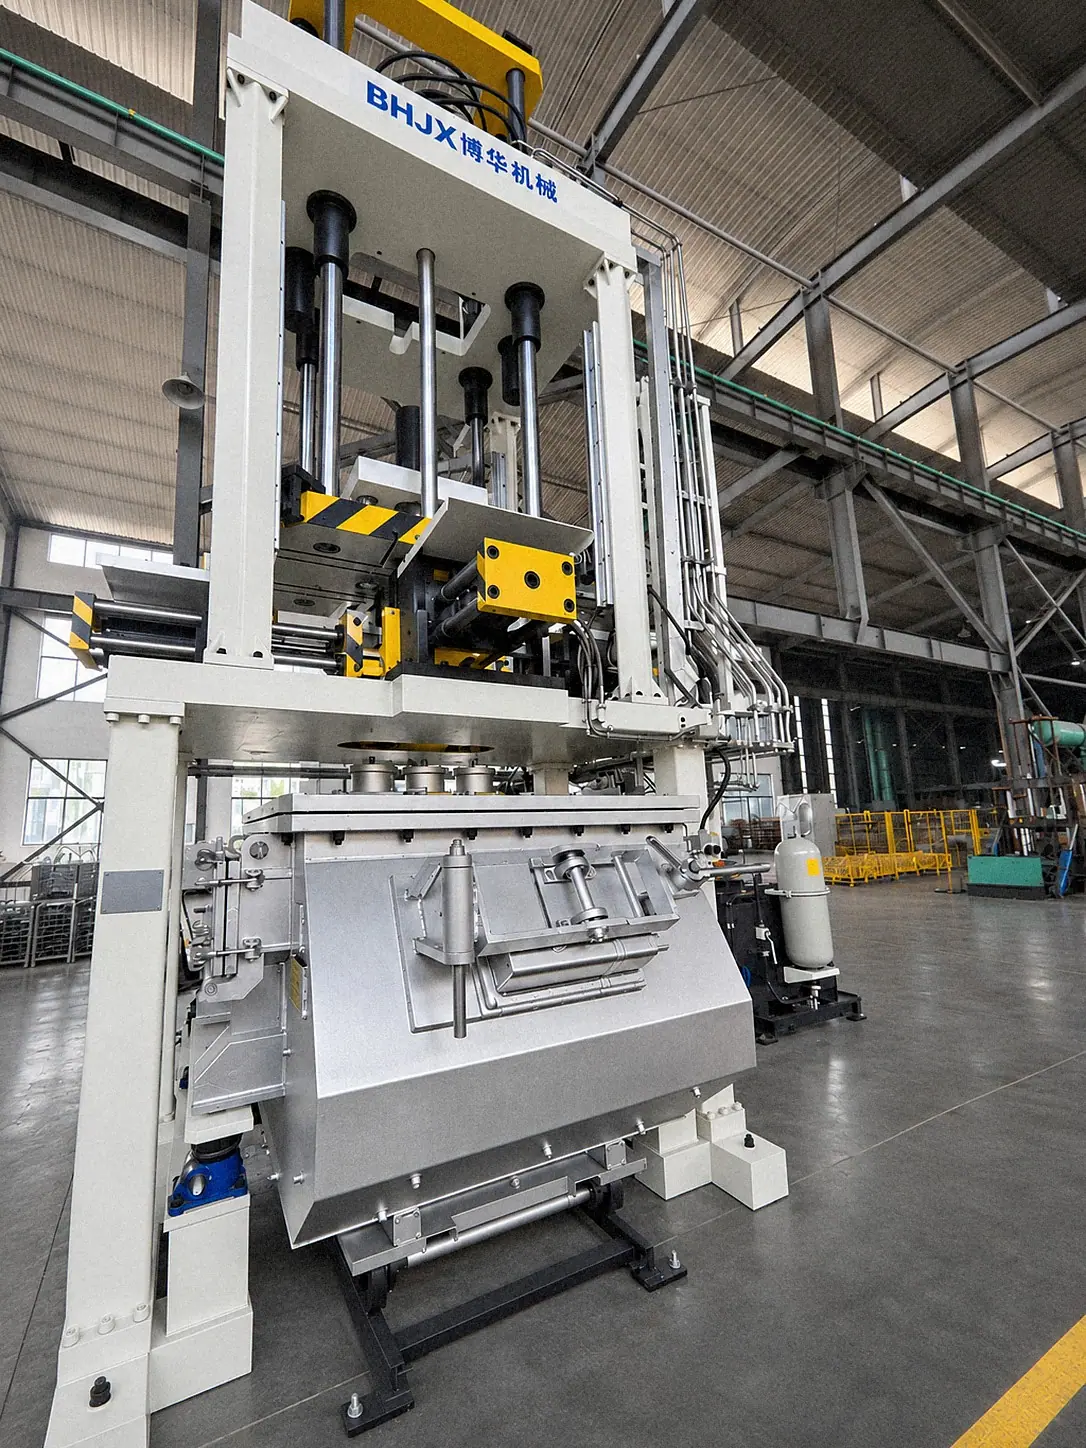
Established in-house low-pressure casting
Low-pressure casting has been an established in-house process at Bohua since 2014.
At Bohua
- Low-pressure casting is performed in-house.
- Molds are designed and made in-house.
- T5 and T6 heat treatment are performed in-house.
- Casting, mold making, heat treatment, CNC machining and inspection share our site of about 16,300 m².
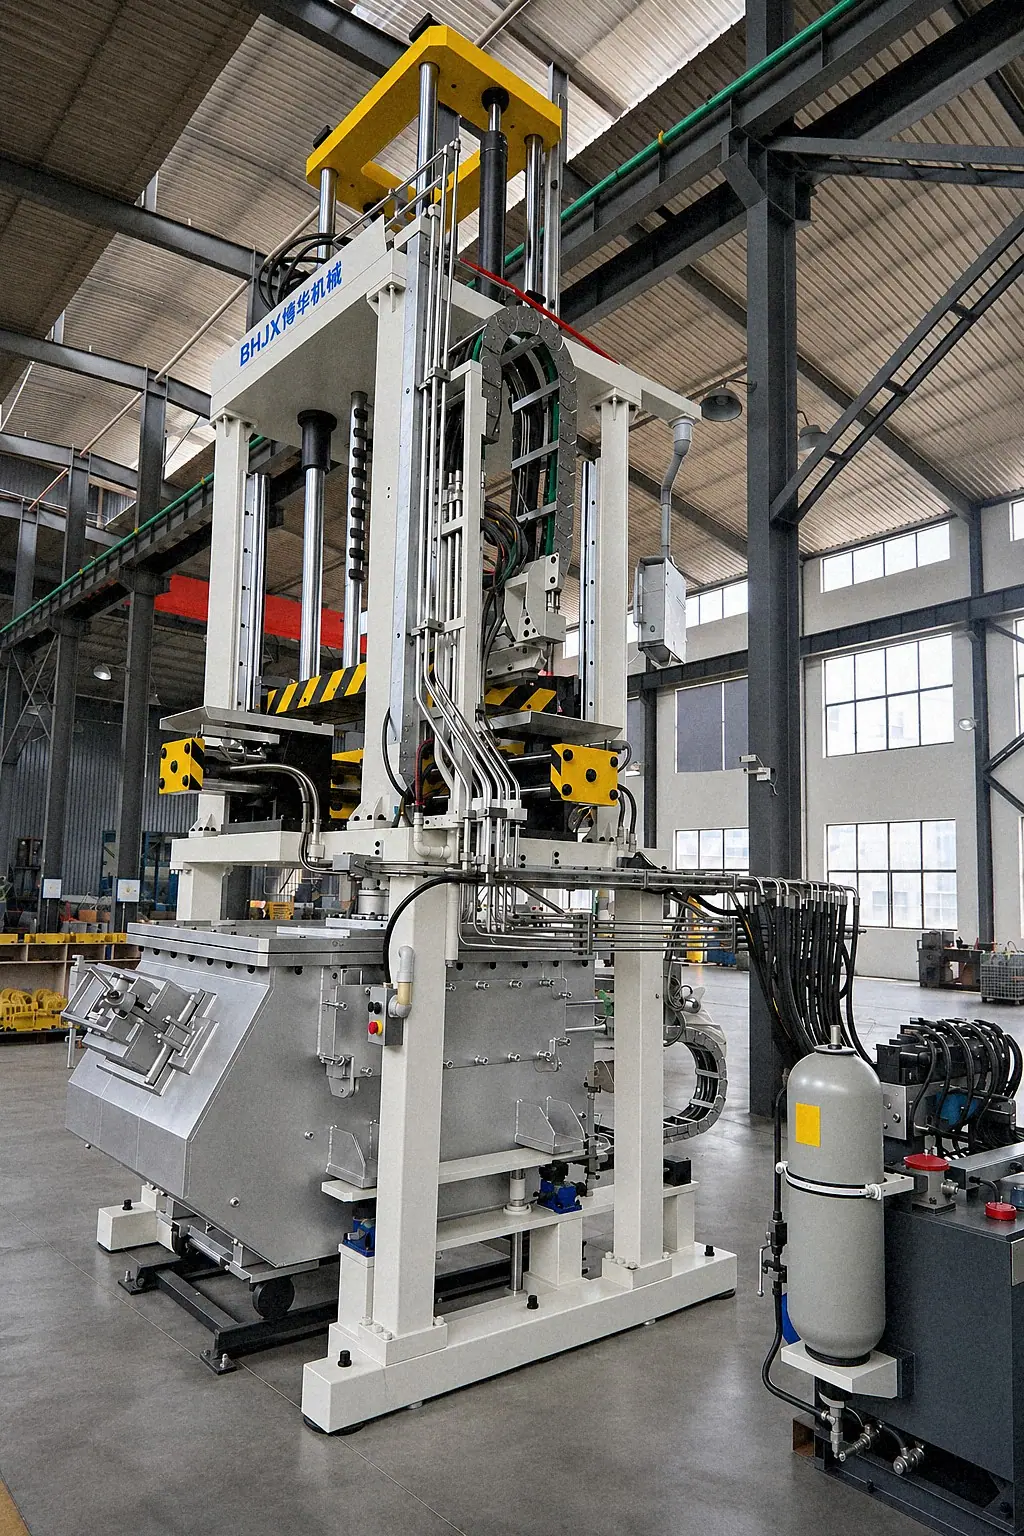
Our main focus is gravity and tilt-pour casting. See the casting processes available at Bohua and the tilt-pour gravity casting capability for other routes.
When low-pressure casting is worth reviewing
Low-pressure casting may be reviewed when controlled bottom filling and feeding suit the geometry and pressure-boundary requirements.
In general, this permanent mold process uses gas pressure to move molten metal upward into the cavity. The drawing review must address filling, feeding, internal passages and the surfaces exposed by machining.
Check internal soundness and leak tightness through part-specific inspection and testing. Compare the proposed route using drawing-specific samples, machining exposure, inspection zones and acceptance criteria.
| Requirement | Information to supply | Decision it supports |
|---|---|---|
| Geometry | Released drawing, 3D model and sections through internal passages | Mold arrangement, filling access and core requirements |
| Pressure boundary | Sealing faces, test method, pressure, hold time and acceptance criteria | Inspection scope and sample acceptance |
| Material condition | Required alloy, temper and mechanical properties | Material and heat-treatment suitability for the part |
| Finished interfaces | Machining datums, sealing-face flatness and surface roughness requirements | Machining stock and dimensional inspection |
| Existing tooling | Mold drawings, connection details, condition and ownership | Equipment compatibility and modification scope |
For a route comparison, use the low-pressure and gravity casting comparison. For a cooling-system component, see the coolant water outlet manufacturing scope and RFQ inputs.
Include machining and delivery condition
Define the delivered condition together with the casting requirement.
At Bohua
Our machining workshop includes 16 vertical machining centers, 22 CNC lathes and 2 large lathes. T5 and T6 heat treatment are available in-house; the required material condition must be specified for the project.
Separate as-cast dimensions from machined dimensions. Mark datum features, threaded ports, sealing faces and any surfaces that must remain unmachined. State whether dimensional acceptance applies before or after heat treatment and final machining.
See the casting and CNC machining scope for the supporting operations.
Specify how the part will be accepted
Mark the inspection zones on your drawing and specify the acceptance criteria for each zone.
At Bohua
Inspection equipment includes an Oxford optical emission spectrometer, X-ray systems, and Hexagon Global S and NANO Metrology coordinate measuring machines. Leak testing uses air-under-water immersion, with capability at 3 bar or more. The pressure and hold time for a particular part must be agreed against its requirements.

Specify the sampling basis, required records and inspection stage. Identify internal-inspection zones and areas exposed by machining. For pressure testing, identify the sealed openings and the acceptance criterion. Use the inspection results for your component to confirm whether it meets the agreed acceptance criteria.
Review the inspection equipment and quality-control scope, then submit a low-pressure casting RFQ with the drawing revision, annual volume, sample quantity and delivery scope.
Send a drawing for a low-pressure casting review
Include the alloy, annual volume, machined interfaces and inspection requirements. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →