Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Casting process
Aluminum Gravity Casting
Bohua offers aluminum gravity casting in A356 and ZL114, with 10 vertical gravity casting machines and 32 tilt-pour machines. Molds, T5/T6 heat treatment and CNC machining are handled in-house. Send the drawing, annual volume and acceptance requirements to assess the casting route and the scope of the finished part.
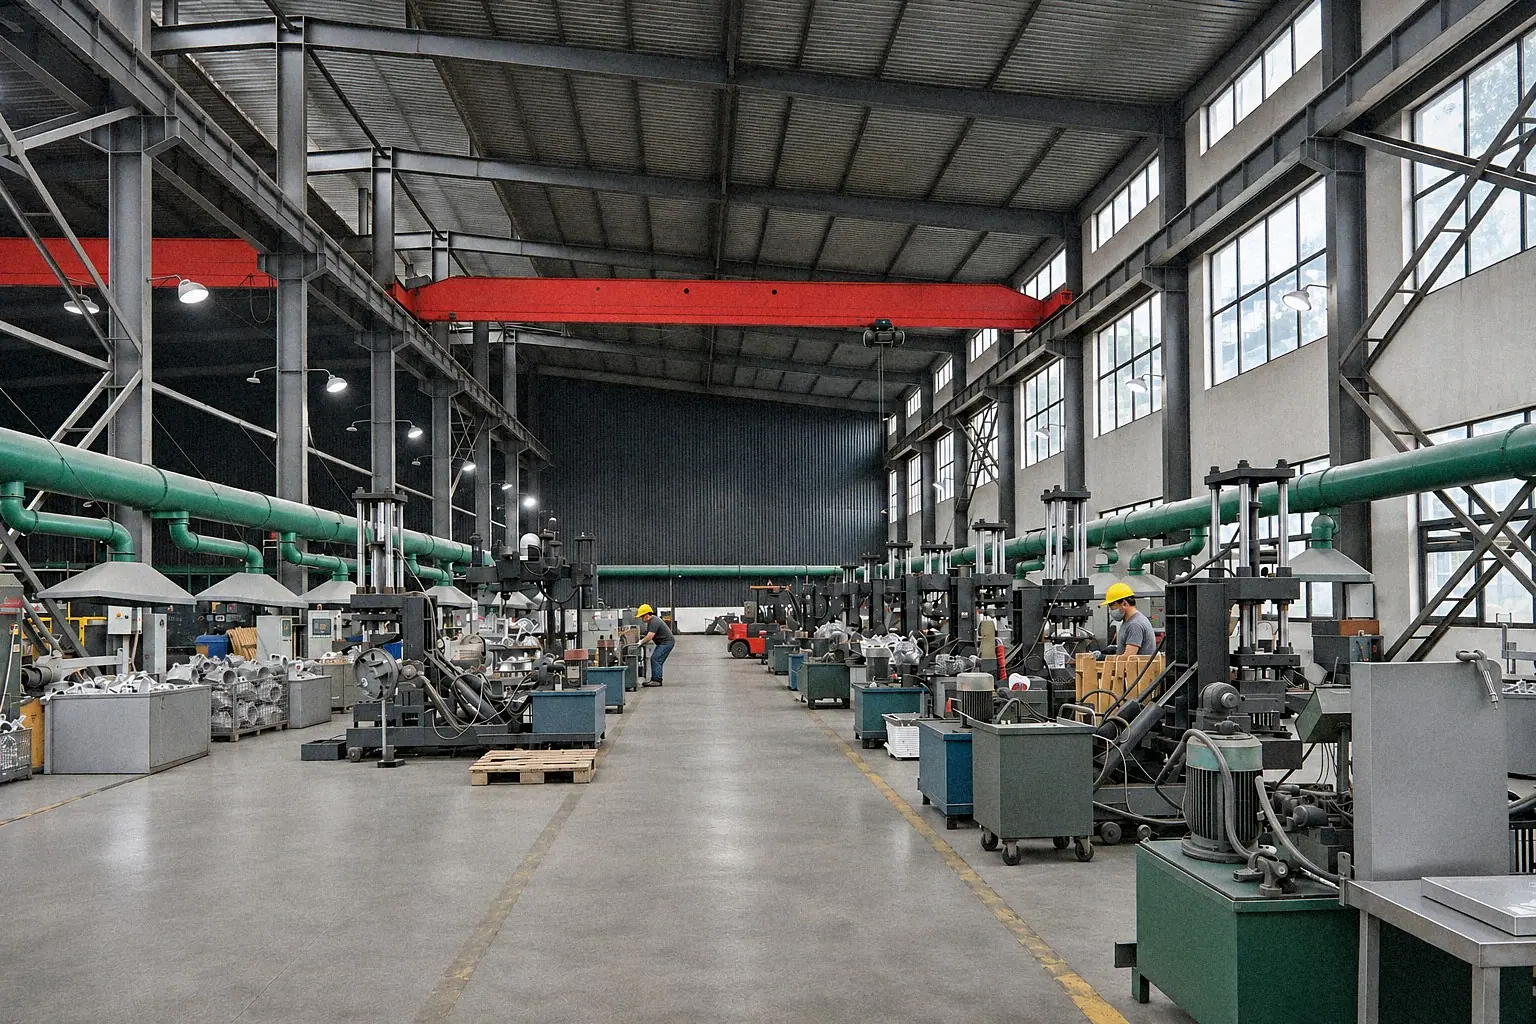
Gravity casting equipment at Bohua
At Bohua, gravity casting is a core process, supported by 10 vertical gravity casting machines and 32 tilt-pour machines.
At Bohua
Some of the tilt-pour machines were designed and built in-house. The plant also has 10 hot-box core shooting machines. Some tilt-pour castings use sand cores.
- Vertical gravity casting machines
- 10
- Tilt-pour machines
- 32
- Hot-box core shooting machines
- 10
For the rotating mold route and its equipment limits, see tilt-pour gravity casting. Compare the other in-house routes in the casting processes overview.
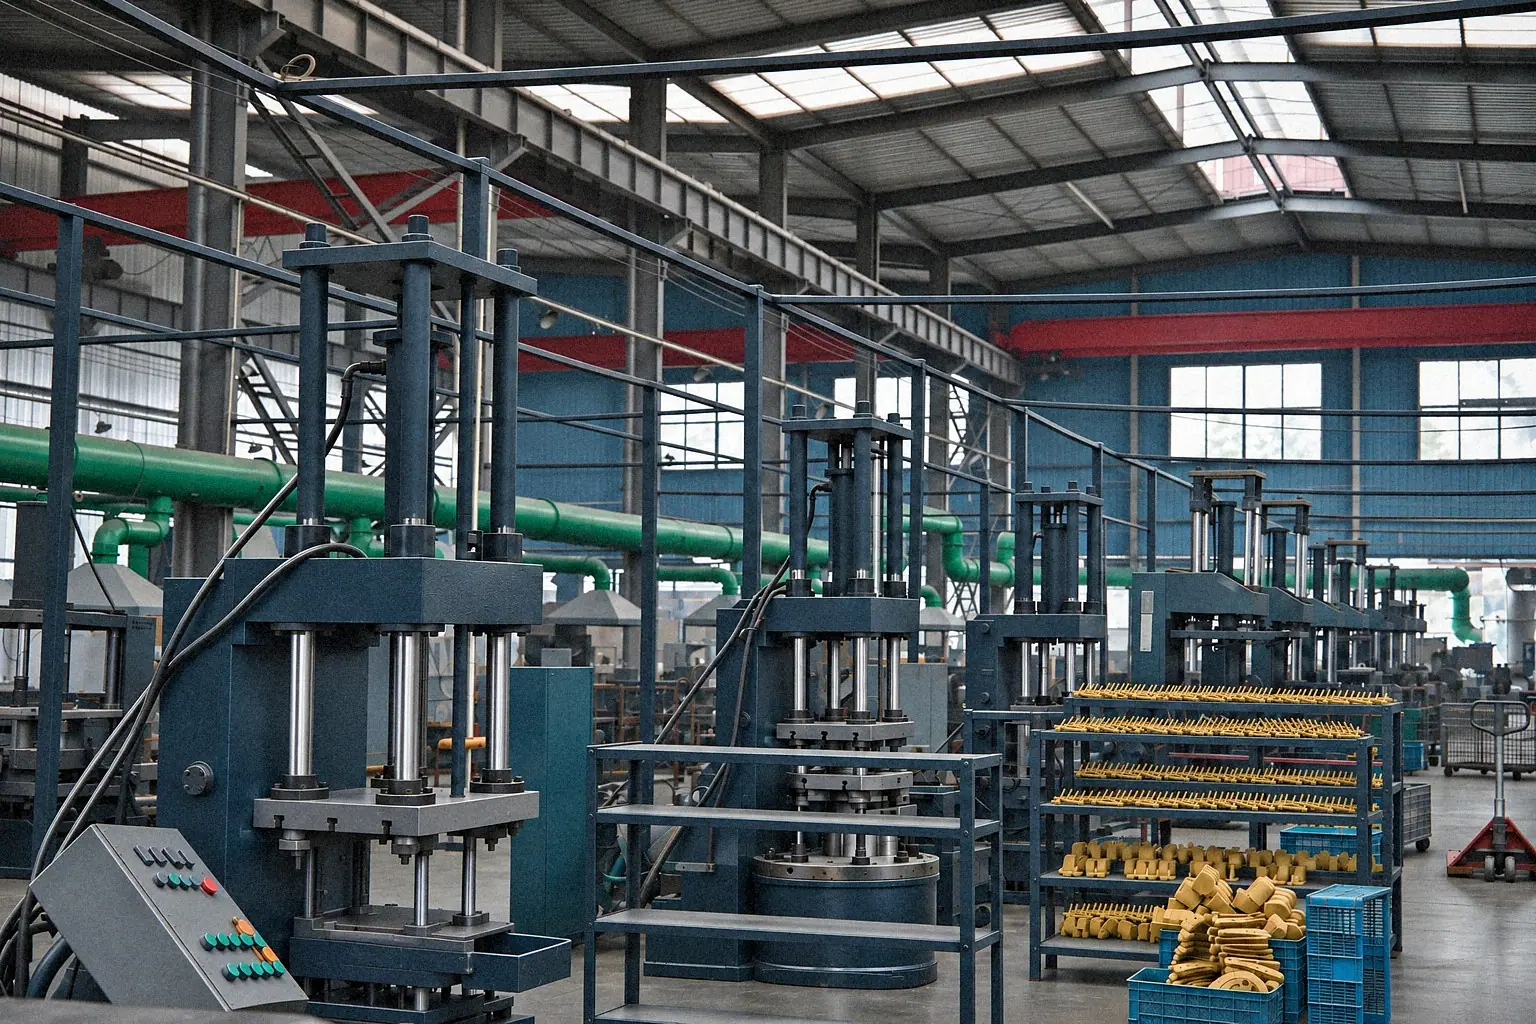
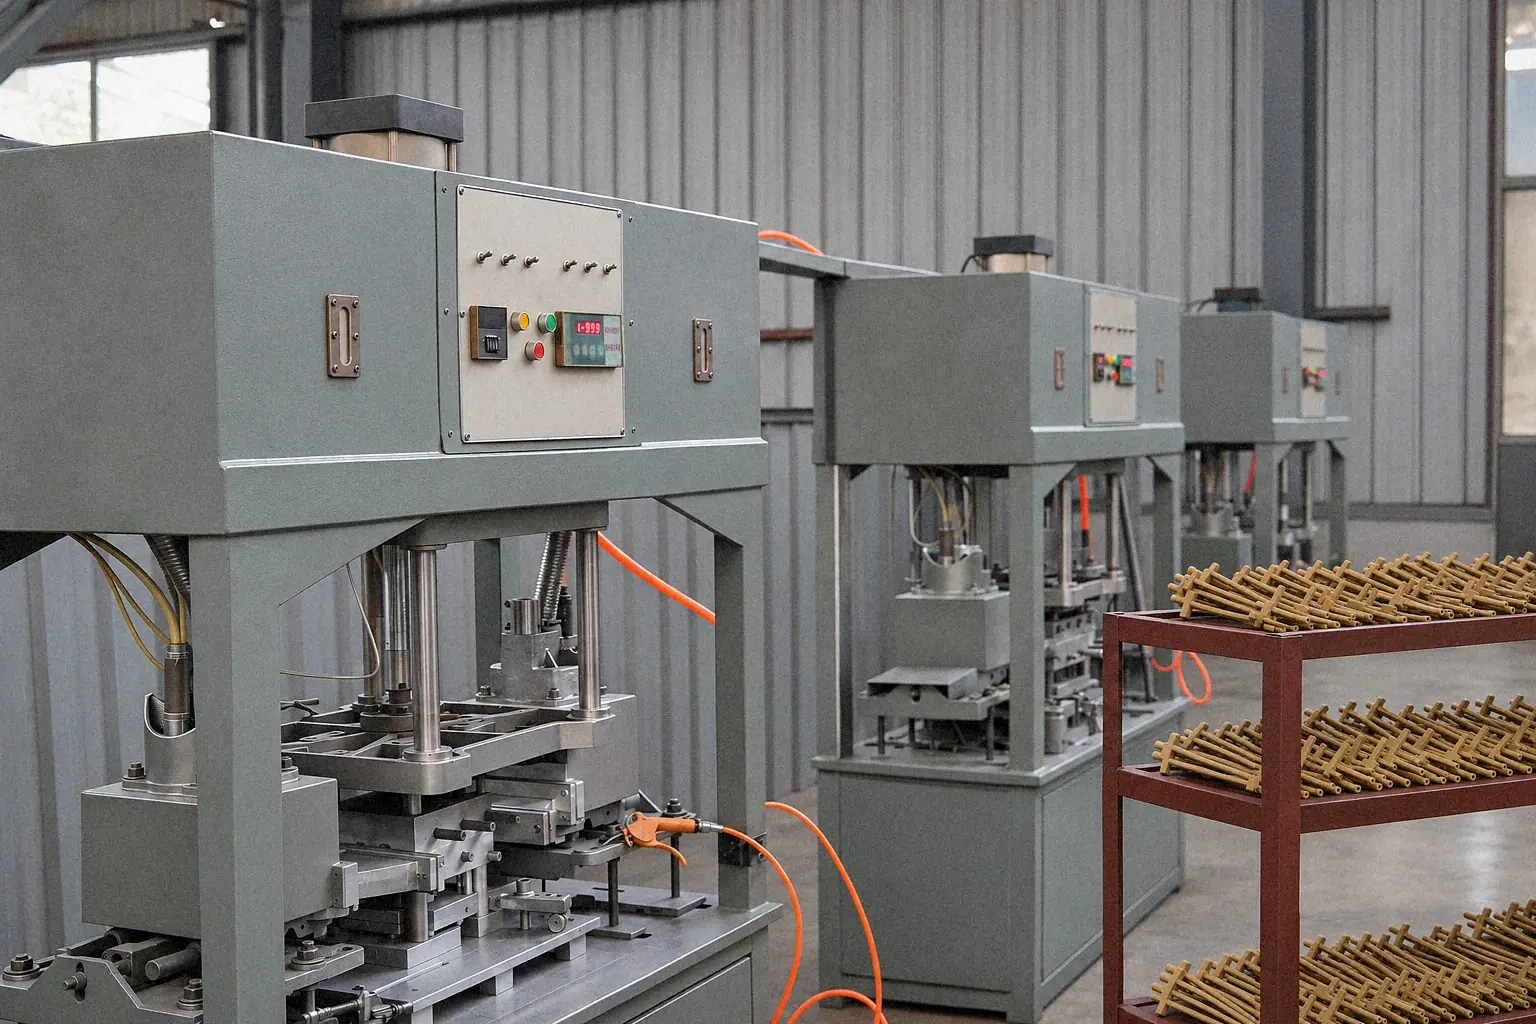
Gravity casting fills a reusable mold under gravity. Check how the proposed tooling will release the part, form internal passages and feed thick sections. Send your geometry, soundness requirements and acceptance criteria along with the A356 or T6 callout so we can review them together.
The permanent mold casting guide explains the definition and design boundaries. The gravity casting process guide covers the production sequence and control points.
Casting scope and finished dimensions
At Bohua, the published size and weight figures below apply to tilt-pour castings. For vertical gravity casting, send the part dimensions so we can review the size requirements separately.
| Feature | Published dimension (mm) | Published weight (kg) | Scope |
|---|---|---|---|
| Casting weight | Not applicable | From <0.2 to >30 | Range extends below 0.2 kg and above 30 kg. |
| Largest casting, longest dimension | >600 | Not applicable | A lower bound for the largest parts, not a maximum size. |
| Minimum wall thickness | About 3 mm typical; 2.5 mm over small areas near the gate | Not applicable | Evaluate against geometry and filling requirements. |
At Bohua
As-cast tolerances are CT8. Key machined features can reach ±0.02 mm where the drawing, feature and datum scheme allow. Identify cast surfaces and machined interfaces separately.
A356 and ZL114 are used for gravity and tilt-pour casting. T5/T6 heat treatment is performed in-house.
Specify the alloy and heat-treatment condition in the drawing. Use the A356 material page and ZL114 material page for material planning.
In-house tooling and machining
Bohua designs and makes its molds in-house, with a tooling workshop containing 17 machines.
At Bohua
Most molds use GB 45 carbon steel, with H13 for higher requirements. An A356 permanent mold typically lasts about 20,000–50,000 shots. That range applies to GB 45 carbon-steel molds; H13 molds last about 100,000 shots with regular maintenance. First article takes 5–6 weeks from drawing confirmation.
The machining workshop has 16 vertical machining centers, 2 CNC engraving and milling machines, 22 CNC lathes and 2 large lathes.
Mark machining stock, datums, sealing faces and bearing bores before defining the delivery scope. State whether the requirement is for a rough casting or a finished machined part. See casting and CNC machining capabilities and the T6 heat-treatment guide for these downstream requirements.
Evidence to define before supplier approval
Match each acceptance requirement to a specified record before approving the project.
At Bohua
Bohua holds IATF 16949:2016 certification issued by NQA, valid through November 20, 2027. PPAP support is available up to Level 5. Inspection equipment includes an optical emission spectrometer, a vacuum hydrogen analyzer, X-ray systems and coordinate measuring machines.
Air-under-water immersion testing is available at 3 bar or more within the equipment range. The pressure, duration and acceptance criteria depend on the project. Impregnation requires customer approval and is performed by a qualified subcontractor.
| Requirement | Record to request | What the buyer should specify |
|---|---|---|
| Alloy and mechanical properties | Material certificate and mechanical test report | Controlling specification and edition, test method, sample source and batch linkage |
| Heat treatment | Heat-treatment record | Required condition, batch identification and property acceptance criteria |
| Finished dimensions | First-article or CMM report | Drawing revision, datums and critical feature list |
| Internal soundness or pressure tightness | Required X-ray or immersion-test evidence | Inspection areas, sampling, test pressure, duration and acceptance criteria |
| Program approval | Specified PPAP package | Submission level and required records |
Use this checklist to specify the evidence you need, then review your part’s test results against the agreed acceptance criteria. Review quality control and inspection capabilities for the available equipment.
Send the inputs for a gravity casting review
Send the current drawing together with the manufacturing and acceptance requirements.
- Dimensioned drawing, revision, CAD model and controlling specifications with editions.
- Alloy, heat-treatment condition, overall dimensions and estimated casting weight.
- Annual demand, order quantities and requested delivery schedule.
- Internal passages, core access, critical walls, machining stock and datum scheme.
- Required finishing, test methods, inspection areas, acceptance limits and records.
- Existing tooling ownership, condition and modification limits, if applicable.
- Packaging and labeling requirements for the delivered part.
For application-specific inputs, use the coolant water outlet casting requirements or automotive suspension bracket RFQ. Use these inputs to describe your proposed component and the requirements you want us to review.
At Bohua, quantities are quoted by annual volume; small batches are negotiable. Use the casting quotation request to start the review.
Send your drawing for a gravity casting review
Include alloy, annual volume, machining scope and acceptance requirements. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →