Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Overview
Aluminum Casting Applications
Choose the application closest to your drawing to identify the manufacturing and inspection inputs for an RFQ. Bohua has operated in casting since 1994. Our factory combines gravity and tilt-pour casting with core making, tooling, heat treatment, CNC machining and inspection at one site in Ningbo.
Choose the component to review
Start with the part's function and critical interfaces. Each page below identifies drawing inputs and manufacturing questions for that component.
Choose a component page, then send your drawing, required alloy and performance rating. We will review the manufacturing route against your production specification.
Other part families: what to send with the drawing
Parts without their own page are reviewed from the drawing, not from the part name. Send the inputs below with the annual volume.
At Bohua
Two die casting machines are available, at 280 t and 450 t. A356 and ZL114 are the confirmed alloys for gravity and tilt-pour casting. PPAP documentation can be provided up to Level 5 when the project requires it.
Compressor housings, covers, brackets, and valve plates
Appliance and HVAC compressor housings, covers, brackets, and valve plates need wall thickness, sealing faces, mounting datums, coating zones, and any vibration or noise requirement defined before quotation. State whether the quote covers the housing, a cover, a bracket, or a valve plate, and list tooling, machining, coating, inspection, and packaging separately from the casting. Choose between die casting, gravity casting and low-pressure casting from the drawing and the annual volume.
Impellers
For a pump, blower, or fan impeller, define the vane geometry, the hub bore and mounting features, and the machining allowance on the balance reference surfaces. Bore size and the agreed runout checks belong in the inspection plan. Balance acceptance and hydraulic or airflow performance stay with the buyer. When the impeller is quoted with a pump housing, use the pump housing page for the pressure boundary and keep the vane and balance inputs in the same request.
Home-appliance castings
For a gas-burner body, define the gas-channel geometry and who owns the project pressure test versus appliance approval. For a motor or compressor bracket, define the mounting datums. Confirm the alloy and temper from the drawing rather than from the appliance name.
Cylinder heads
An aluminum cylinder-head RFQ should define the coolant and oil passages, the combustion-face and valve-seat machining stock, the heat-treatment target, and the project pressure-test plan. Review gravity casting, sand casting or low-pressure casting against the passage geometry and the annual volume; all three are done in-house. Set the PPAP level from the buyer requirement, use the pressure-tight casting page for the leak-test method, and keep engine or vehicle approval with the buyer. See certification and PPAP scope for what the quality-system certificate covers.
Fire-apparatus water-pipe joints
For a fire-apparatus water-pipe joint, define the delivered state, the controlled connection drawing or standard edition, and the sealing faces. State who owns the component test and who owns complete-apparatus approval. A356 with T6 can be reviewed when the drawing specifies that alloy and temper. A catalog example does not approve a hose, a pump module, or a vehicle.
Factory capabilities behind the application review
Bohua brings casting and the supporting manufacturing operations together at one site.
At Bohua
We have worked in casting since 1994. Our site of about 16,300 m² in Ningbo includes casting, core making, tooling, T5/T6 heat treatment, CNC machining and inspection.
- Tilt-pour machines
- 32 machines
- Vertical gravity casting machines
- 10 machines
- Hot-box core shooting machines
- 10 machines
- Vertical machining centers
- 16 machines
Gravity casting and tilt-pour casting are our primary processes. Low-pressure casting has been in-house since 2014. Sand casting is also done in-house.
Use the casting process directory for process capabilities. Select the route against geometry, wall sections, material requirements, annual demand and inspection scope.
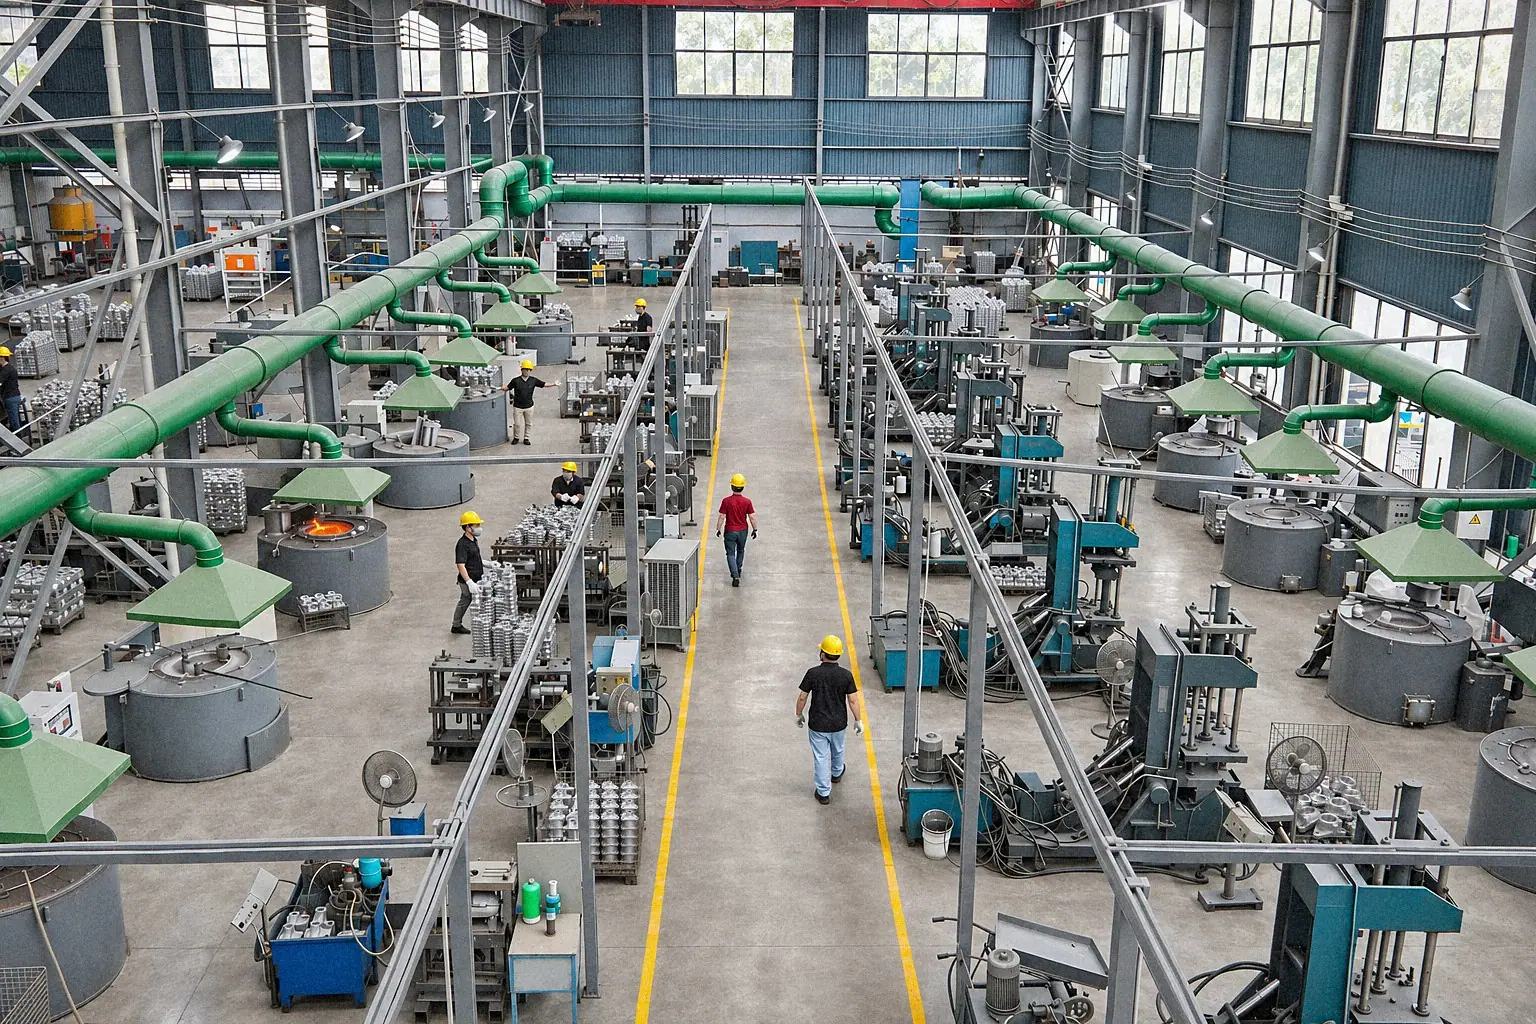
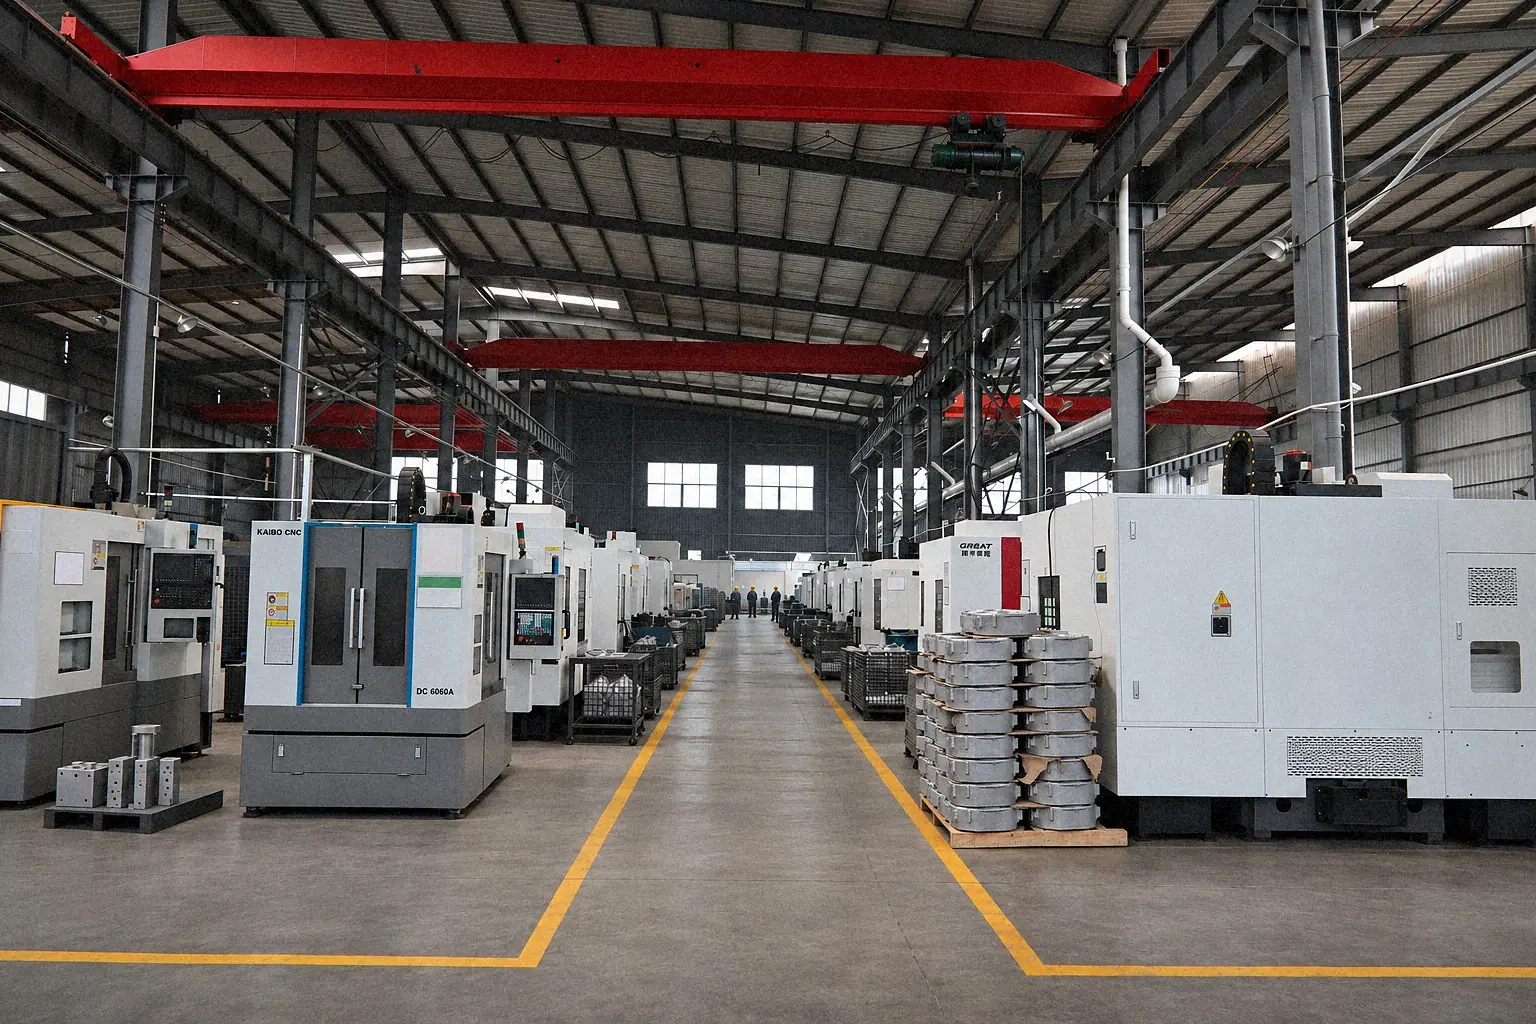
Examples of parts made at Bohua
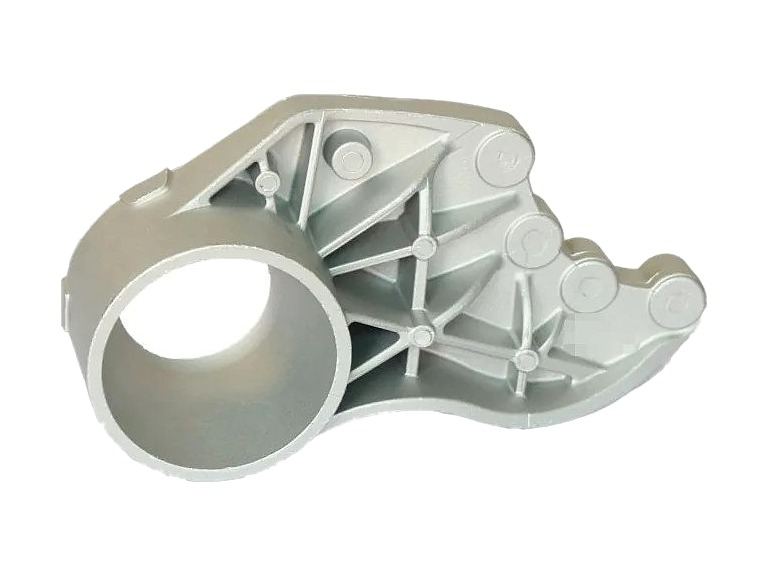
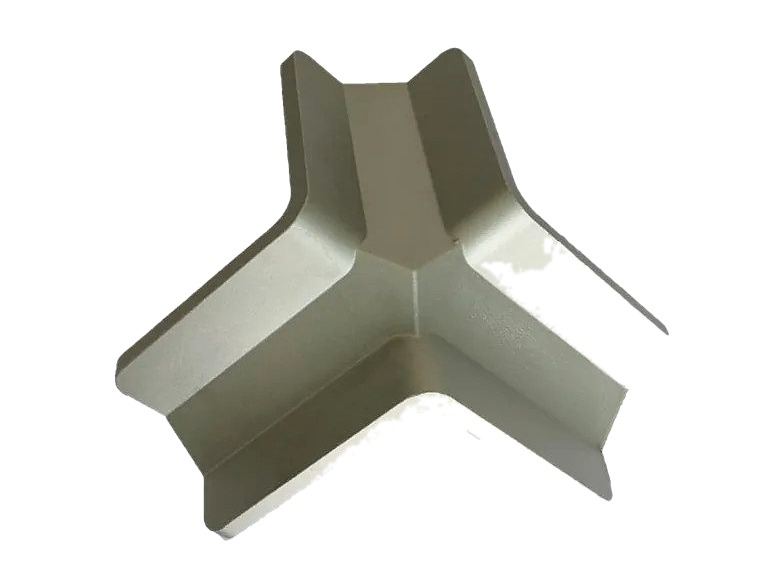
These aluminum castings show examples of geometry made at Bohua. Customer logos and part numbers are masked. Use these photographs to discuss geometry; use your controlled drawing to specify the new part.
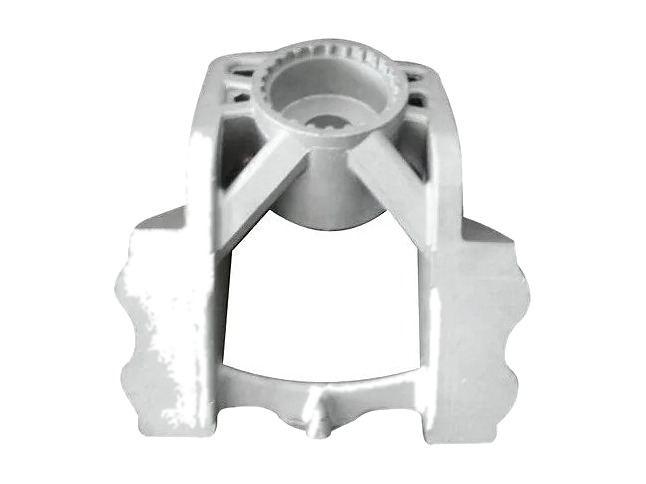
Have a similar part? Send your drawing
Browse the cast-part photo gallery for more examples.
Send the function as well as the drawing
A useful application review connects the component's job to its critical features and required evidence.
| Requirement | Include in the RFQ |
|---|---|
| Fluid or pressure boundary | Medium, service conditions, sealing interfaces and test acceptance requirements |
| Rotating or mating assembly | Bore relationships, mounting datums, clearances and finished measurement condition |
| Structural loading | Load direction, mounting constraints, critical sections and validation requirements |
| Complete delivery scope | Alloy and temper, machining, inspection records, quantity, tooling status and packaging |
For sector requirements, see automotive casting requirements or energy-sector casting requirements. Include your component requirements in the RFQ so we can review the part alongside the requirements for your industry.
If your component is not in the list above, use the aluminum casting RFQ checklist to organize its drawing and requirements, then send them through the casting RFQ form.
Send the drawing for your application
Include the component function, material, annual demand, machining scope and acceptance requirements. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →