Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Aluminum Casting Surface Finish: Specify the Requirement
Surface finish can refer to as-cast texture, a machined surface or an applied finish. These are different purchasing requirements. A useful casting RFQ identifies which surface is being controlled, the delivered state and the evidence needed to accept it. Specify the parameter, units, measurement conditions and final part state.
On this page
Separate the Three Requirements
| Requirement | What to specify | Common quotation gap |
|---|---|---|
| As-cast surface | Areas, allowed surface conditions, applicable visual or texture criteria | A generic process range used as a part guarantee |
| Machined texture | Parameter, units, measurement direction/method and surface boundaries | A bare number without Ra/Rq or a controlled method |
| Coating or conversion finish | Approved system, preparation, thickness where required, masking and final acceptance | Coating name alone, with no interface or inspection definition |
A surface that looks smooth may still fail a dimensional, sealing or coating requirement. Conversely, a functional surface need not receive a cosmetic treatment unless the design or purchase specification requires it.
Write Roughness Requirements Unambiguously
State the parameter and unit together. Ra and root-mean-square roughness, commonly designated Rq, are different parameters; do not treat an RMS value as an Ra value without an approved basis. When reviewing older data, verify whether the unit is micrometers, microinches or another explicitly specified unit.
Record the applicable drawing convention and measurement method, including direction and filtering/evaluation conditions where required. If a source shows a descending range or an unclear comparison symbol, check the original controlled information before editing it. Do not guess a missing digit or silently reverse a range.
This guide does not publish a universal roughness range for resin-sand, gravity or die-cast surfaces. Ask for evidence on a comparable feature and distinguish a typical process observation from a contractual limit.
Ra describes an average profile-height measure. Rz describes a peak-to-valley height measure under the specified convention. Rz is not interchangeable with Ra. Record the governing standard and edition before comparing results, especially on older drawings.
| Record field | Required definition or evidence |
|---|---|
| Surface and state | Drawing feature, measurement location, as-cast or machined state, and any polishing or coating |
| Parameter and unit | Ra, Rq or Rz as specified; micrometers or the explicitly stated drawing unit |
| Trace direction | Direction relative to surface lay and accessible trace locations |
| Evaluation conditions | Applicable standard and edition, filters, evaluation length and stylus conditions |
| Instrument | Instrument identification and calibration or verification record |
| Acceptance basis | Drawing limit, sampling rule, actual measured results and disposition |
At Bohua
Bohua has a Mitutoyo SJ-410 surface roughness tester. Mirror polishing is available. For a polished surface, specify the Ra requirement, measurement location and agreed conditions so you can assess acceptance from the measured result.
Plan Machining Around Functional Surfaces
For sealing faces, bearing seats, datum pads and mating interfaces, define the final geometry and surface requirement together. Review stock, access, fixturing, tool marks, edge condition and the stage at which acceptance will be checked.
A roughness value alone cannot replace flatness, waviness, defect or leak-test requirements when those are needed by the design. See the CNC machining capability page and the casting tolerance guide when preparing the drawing package. The supplier should identify assumptions that prevent a firm quotation rather than substitute a generic surface range.
At Bohua
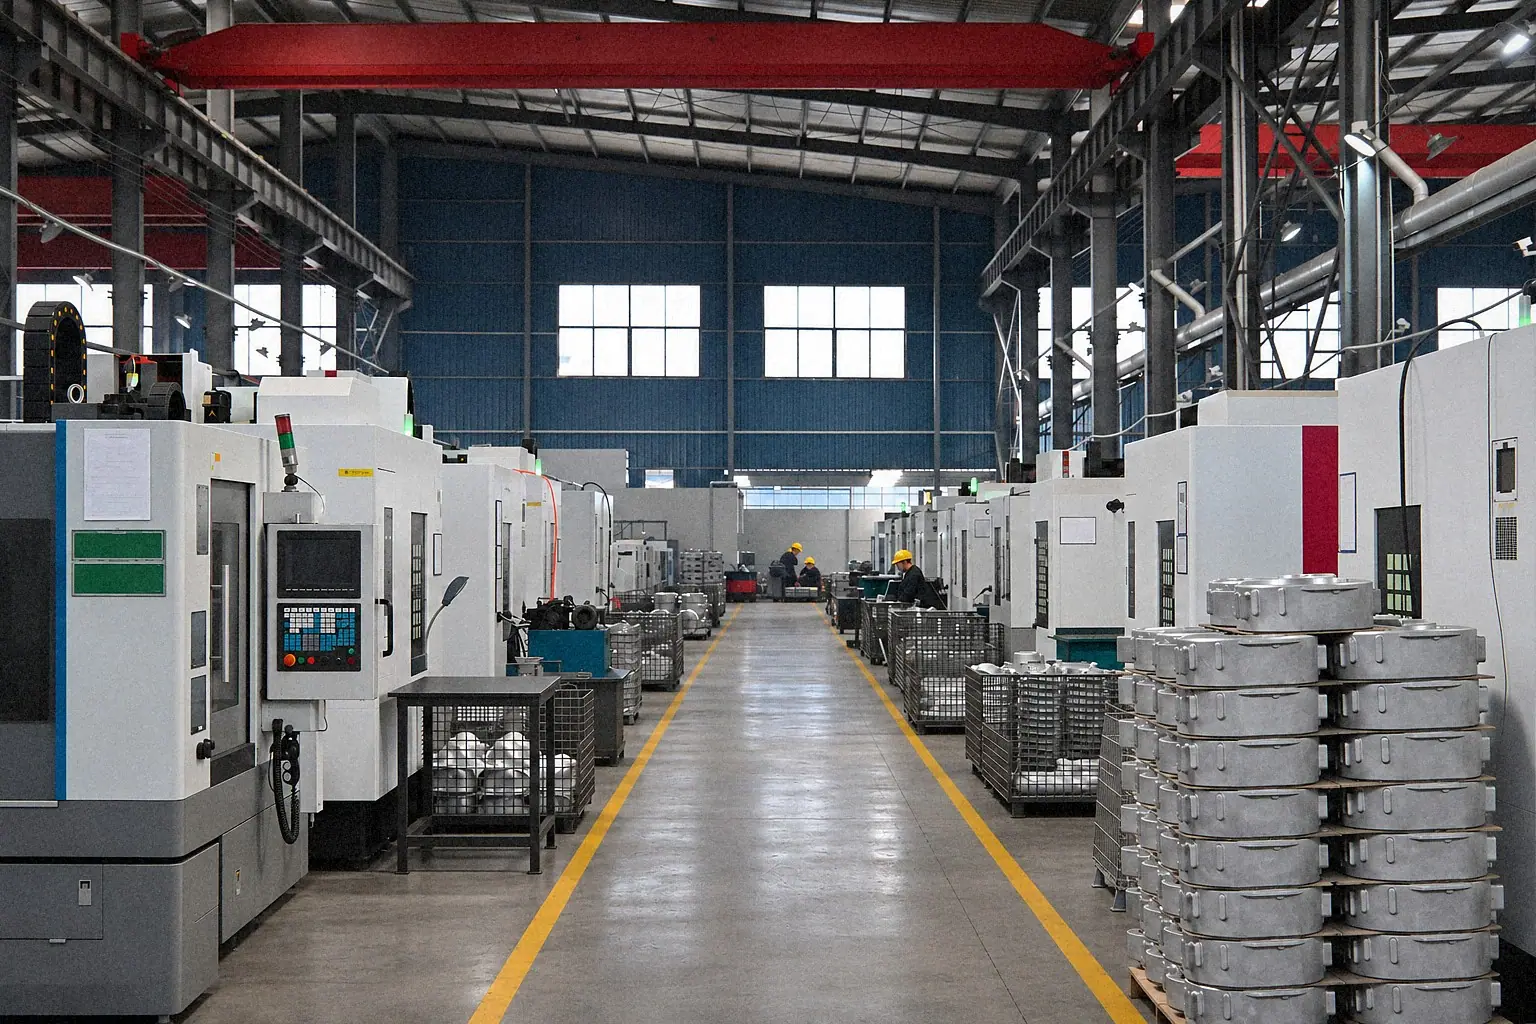
Bohua’s machining equipment includes 16 vertical machining centers, 2 CNC engraving and milling machines, 22 CNC lathes and 2 large lathes. Identify the faces that remain as-cast and those that require machining. State the surface parameter, units, measurement direction and final delivery condition on the drawing. Use a photograph to mark the surface location and appearance, then state how you want the specified requirement inspected.
Bohua quotes CT8 as-cast tolerances and key machined features to ±0.02 mm where the drawing, feature and datum scheme allow. Specify the surface roughness value separately from these dimensional limits. Bohua also completes T5 and T6 heat treatment in-house. Identify the finished state for the surface requirement, including any heat treatment and machining, so the inspection requirement refers to the delivered component.

For a coolant connection, identify the sealing face and its final state in the coolant water outlet casting requirements.
Scope Coating, Masking and Dimensional Effects
For anodizing, powder coating, painting or another specified finish, provide the approved finish specification and edition or a buyer-controlled requirement. Agree the substrate condition, preparation, required thickness and measurement method, color or appearance where relevant, and acceptance evidence. Mark masked bores, threads, seals, datum faces and electrical-contact areas. Identify whether dimensions apply before or after the finish and who accounts for its effect on fits.
Specify how handling and packaging protect the accepted surfaces. Do not place a single unverified coating-thickness range on every casting family. Hardness requirements also need a defined material, location, test method and scale. Do not convert a coating-hardness statement into an HRC value without an applicable, approved basis.
Use the anodizing, powder coating and masking guide to define the treatment route and coating acceptance.
RFQ Surface Schedule
For each controlled area, include:
- Feature ID and drawing/model reference.
- As-cast, machined, coated or masked final state.
- Geometry and texture requirements with parameters and units.
- Finish system and thickness/appearance criteria where applicable.
- Inspection method, sampling and record requirements.
- Repair, touch-up and deviation approval rules.
- Cleaning, corrosion protection and packaging requirements.
FAQ
Does a coating remove the need for machining?
Not automatically. Required geometry, fits and functional surfaces still need a defined manufacturing and acceptance plan.
Can a supplier choose the roughness unit from context?
It should not. Resolve the drawing or specification ambiguity before quotation and inspection planning.
What is the most useful first step?
Send a marked surface schedule with the drawing through the surface-finish RFQ route. Ask the supplier to return proposed operations, exclusions and any missing acceptance details.
Send your drawing and surface schedule
Submit the RFQ details, then email your drawing for a structured quote review. Send the drawing, target alloy, finishing scope, MOQ, and delivery timing. Bohua will review it like a real sourcing project, not a generic contact request. Our engineering team can recommend the right alloy, process, and design optimizations for your specific requirements.
Send your drawing →