Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Aluminum Casting Tolerances: ISO 8062, Die Casting and CNC
An aluminum casting tolerance is the permitted variation for a specified feature at a specified delivery stage. There is no single plus/minus value that applies to every sand, gravity or die casting. Start with the nominal dimension, feature location, mold or core arrangement, and whether acceptance is before or after machining.
On this page
- Separate three requirements before comparing foundries
- Which casting tolerance standard should you use?
- Gravity casting versus die casting: review the actual feature
- A drawing-review worksheet you can use
- What evidence should accompany a tight-tolerance claim?
- Bohua’s Casting and Machining Tolerances
- Inspection Resources for the Datum Scheme
- Common questions
Separate three requirements before comparing foundries
Compare ISO 8062 and die casting standards, machining allowances and inspection inputs. Separate as-cast size, machined size and geometrical relationships in the drawing.
| Requirement | Example feature | What the drawing must clarify |
|---|---|---|
| As-cast size | Housing envelope or unfinished wall | Applicable general tolerance, individually toleranced exceptions and inspection state |
| Machined size | Bearing bore, thread or sealing diameter | Final limits, machining stock, process sequence and inspection method |
| Geometrical relationship | Bore alignment or sealing-face flatness | The applicable geometrical specification and datum references where required |
A bore diameter within its size limits does not, by itself, establish alignment to another bore. Equally, stock left for CNC machining is not the finished-part tolerance. Ask suppliers to distinguish these requirements in the quotation and first-article plan.
For example, a drawing dimension of 100 ±0.5 mm permits 99.5 to 100.5 mm. This is an arithmetic illustration, not a Bohua capability claim or a recommended casting tolerance.
Which casting tolerance standard should you use?
ISO 8062-3:2023 addresses general dimensional and geometrical tolerances and machining allowances for castings with indicated dimensions using plus/minus tolerances. Its published scope excludes 3D CAD models without indicated dimensions and does not cover every type of geometrical control. Use the controlled standard and drawing to select the applicable requirements.
Use the ISO 8062 drawing and tolerance-width guide for grade notation, nominal-size bands and total-width interpretation.
For high-pressure die casting, NADCA's Product Specification Standards include standard and precision tolerances, GD&T and design guidance. Do not transfer a die-casting table to gravity casting without a process-specific review.
ASTM B108/B108M addresses permanent-mold casting material requirements, not a universal dimensional tolerance. The ASTM versus ISO casting standards guide explains how these documents serve different purposes.
Source: ISO 8062-3:2023, public scope.
Source: NADCA 2024 Product Specification Standards for Die Castings, official overview.
Source: ASTM B108/B108M-25, public scope.
Gravity casting versus die casting: review the actual feature
Compare the same feature and delivery state when reviewing gravity casting and high-pressure die casting.
| Feature or condition | Question for gravity permanent mold | Question for high-pressure die casting |
|---|---|---|
| Dimension within one mold section | What variation can the proposed tool and process hold? | Which applicable standard or precision requirement is being quoted? |
| Feature crossing a parting line | How are mold alignment and trimming addressed? | How do parting and moving tool elements affect the feature? |
| Cored passage or internal wall | How is core location checked and minimum wall verified? | How are internal features formed and verified? |
| Final machined interface | Which casting datums and stock support machining? | Which datums, stock and internal-integrity checks support machining? |
| Heat-treated or coated component | At what stage is acceptance inspection performed? | Is the proposed alloy and process compatible with the full finishing route? |
This comparison deliberately avoids claiming one process is always twice as accurate or assigning a guaranteed tolerance from annual volume alone. Ask for evidence from a relevant feature and delivery condition. See the permanent mold process guide for process selection.
A drawing-review worksheet you can use
The following is an illustrative planning template, not a released drawing note or an inspection report. Have the responsible design engineer fill and approve each field.
| Field | Buyer input |
|---|---|
| Part and revision | Part number, controlled drawing revision and model revision |
| Supplied condition | As cast / heat treated / finish machined / coated |
| General requirements | Standard, edition, selected requirements and exceptions |
| Critical feature | Feature ID, nominal size, limits and functional reason |
| Dimension range and units | Nominal dimension and applicable range (mm); specify a different unit explicitly |
| Datum scheme | Identified datum features and inspection setup |
| Machining stock | Surfaces to machine and agreed stock at the relevant stage |
| Verification | Method, reporting format, sampling and approval owner |
For a pump housing, use separate rows for the bearing bore, seal face and their relationship. Attach the seal-chamber-to-bearing-bore CMM checklist when that relationship is the assembly risk. For an internal passage, the core-shift and wall-thickness checklist addresses a different inspection problem. Define the datum setup and measurement method in the CMM inspection requirements for cast aluminum parts.
What evidence should accompany a tight-tolerance claim?
Request a drawing-linked dimensional report that identifies the measurement state, feature IDs, actual results, equipment or method, part or lot identification and inspection date. Where a customer requires capability or measurement-system studies, agree the study design and acceptance criteria separately; a single first-article result is not a production capability study.
Use Bohua's quality-control overview to review the inspection scope. A CMM photograph demonstrates equipment, not proof that a new part meets its drawing. The project-specific report is the evidence to review.
Bohua’s Casting and Machining Tolerances
At Bohua
Bohua’s confirmed as-cast tolerance is CT8. Key machined features can reach ±0.02 mm where the drawing, feature and datum scheme allow. These are two different delivery states.
Mark the casting dimensions separately from the bores, locating faces and sealing interfaces that will be machined. The drawing should show the applicable datums and the condition in which each critical feature will be measured.
| Feature state | Confirmed capability | Conditions to define |
|---|---|---|
| As-cast dimensions | CT8 grade | Standard edition, applicable dimension range, feature, process, datum requirements and inspection state |
| Key machined features | ±0.02 mm | Feature and nominal dimension (mm), permitted limits (mm), datum scheme, final condition and measurement method |
Match each selected feature to the applicable as-cast or machined tolerance. Send us the marked features so we can review which tolerance applies to each one.
At Bohua
Selected critical as-cast dimensions at Bohua can reach approximately DCTG 6; for a nominal dimension of 63–100 mm, DCTG 6 corresponds to a total tolerance of 0.78 mm, or ±0.39 mm if centered on nominal.
Bohua cannot accept machining work that requires ±0.005 mm.
Mark the selected casting dimensions for individual agreement; if ISO 8062-3:2023 governs the drawing, check its applicable size band and grade. The tighter casting grade is not a blanket replacement for routine CT8.
For how to read an ISO 8062-3 casting tolerance chart, see the ISO 8062 tolerance guide.
Inspection Resources for the Datum Scheme
At Bohua
Bohua has 16 vertical machining centers and uses Hexagon Global S and NANO Metrology coordinate measuring machines.
For your machined casting, mark the datum references and required inspection record for each critical dimension.
At Bohua
When T5 or T6 is specified, Bohua completes that heat treatment in-house; identify whether the dimensional requirement applies before or after heat treatment and final machining.

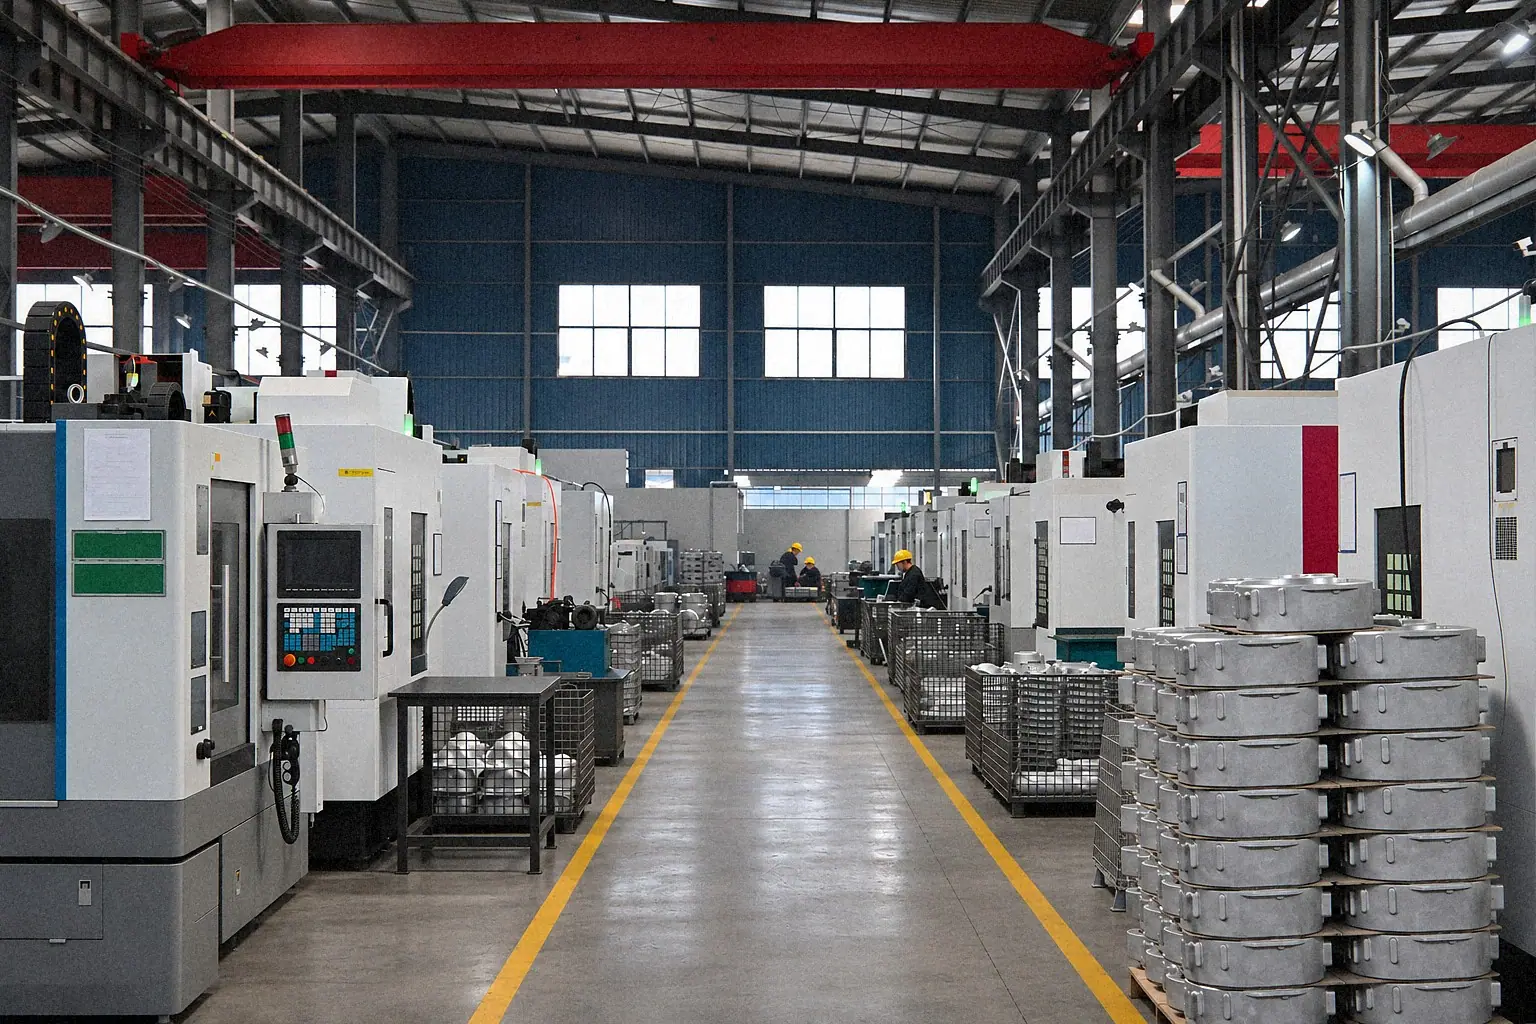
Review casting and CNC machining for the manufacturing scope. For a suspension bracket, carry the feature limits and datum scheme into the suspension bracket quotation scope.
At Bohua
A handheld 3D scanner is also available at Bohua for dimensional review.
Assign each critical feature its agreed measurement method and report requirement using the CMM inspection planning guide.
Common questions
Can a STEP file alone define the required tolerances?
Do not assume an unannotated model specifies the complete acceptance requirement. Supply a controlled drawing or an agreed model-based definition with the required annotations and governing specification. ISO 8062-3's stated scope does not cover CAD models without indicated dimensions.
Does T6 guarantee the final dimensions?
No. Include heat treatment, machining and finishing in the agreed production sequence, and identify the state in which dimensions must pass inspection. See the A356 properties and testing guide.
Should every surface be machined?
Only specify machining where the function, finish or dimensional requirement needs it. Ask the foundry to identify which requirements can be met as cast and which need secondary operations, with assumptions and exceptions stated before tool approval.
Send the drawing for a tolerance and machining review. Include the worksheet above so the response addresses the critical features rather than a generic process tolerance.
No numerical process-capability guarantee or copyrighted tolerance table is reproduced here. The approved drawing, controlled standards and agreed verification plan govern acceptance.
Send the marked casting and machining drawing
Send the controlled drawing, alloy, delivery condition, annual volume and required acceptance records. Submit the RFQ details, then email your drawing for a structured quote review. Send the drawing, target alloy, finishing scope, MOQ, and delivery timing. Bohua will review it like a real sourcing project, not a generic contact request. Our engineering team can recommend the right alloy, process, and design optimizations for your specific requirements.
Send your drawing →