Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Permanent Mold Aluminum Casting: Process, Uses and Limits
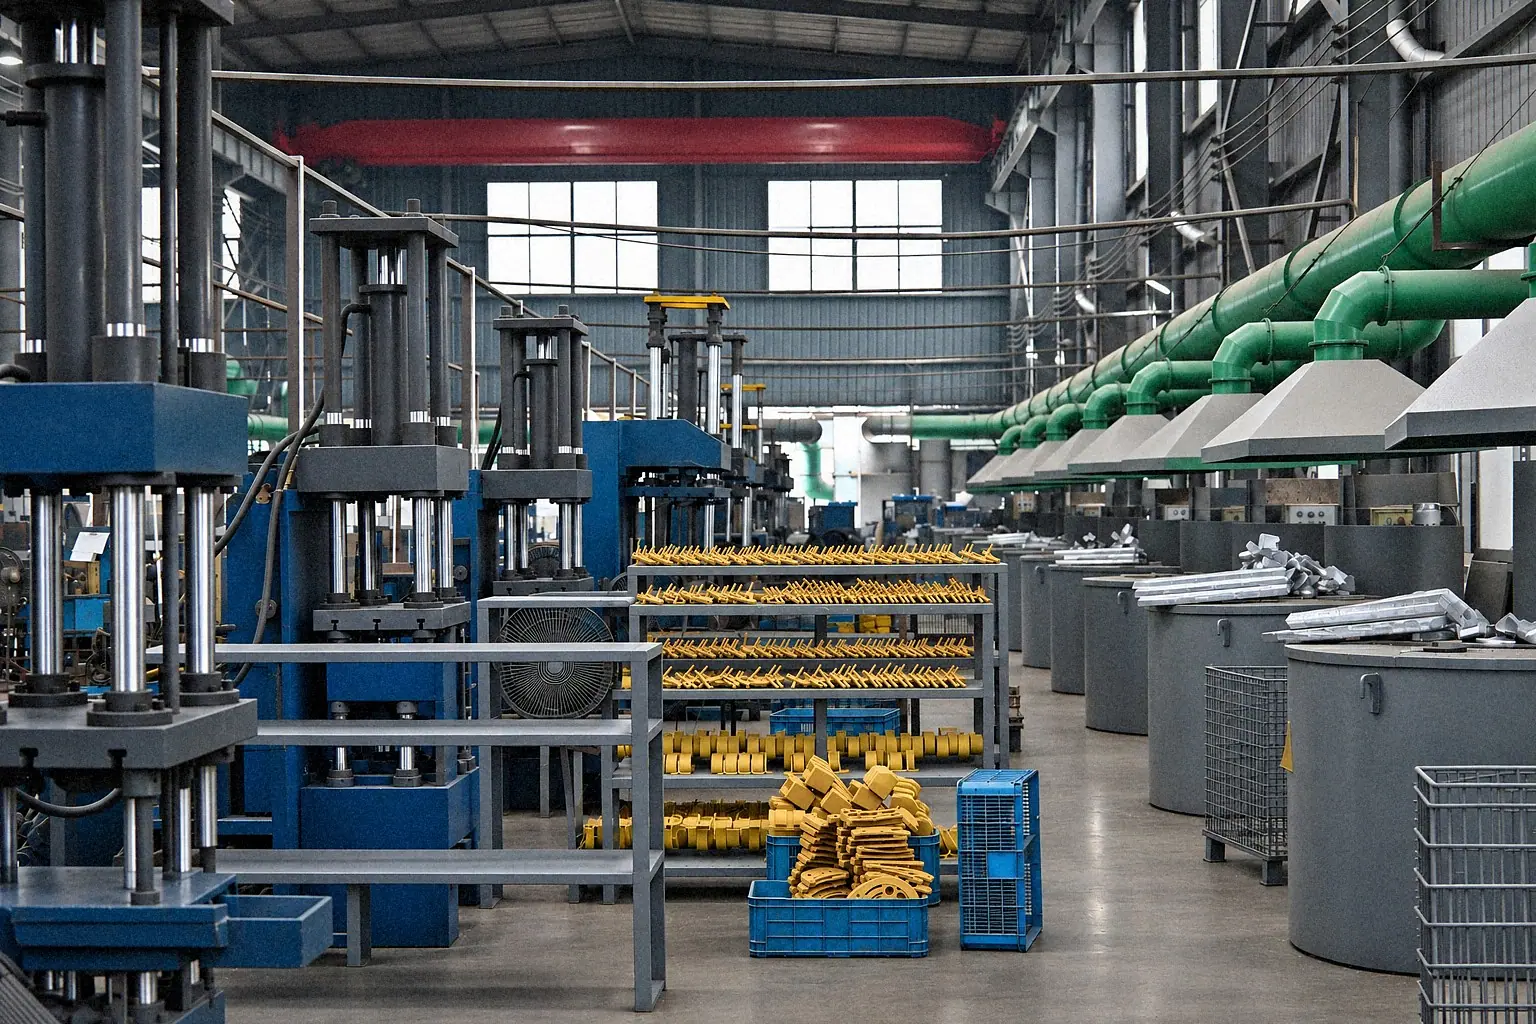
Permanent mold aluminum casting uses a reusable metal mold. This guide focuses on the gravity-filled route, including designs that need sand cores. Suitability depends on mold release, feeding, internal passages and the finished-part requirements. Bohua makes molds in-house, operates 10 hot-box core shooting machines and performs T5/T6 heat treatment in-house.
On this page
What permanent mold means
Permanent mold describes reusable metal tooling; gravity describes how metal fills it. Gravity permanent mold casting combines the two. Low-pressure casting also uses reusable metal tooling, so a purchase specification should identify the filling route instead of relying on the mold name alone.
Sand cores can form internal passages inside a reusable metal mold. This is often called semi-permanent mold casting. The core is expendable even though the outer mold is reused.
For the production sequence and inspection controls, use the aluminum gravity casting process guide.
Check the design boundaries
Reusable tooling is useful when the geometry can be released from the mold and repeat demand supports the tooling scope. Send your strength, pressure-tightness, surface-finish and dimensional requirements so we can review the route against the finished part.
| Design question | Input to mark on the drawing | Boundary to resolve |
|---|---|---|
| Can the part release? | Parting line, draft directions and undercuts | Confirm metal core withdrawal or a removable sand-core arrangement. |
| Can internal passages be formed? | Passage sections, core location and cleaning access | Define core support, removal and inspection access. |
| Can heavy sections be fed? | Wall transitions, bosses and critical pressure boundaries | Review feed paths and local cooling rather than assuming uniform soundness. |
| What is machined? | Datums, bores, threads, sealing faces and machining stock | Show finished features separately from as-cast dimensions. |
| What must survive heat treatment? | Required temper and distortion-sensitive interfaces | Agree the sequence, machining allowance and any permitted straightening. |
Use the gravity casting design guide for detailed drawing preparation. For a cast intake manifold, identify internal passages and sealing interfaces before evaluating tooling.
At Bohua
Within Bohua's tilt-pour permanent-mold scope, walls are normally about 3 mm thick. A 2.5 mm wall is possible over small areas near the gate, subject to the mold and gating design. The tilt-pour casting range includes weights below 0.2 kg and above 30 kg, and the largest parts have a longest side above 600 mm. These statements describe tilt-pour scope; they do not set limits for every permanent-mold process.
When another route needs review
Compare another route when mold release, passage geometry or required features conflict with the proposed permanent mold design. Do not select a process from an annual-volume threshold alone.
| Route | Reason to compare | Further reading |
|---|---|---|
| Sand casting | Expendable tooling or a different core arrangement may suit the geometry or design changes. | Sand casting vs gravity casting |
| Low-pressure casting | Bottom filling and pressure-assisted feeding may suit the cavity and feed path. | Low-pressure vs gravity casting |
| High-pressure die casting | Fine detail and thin sections may favor injection into the die, subject to material and acceptance requirements. | Gravity casting vs die casting |
Define the design and acceptance inputs
A useful design package makes the tooling, material condition and finished surfaces explicit. These inputs prevent two quotations from describing different parts.
- Identify the required gravity permanent mold route and whether tilt-pour is acceptable. If the route is open, request a proposed route with its assumptions.
- Send revision-controlled 2D drawings and a 3D model. Specify the alloy, temper and controlling material specification with its edition.
- Show core quantity and type, inserts or chills, parting-line restrictions and draft assumptions. Request disclosure of any moving tool elements.
- State whether the first-article tool must match production tooling. Define tool ownership, maintenance responsibility and expected life as contractual assumptions.
- Identify the machining sequence relative to heat treatment. Mark bearing seats, seal bores and gasket faces that are sensitive to distortion. State whether straightening is permitted.
- Separate fully machined, cleaned-up and as-cast surfaces. Give surface texture requirements for each functional face.
- Mark the pressure boundary and every surface opened by machining. Define test medium, pressure, hold time, test stage, sampling and acceptance criteria.
- Specify the required material record, heat-treatment record, datum-based dimensional report and any internal inspection evidence. Identify approval and traceability requirements.
- Provide sample quantities, annual demand, delivery batches, destination, Incoterm and target first-article timing.
For a pressure-containing part, agree any impregnation or weld-repair permission explicitly. Inspection references must identify their editions, relevant thickness ranges and acceptance criteria. Agree the part-acceptance evidence alongside the quality-system certificate review.
For the detailed pressure-test inputs, see the casting leak-test specification guide.
What Are the Tolerances for Permanent Mold Casting?
At Bohua
For Bohua permanent-mold drawing review, routine as-cast tolerance is CT8. Selected demanding as-cast dimensions can reach about DCTG 6, while the critical machined-dimension capability is ±0.02 mm. Specify each feature and its inspection condition; the selected as-cast grade is not a blanket tolerance for the entire part.
For an 80 mm as-cast feature, DCTG 6 in ISO 8062-3 corresponds to a total tolerance of 0.78 mm, or ±0.39 mm if the tolerance is centered on nominal. Bohua can reach about DCTG 6 on selected features of this kind.
Bohua tooling and core resources
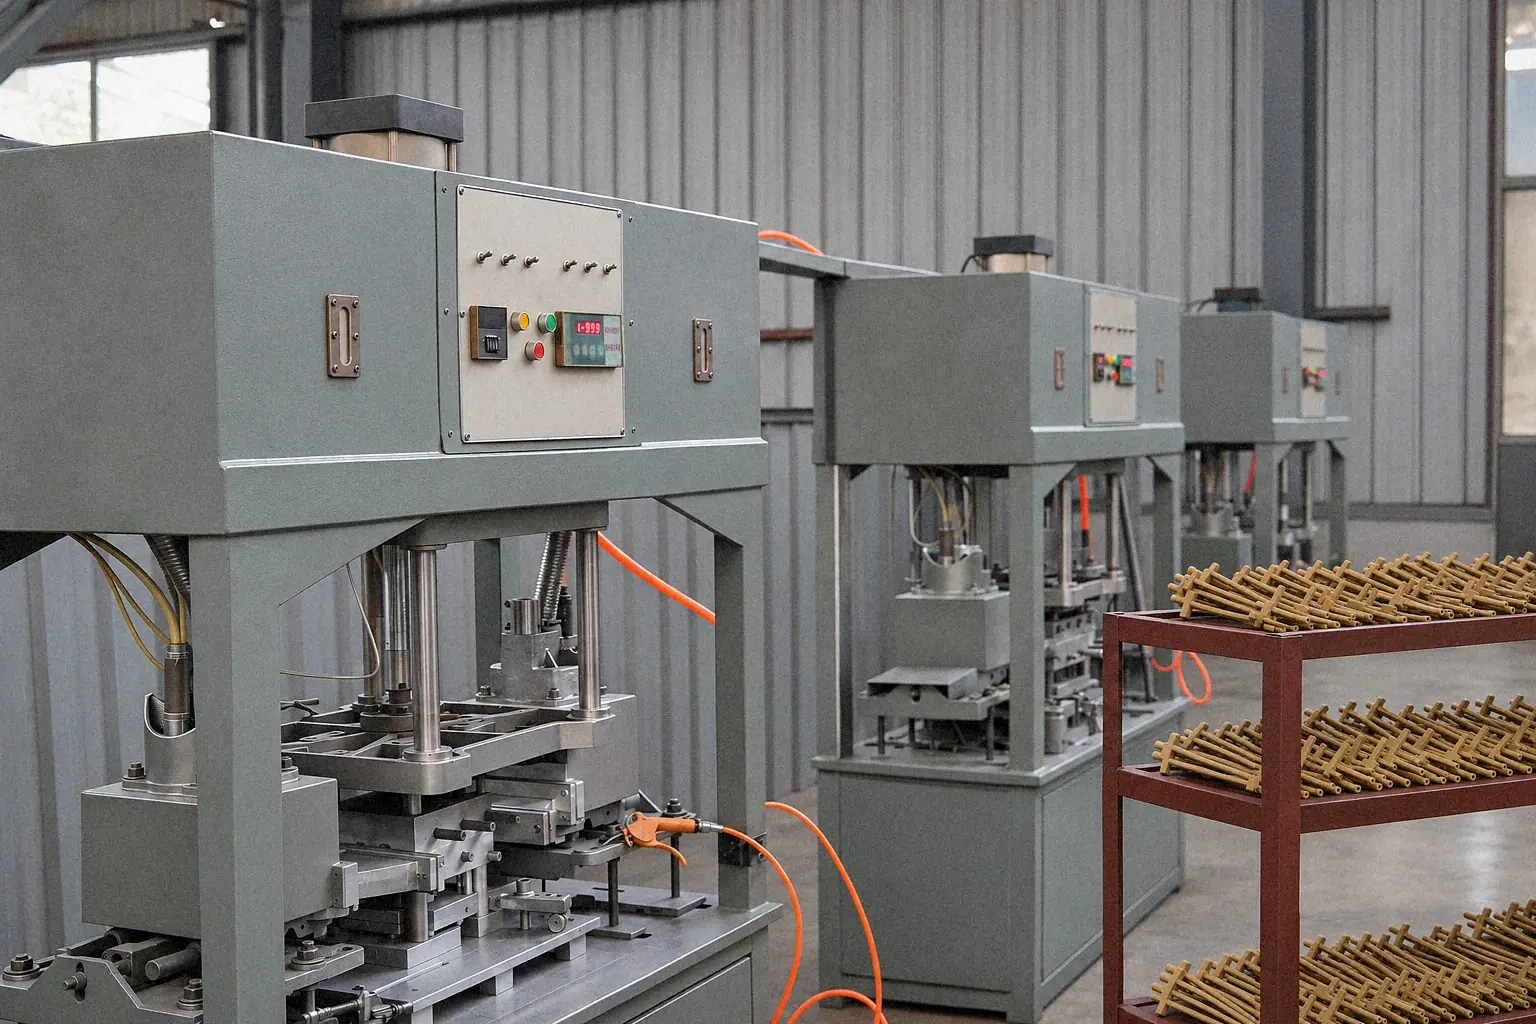
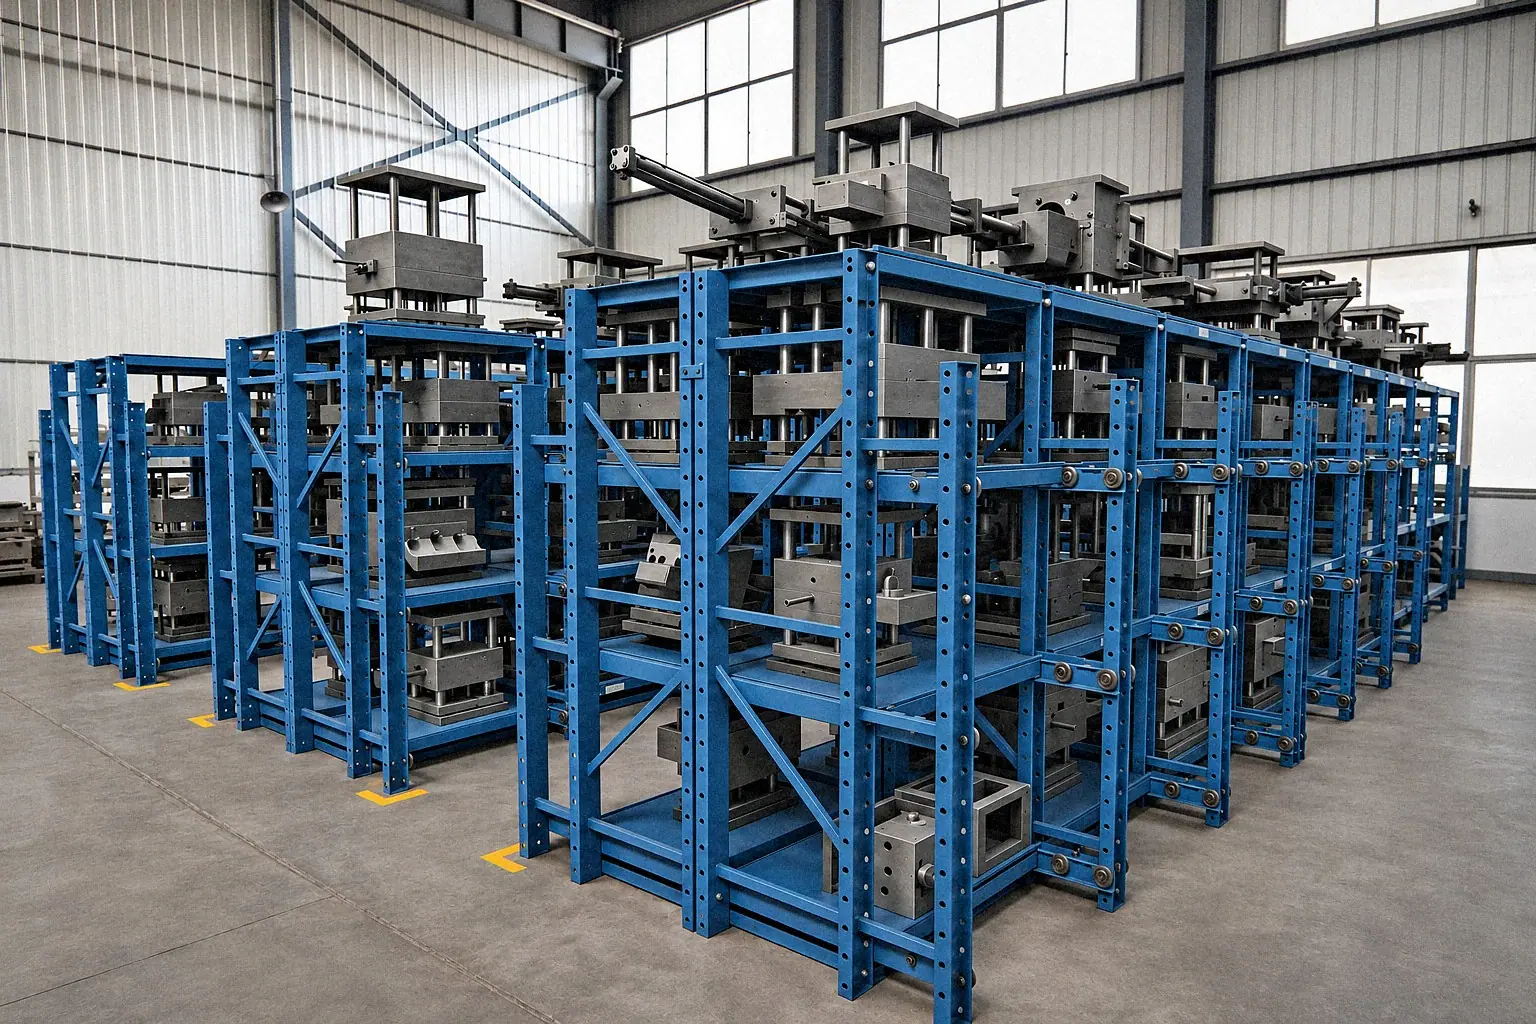
Bohua makes its molds in-house and has core-making and heat-treatment resources relevant to permanent mold designs. Send the drawing so we can review mold release, core access and the required heat-treatment condition for your part.
At Bohua
- Bohua designs and makes molds in-house, using UG and SolidWorks for mold design and AnyCasting for casting simulation.
- Bohua has 10 hot-box core shooting machines. Some tilt-pour castings use sand cores.
- Bohua uses A356 and ZL114 for gravity and tilt-pour casting. T5/T6 heat treatment is carried out in-house.
For equipment counts and casting scope, see Bohua gravity casting capability. Submit the design package through the permanent mold drawing review request.
At Bohua
Bohua normally reaches first article 5–6 weeks after drawing confirmation. Most molds are made from GB 45 carbon steel; H13 is used where the tooling requirements are higher. Keep the first-article milestone separate from customer approval and series-delivery scheduling.
| Input | Confirmed scope | Project decision |
|---|---|---|
| Tilt-pour wall layout | About 3 mm typical; 2.5 mm only in small gate-adjacent areas | Mark the local thin area and feeding path |
| First article | 5–6 weeks from drawing confirmation | Define the first-article deliverable and subsequent approval steps |
| Dimensions | Routine CT8; selected as-cast features about DCTG 6; critical machined features ±0.02 mm | Assign tolerances by feature and manufacturing stage |
| Draft and surface finish | No numerical factory values supplied here | Agree release directions, draft and measured surface requirements |
Permanent Mold Aluminum Tool Life: GB 45 vs H13
At Bohua
Bohua selects GB 45 carbon steel or H13 for permanent-mold tooling according to the product's tool wear and cost-effectiveness.
| Mold steel | Approximate life | Selection condition |
|---|---|---|
| GB 45 carbon steel | GB 45 carbon-steel molds have an approximate life of 20,000–50,000 shots. | Lower initial tooling cost; selected where the product's tool wear and cost-effectiveness support it. |
| H13 | H13 molds have an approximate life of 100,000 shots when maintained as specified. | Used for higher tooling requirements; the stated life depends on the specified maintenance. |
For the finishing sequence, use the T6 treatment and acceptance guide.
Send your drawing for a process review
Include the drawing revision, alloy, annual volume, machining scope and acceptance requirements. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →