Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering resource
Aluminum Gravity Casting Design Guide
Prepare a gravity casting RFQ by connecting geometry, material, machining, and acceptance requirements before tooling.
On this page
Start with the drawing and the required function
Prepare wall sections, core passages, machining datums, and acceptance requirements before releasing a gravity casting tool. Keep required performance separate from an assumed manufacturing route.
A practical buyer's guide for engineers, sourcing teams, and quality managers.
Consider this RFQ failure pattern: The drawing is over-toleranced, the alloy is chosen by habit, and the supplier is judged on piece price instead of process fit.
At Bohua
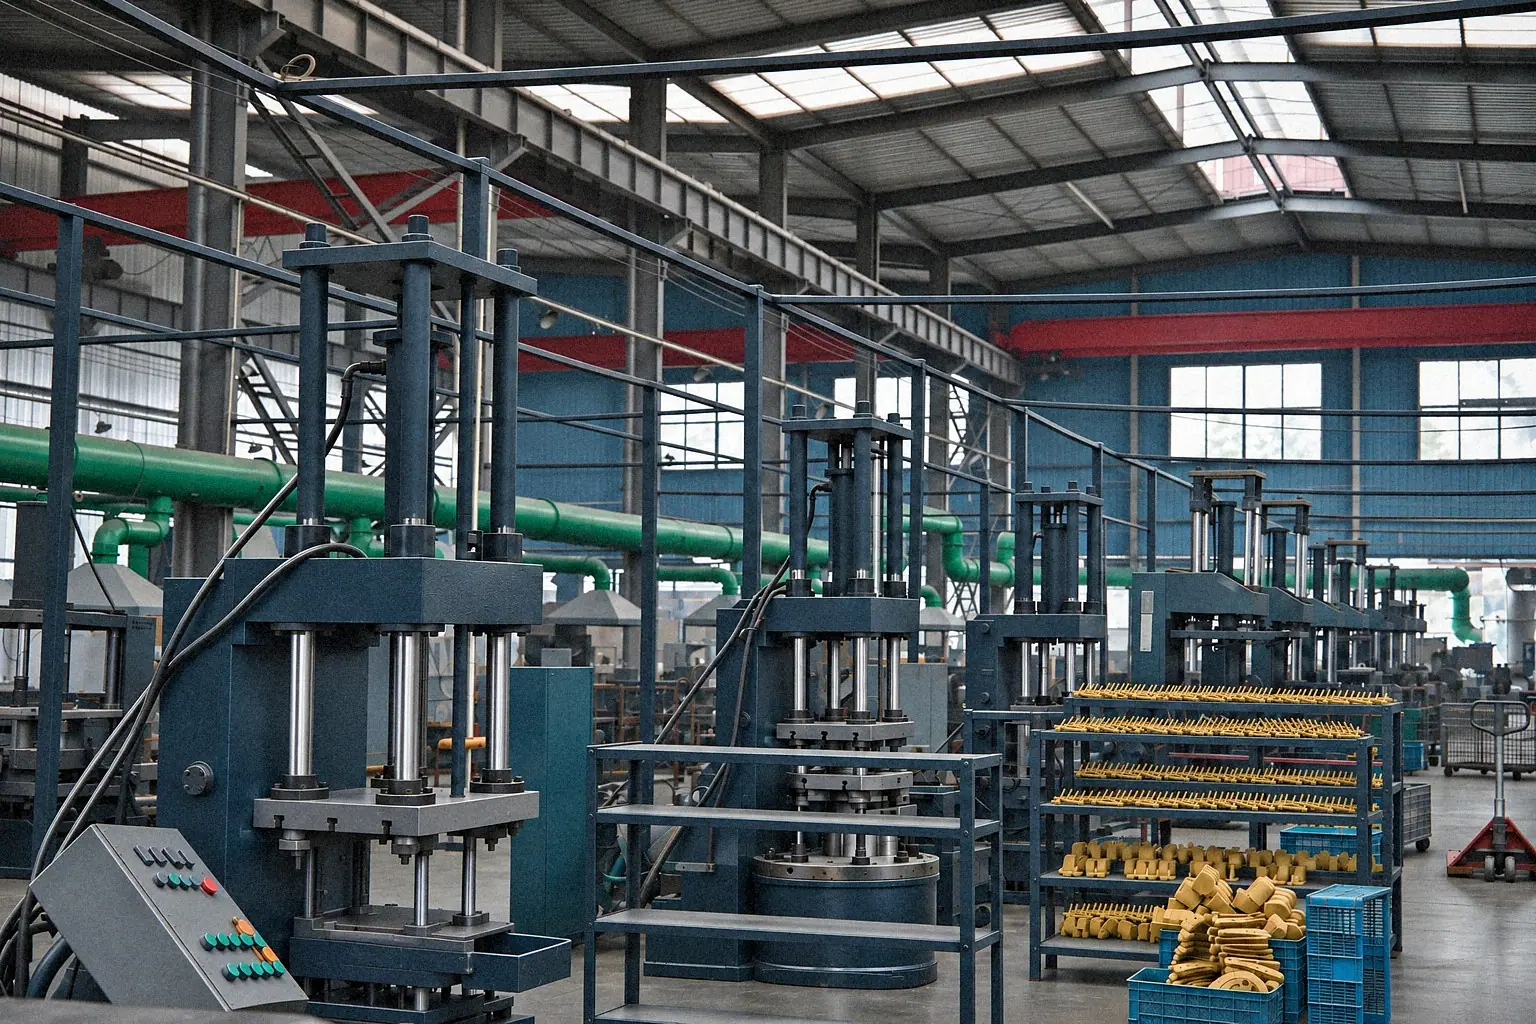
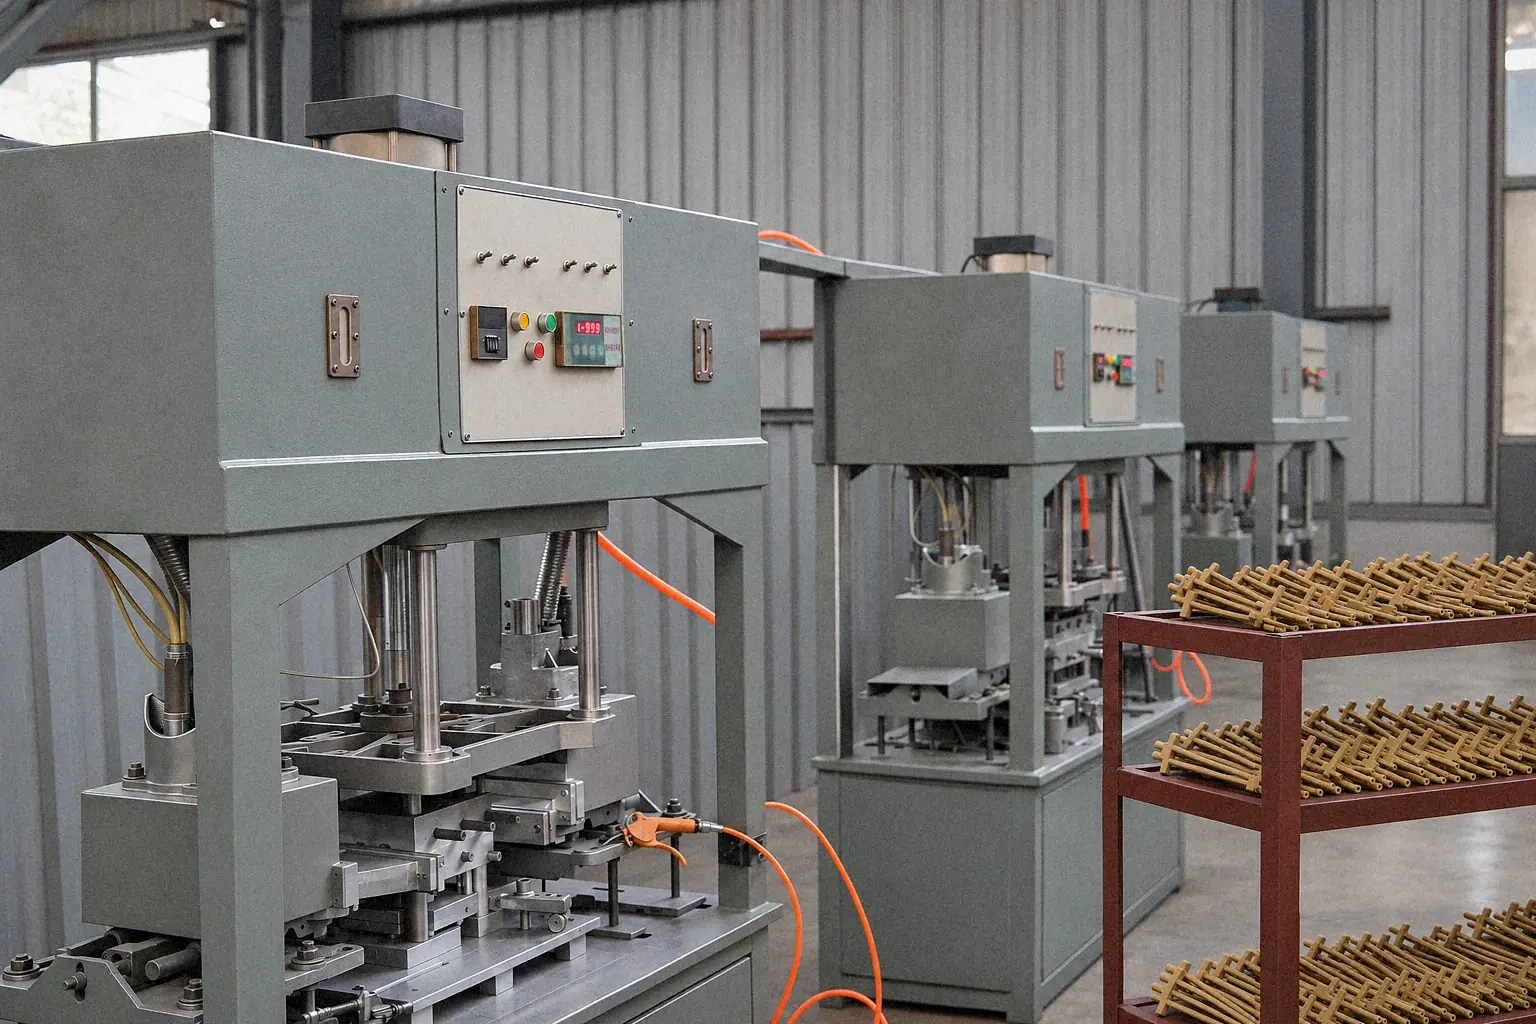
Bohua uses A356 and ZL114 for gravity and tilt-pour casting. The factory has 32 tilt-pour machines and 10 upright gravity casting machines. Some tilt-pour parts use sand cores. Molds are designed and made in-house.
For tilt-pour casting, walls are typically about 3 mm; with the gating designed for it, small areas near the gate can go down to 2.5 mm, which is the practical limit of the process. Send your wall map and section transitions so we can review this process-specific reference against your geometry before you fix the drawing.
| Your question | What to send | What happens next |
|---|---|---|
| Is my wall thickness castable? | The wall map, local thick sections, ribs, and transitions. | Send the geometry for a gravity casting design review; we will review filling and feeding with you. |
| Can my internal passages use cores? | Passage geometry, openings, and access needed for core removal and inspection. | Include the passages in your drawing review request so we can review core support and removal access. |
| Which surfaces need machining? | Functional datums, bores, threads, sealing faces, and required tolerances. | Use the drawing requirements checklist to separate cast and machined features before the stock and fixture review. |
| How should I specify acceptance after heat treatment? | The alloy, temper, mechanical requirements, specimen basis, and final inspection condition. | Use the heat-treatment acceptance guide to prepare the material and inspection requirements for review. |
Executive Summary
Gravity casting sits in the sweet spot between sand casting and high-pressure die casting. The drawing, the required properties and the annual volume decide the route for a specific part.
When to choose gravity casting
Choose gravity casting when the part is too structural for typical thin-wall die casting, too repeatability-sensitive for sand casting, and valuable enough to justify better tooling, tighter process control, and heat-treatable alloys such as A356.
Guide overview
Use the following design inputs to define the questions that need resolution before tooling. Keep process selection, material requirements, and acceptance decisions tied to the same drawing revision.
01 Process Selection
Compare gravity casting, die casting, and sand casting using real-world design and cost logic instead of generic process charts. Use the casting process selection guide for comparisons and Bohua's gravity casting manufacturing scope for factory capability.
02 Alloy Selection
Understand the practical differences between A356, ZL114, and ADC12 before you lock the drawing or RFQ package.
Keep alloy comparisons separate from supply scope. For Bohua's gravity and tilt-pour route, the confirmed alloys are A356 and ZL114. Use the A356 and ADC12 comparison for the material decision.
03 DFM Rules
Review wall thickness, draft, fillets, undercuts, parting lines, and gating strategy with gravity-casting-specific guidance.
| Design feature | Drawing input | Review decision |
|---|---|---|
| Wall layout | Nominal walls, local thick sections, transitions, ribs, and bosses. | Review the complete geometry for filling and feeding. Do not transfer a thin-wall value from another casting process. |
| Draft and parting line | Pull directions, no-draft surfaces, parting-line restrictions, and undercuts. | Agree how the mold opens and which surfaces need machining. Set draft for the actual geometry rather than a universal angle. |
| Fillets and junctions | Required radii, section junctions, and functional clearance limits. | Resolve abrupt section changes without altering the required assembly envelope. |
| Cores and passages | Internal passage geometry, openings, and surfaces that must remain accessible. | Review core support, removal access, and inspection access. |
| Machining datums and stock | As-cast references, finished datums, bores, threads, and sealing faces. | Agree stock allowance, fixture access, and measurement condition before tool design. |
| Gates and feeders | Protected surfaces and areas where attachment or removal is restricted. | Resolve tool layout and removal access before releasing the mold. |
Use the following general tolerance range only where a supplier has documented it for the selected process, geometry, and dimensions. For a Bohua review, use our separate references below and mark the tolerance needed on each feature.
04 Tolerances & Finish
Set as-cast expectations at CT8, avoid billet-style over-tolerancing, and specify secondary operations only where function requires it.
Separate as-cast tolerances from machined critical dimensions. Identify the required finish on each functional surface and state how it will be measured.
At Bohua
| Characteristic (unit where applicable) | Bohua reference | Condition |
|---|---|---|
| Minimum wall thickness (mm) | About 3 mm typical; 2.5 mm over small areas near the gate | Tilt-pour casting only; part geometry requires review. |
| As-cast tolerance grade | CT8 | As-cast condition; not the finished machining tolerance. |
| Machined critical dimensional tolerance (mm) | ±0.02 | Applies to critical dimensions after machining; mark those features and agree the tolerance for each remaining feature. |
| Core-making equipment (machines) | 10 hot-box core shooters | Some tilt-pour parts use sand cores. |
| Mold design and simulation | UG, SolidWorks, and AnyCasting | UG and SolidWorks for mold design; AnyCasting for casting simulation. |
State the required tolerance standard and edition on the drawing. Use the casting tolerance drawing and RFQ guide for the detailed specification.
05 Heat Treatment
See when T5 or T6 makes sense, what property gains are realistic, and why porosity control still matters first.
At Bohua, T5/T6 heat treatment is performed in-house. Define the temper, mechanical requirements, specimen basis, and inspection condition using the heat treatment and acceptance guide.
06 Quality Control
Cover common defects, traceability, and how to ask the right supplier evaluation questions.
Mark the critical zones and required evidence on the RFQ. Use the casting supplier evaluation checklist for qualification decisions.
Connect design decisions to quotation scope
Compare the same geometry, operations, and acceptance requirements before choosing a manufacturing route.
Real comparison should include tooling cost, yield, heat treatment, scrap risk, and the supplier's ability to explain defect modes before production starts.
What the guide covers
The full guide walks through alloy selection, DFM rules, tolerances, heat treatment, RFQ structure, and supplier-evaluation questions you can actually use in a sourcing meeting.
Use the linked topic guides for the detailed process and supplier decisions. The design review here focuses on the inputs needed before tooling.
Apply the design review to your RFQ
For A356, connect the wall sections and machining datums to the material, temper and specimen requirements.
Record unresolved items in the RFQ completeness check and use the quotation scope sheet to compare the same deliverables.
Include the released drawing, model, annual volume, tooling status, machined features, inspection requirements, and the person who approves design changes. For a part with internal passages, use the intake manifold manufacturing and RFQ guide to organize the relevant inputs.
If you want help applying the guide to your own part, send us a drawing and we'll review the alloy, process fit, and manufacturability.
Send your package through the casting RFQ page.
Using this design guide
Use the guide to prepare engineering questions and approval inputs for a specific part.
Who is this guide for?
It is written for design engineers, sourcing managers, quality teams, and OEM buyers evaluating aluminum gravity casting suppliers and process choices.
Do the process references guarantee part performance?
Alloy and process names referenced on this page are technical descriptors of casting options. They are not performance promises or supply commitments. Final part-specific performance, certification scope, and inspection plan are determined per RFQ review.
Find supporting checklists in the engineering and buyer resources.
Send your drawing for a gravity casting design review
Include wall sections, cores, datums, material requirements, and the acceptance plan. Submit the RFQ details, then email your drawing for a structured quote review. Send the drawing, target alloy, finishing scope, MOQ, and delivery timing. Bohua will review it like a real sourcing project, not a generic contact request. Our engineering team can recommend the right alloy, process, and design optimizations for your specific requirements.
Send your drawing →