Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Leak-Test Specification for Pressure-Tight Aluminum Castings
Specify the pressure boundary, manufacturing stage, test conditions, observation rule, sampling, and required records before quoting an immersion leak test. Bohua uses air-under-water immersion testing at 3 bar or more. The actual pressure, its basis, timing, temperature, and acceptance criteria must be agreed for the part; the pressure statement alone is not a complete specification.
On this page
- Define the part and pressure boundary first
- Write the immersion conditions into the specification
- Read the report from identity to disposition
- Check the fixture and preserve repeat-test history
- Keep dimensional and internal inspection separate
- Compare supplier reports against one requirement
- Send an acceptance specification with the RFQ
Define the part and pressure boundary first
An immersion specification must identify which cavity is pressurized, which surfaces are observed, and which manufacturing stage is being accepted. Ask the report to link its PASS result to that boundary and manufacturing stage.
A casting wall, a machined sealing face and an assembled joint are different potential leak paths. Mark the pressurized passages, connected ports, temporary plugs, and surfaces accessible for observation. Identify whether the requirement concerns leakage to the outside or isolation between passages; confirm that the proposed fixture evaluates the required boundary.
For a valve body, identify the passage pairs that must remain isolated. For a complete valve or pump assembly, define the assembly leak test separately from the body test.
Record the manufacturing state: as-cast, heat-treated, final-machined, coated or assembled. If impregnation or another approved treatment is allowed, identify when it occurred and the agreed retest requirement. If acceptance applies after a later machining operation, specify a test in that condition and link its result to the part.
For cooling passages, use the coolant water outlet RFQ inputs to prepare the drawing. Review Bohua gravity casting capabilities for the manufacturing route.
Download the review sheet: Leak-test report review worksheet (CSV). Use it to check each supplier report against your approved drawing and test procedure. It contains no preset acceptance limits.
Write the immersion conditions into the specification
Define pressure, timing, temperature, sampling, and visible-bubble acceptance in the approved procedure. Send the pressure value together with those conditions so we can review one complete test specification.
At Bohua
Bohua uses air-under-water immersion testing at 3 bar or more in its pressure-tightness testing room. The required conditions and acceptance rule are agreed for the project.
| Parameter and unit | What the buyer should define |
|---|---|
| Part and manufacturing stage | Drawing revision, cavity map, tested condition, and applicable machining or treatment sequence |
| Method and medium | Air inside the specified cavity, water immersion arrangement, and any required conditioning |
| Test pressure (bar) | Required pressure and permitted variation; explicitly identify gauge or absolute basis |
| Timing (s) | Separate pressure establishment or stabilization, hold, and observation periods |
| Temperature (°C) | Required part, air, and water conditions; identify which are controlled and recorded |
| Fixture and observation | Fixture revision, sealed ports, boundary, immersion orientation, visible surfaces, and access limitations |
| Visual acceptance | Define what observed bubble behavior constitutes rejection, where it is evaluated, and during which interval |
| Sampling (parts per lot or stated frequency) | Lot definition, sample selection, quantity, production frequency, and response to a failed sample |
| Disposition and records | Result format, repeat-test rules, treatment permissions, review responsibility, and release authorization |
The 3 bar or more statement is not a universal operating-pressure rating or an unlimited test range. Confirm the actual requirement against the part and fixture. Do not assign a numerical leak-rate result to a visible-bubble observation without an agreed, validated basis.
A missing field is a request for clarification, not proof that the physical part leaks. Resolve open requirements before using a result for acceptance.
At Bohua
In Bohua's immersion test, air escaping from a leaking submerged part produces visible bubbles in the water. The test pressure and holding time follow the customer's requirements. Identify the pressurized cavity, visible surfaces and manufacturing stage in the approved procedure.
Read the report from identity to disposition
Check that the report covers the supplied parts and the approved test conditions before relying on its pass/fail decision. Preserve the recorded observations and their requirement references.
| Record group | Evidence to check |
|---|---|
| Identity | Drawing revision, specimen or lot reference, lot quantity, sample identity, and manufacturing stage |
| Procedure and setup | Procedure revision, test station, fixture revision, sealed boundaries, and applicable verification records |
| Conditions | Actual pressure with unit and basis; timing and temperature records required by the procedure |
| Observation | Observed bubble behavior and location, observation interval, and any access limitation |
| Acceptance | Approved criterion and revision, recorded decision, and connection to the actual observation |
| Exceptions | Original failed or invalid record, reason for repeat testing, correction or treatment, and authorization |
| Release | Inspector, reviewer, date, linked lot or specimen, and final disposition |
Use this checklist to specify your report fields. Enter actual measurements from the test and acceptance limits from the approved procedure when completing the report.
State whether the requirement applies to every part, selected samples or a qualification batch. A lot summary and a serial-number record answer different traceability questions. Agree on the record granularity, sampling plan and response to a failure rather than inferring them from the word "tested."
Check the fixture and preserve repeat-test history
An unexpected result should trigger a review of the part and test system together. Check temporary plugs, seals, the fixture revision and the applicable verification records.
- Locate the observation. Record whether bubbles appear at a temporary seal, a fixture connection, a casting wall, or another identified location. Keep the observation separate from an assumed cause.
- Check the conditions. Compare actual pressure, timing, temperature, orientation, and manufacturing state with the approved procedure.
- Document the action. Record any fixture correction, part treatment, or other authorized change before repeating the test.
- Retain the original result. Link the repeat test to its reason and authorization. Apply the agreed release rule to the affected sample or lot.
At Bohua, impregnation requires customer approval and is performed by a qualified outside provider. Define the treatment record and retest requirement before it is used. See the impregnation approval policy.
At Bohua
Bohua makes the fixtures used for its air-under-water leak testing in-house.
Specify the ports to seal and the wall surfaces that must remain visible. When bubbles appear near a temporary seal, locate the source before assigning the failure to the casting.
Keep dimensional and internal inspection separate
CMM and X-ray reports support different acceptance questions from immersion testing. Keep each report linked to the same specimen or lot and judge it against its own requirement.
At Bohua
Confirmed equipment includes Hexagon Global S and NANO Metrology CMMs, plus Unicomp UNC-160 and Y.MU2000-D X-ray systems. These resources are listed in the quality-control equipment and record guide.

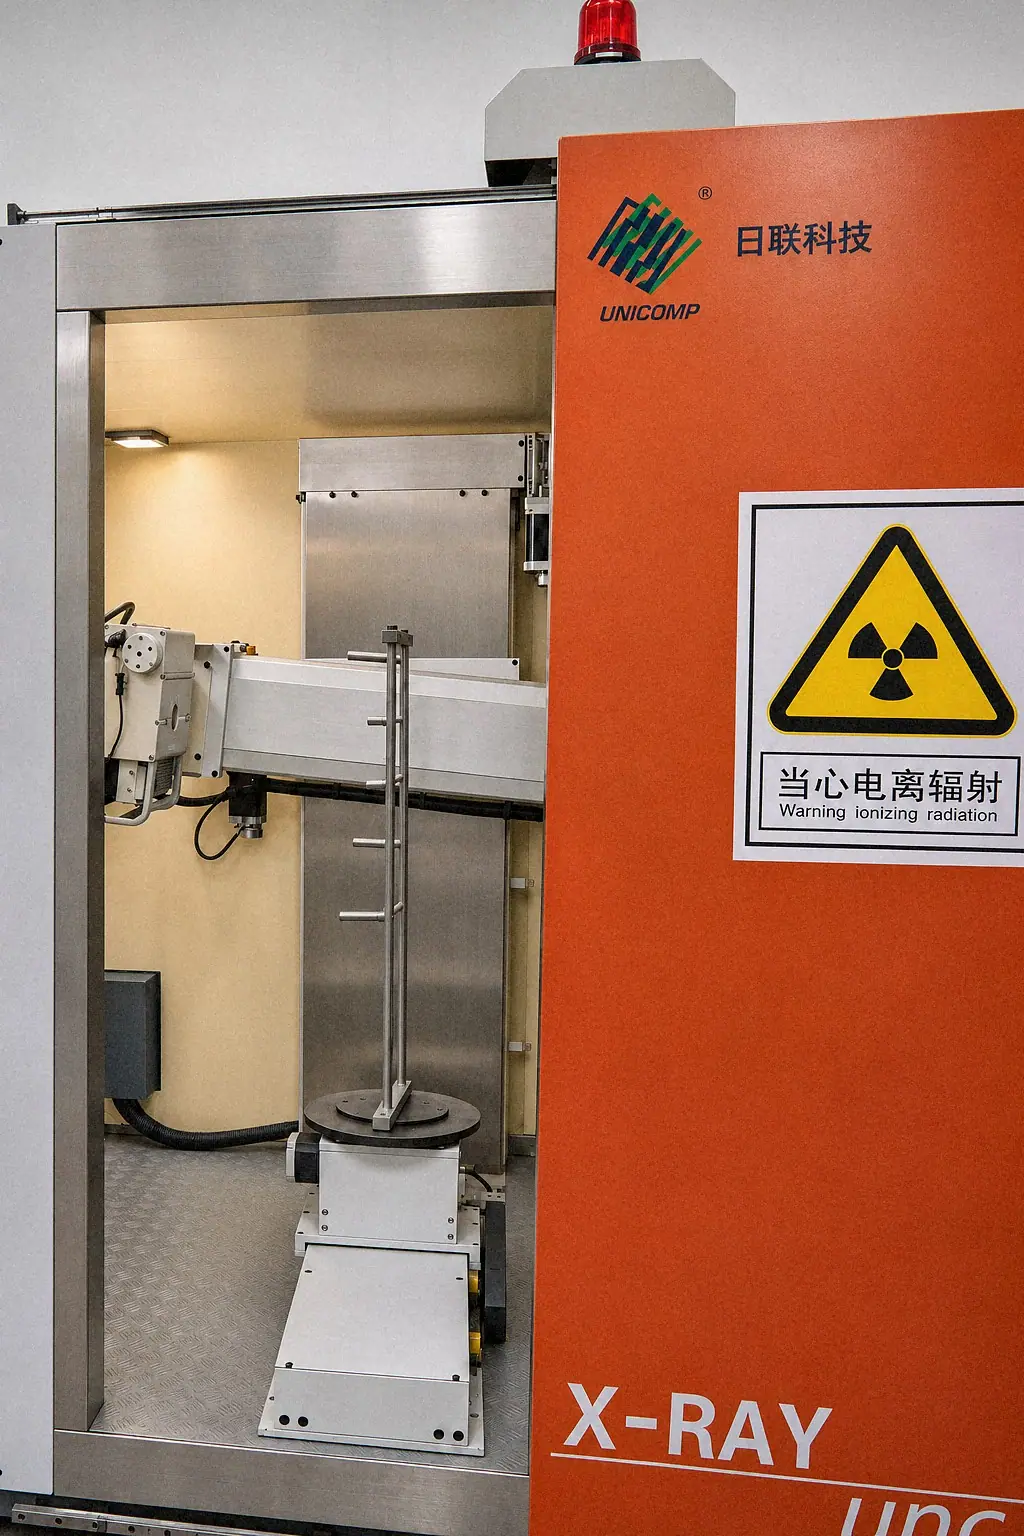
The photographs show dimensional and internal inspection equipment. Request the separate immersion report to review the tested boundary, conditions and leak-test result.
At Bohua
Bohua uses digital X-ray imaging and grades the indications to GB/T 11346-2018, with acceptance set by the customer.
Read that internal-inspection result separately from the immersion result. The porosity inspection guide explains how to separate the questions answered by each method.
Compare supplier reports against one requirement
Compare the same boundary, manufacturing stage, and approved immersion procedure across suppliers. Check the conditions behind each PASS label using the same inspection-scope checklist.
- Check the part revision, final condition, and tested passage map.
- Compare pressure basis, timing stages, temperature conditions, fixture seals, and observation access.
- Check the same visual acceptance rule and the same sampling obligation.
- Confirm whether reports cover individual parts, selected samples, or only initial qualification.
- Review original failures, authorized treatments, repeat tests, and final release decisions.
Use the buyer's approved drawing and test procedure as the comparison baseline. Ask the quotation to identify fixture scope, setup verification, production testing, report delivery, and any approved retesting. Document differences before accepting the scope.
At Bohua
Whether Bohua immersion-tests every part or a sample is determined by the customer's requirements.
State the selected coverage in the order and report. The method name and test-pressure statement alone do not establish how many parts were tested.
Send an acceptance specification with the RFQ
Attach the drawing, cavity map, required delivered condition, and immersion specification to the quotation request. Include sample quantity, annual volume, report format, traceability requirements, and the treatment approval policy.
For sourcing scope, read Bohua pressure-tight casting manufacturing scope. For the rest of the drawing package, use the aluminum casting RFQ checklist, then send the casting and test-scope quotation request.
Send your drawing and leak-test requirements
Include the drawing revision, material, annual volume, test pressure, hold time, acceptance criterion and required records. Bohua tests by air-under-water immersion at 3 bar or more. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →