Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
LPDC Casting Defects: 5 Root Causes & Fixes
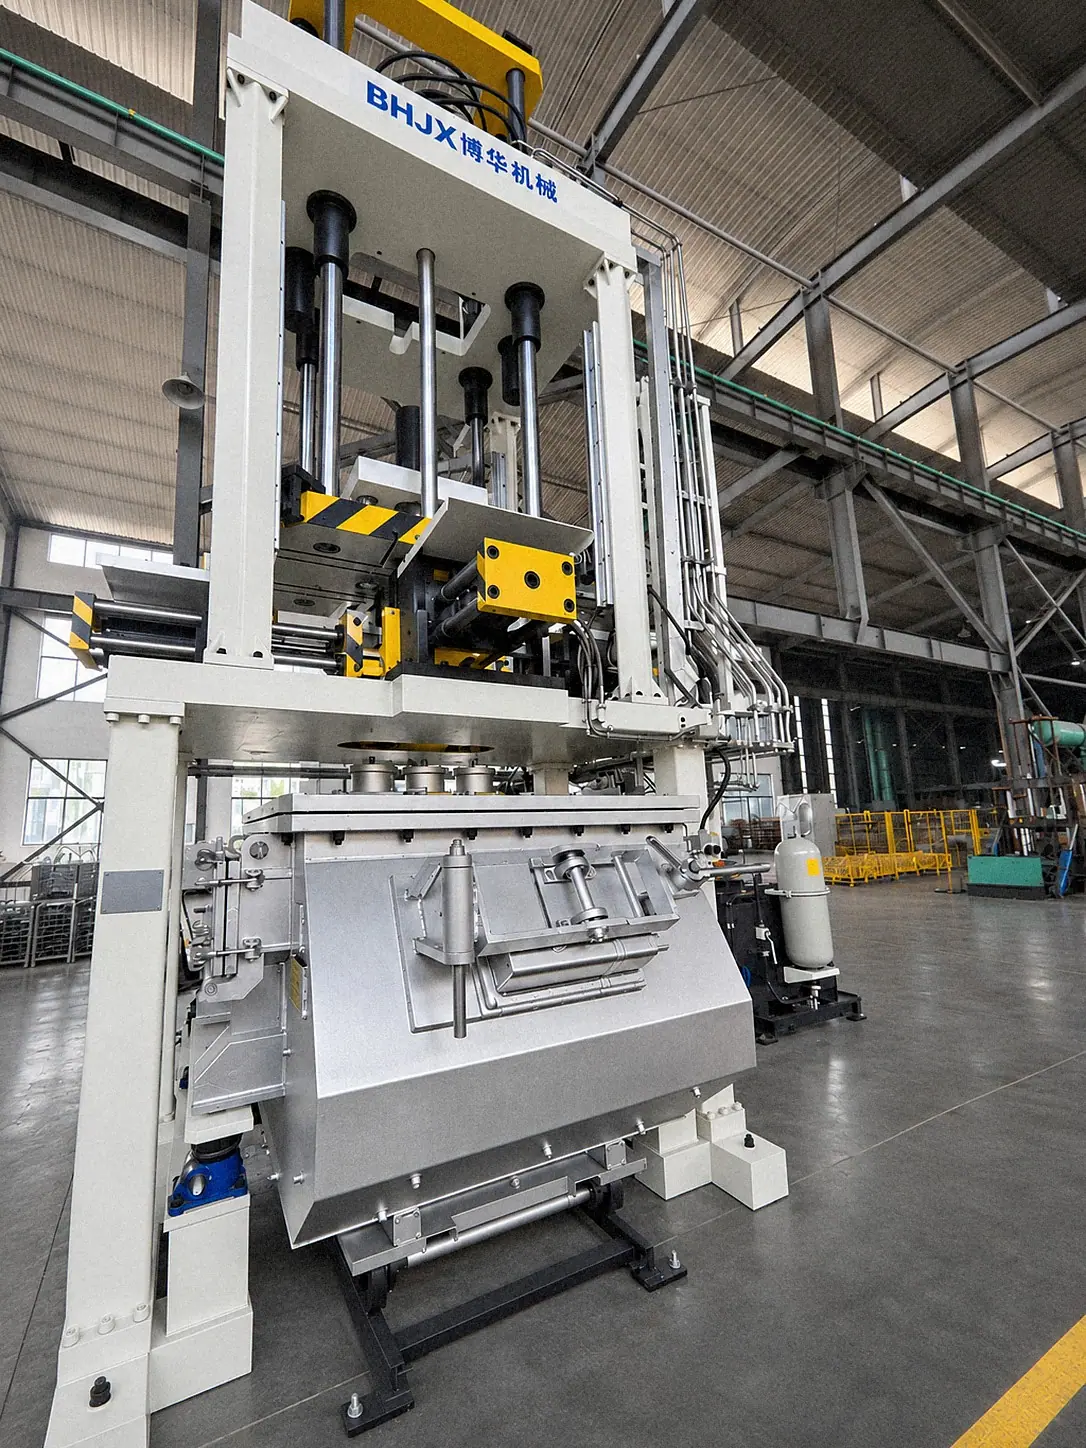
Start LPDC defect troubleshooting by separating cold shuts, misruns, gas porosity, shrinkage, and hot cracking. Match the observed location to pressure, temperature, feeding, and inspection evidence before changing settings. Bohua has operated low-pressure casting in-house since 2014; this guide separates general diagnostic options from its confirmed inspection equipment.
On this page
- Start with the observed defect
- What Causes Cold Shuts in LPDC Castings — and How to Confirm It
- Misruns: Low-Fill Defects vs. Cold Shut — How to Tell the Difference
- Gas Porosity in Low-Pressure Die Casting: Hydrogen vs. Air Entrapment
- Shrinkage Porosity: Why Solidification Sequence Matters in LPDC
- Hot Cracking (Hot Tearing) in Aluminum LPDC: Alloy, Geometry, and Die Factors
- Diagnostic Methods: Dye Penetrant, X-ray CT, Cross-Section Macroetch, and What Each Reveals
- Frequently Asked Questions
- Why Engineers Work With Bohua Casting
- Send a drawing-linked investigation package
Start with the observed defect
Start LPDC troubleshooting with the defect location, fill history, thermal history, and inspection evidence. Compare the observed appearance with the process records to identify which condition failed. Five of the most common LPDC defects look superficially similar on a visual inspection but require different corrective actions. Misidentifying a cold shut as a misrun, or confusing gas porosity with shrinkage porosity, leads to process changes that do nothing or create a second defect mode. This post covers the five main defect types — cold shut, misrun, gas porosity, shrinkage porosity, and hot cracking — with how each presents, root causes, and what you actually adjust to fix it.
Diagnose by symptom and apply the right corrective action.
The causes and adjustments below are investigation options, not universal machine settings. Validate changes against the alloy, geometry, tooling, and approved process window. A hotter melt or faster fill may introduce another defect.
What Causes Cold Shuts in LPDC Castings — and How to Confirm It
A cold shut is a planar discontinuity where two metal fronts meet but fail to fuse. The part looks filled, but a faint line or seam is visible on the surface. Cross-section macroetch reveals a distinct unbonded interface — both sides are solid but the streams never achieved metallurgical bonding.
Cold shuts form when the metal front temperature drops below the liquidus before two streams converge. Three primary mechanisms:
Filling pressure profile too slow in the early fill phase. If the pressure ramp is gradual, metal in thin sections loses heat before the cavity is full. The front solidifies partially and metal arriving behind it cannot rewet the oxide skin on the leading edge.
Die temperature too low at the flow path. Confirm with thermocouple data or IR measurement; high shot-to-shot variation on the thin-section thermocouple indicates the die is not at thermal equilibrium at cycle start.
Metal temperature too low. Compare the measured temperature and transfer losses with the qualified process window for the alloy and flow path.
Corrective actions: Review the filling pressure ramp, metal temperature, and local die temperatures together. Change one controlled variable at a time within the approved process window, then check both fill completion and porosity.
Detection: Dye penetrant can reveal discontinuities that open to a suitably prepared surface. Sub-surface cold shuts require X-ray or CT; the characteristic CT signature is a planar, low-density line tracing the meeting of two flow fronts. X-ray sensitivity depends on orientation and geometry; a qualified technique and confirmatory evidence are needed, and a planar CT indication alone does not identify its cause.
At Bohua
Bohua’s furnace temperature is displayed continuously from a probe with a custom silicon carbide protection tube.
Its quality inspectors spot-check the mold core and mold wall with an infrared thermometer.
Ask for the temperatures relevant to the affected part and tool when investigating a cold shut; use the part-specific process conditions rather than a single published temperature window.
Misruns: Low-Fill Defects vs. Cold Shut — How to Tell the Difference
A misrun is an incomplete fill — the cavity was not full when solidification stopped. Unlike a cold shut, a misrun leaves an obvious open edge. For an accessible surface indication, compare the typical appearance: a cold shut is a continuous surface with a detectable seam; a misrun leaves a rough, rounded edge. Confirm the mechanism with the inspection evidence rather than appearance alone.
Root causes:
Insufficient filling pressure. If pressure is at the low end and back-pressure from venting resistance is higher than expected, the metal column stops before the cavity is full.
Vent blockage or insufficient venting. Clogged parting-line vents stall the fill — commonly misdiagnosed as insufficient pressure. Adding pressure then causes flash. Check vent cross-section and condition before adding pressure.
Metal temperature at the low end with a long thin flow path. A misrun consistently at the cavity extremity is usually temperature or flow-path-length, not an overall pressure issue.
Corrective actions: First confirm the pressure trace, vent condition and thermal history. Where these checks identify insufficient fill drive, restricted venting or premature chilling, evaluate the applicable actions below within the approved process window. Tool changes require a design review.
Increase filling pressure incrementally, confirming actual pressure at the die (line losses matter); clean and enlarge parting-line vents; add overflow wells at last-to-fill locations; increase metal temperature.
The diagnostic discipline matters: cold shut drives toward temperature and ramp rate; misrun drives toward fill pressure, venting, and overflow placement.
Gas Porosity in Low-Pressure Die Casting: Hydrogen vs. Air Entrapment
Gas porosity appears as rounded or slightly elongated pores with smooth walls that do not follow solidification contours on CT — the key distinction from shrinkage porosity.
Pore shape is an initial clue. Gas and shrinkage can coexist, so compare the indications with melt-quality and solidification evidence.
Hydrogen porosity originates in the melt. Liquid aluminum dissolves hydrogen from moisture in furnace atmosphere, wet charge materials, or contaminated tools. On solidification, hydrogen solubility drops sharply and rejected gas nucleates into fine, distributed spherical pores. Specify the hydrogen acceptance limit and measurement method for the actual process. A reduced pressure test is an indirect melt-quality check; it is not interchangeable with a quantitative hydrogen measurement.
Air entrapment occurs during fill. Turbulence at the gate transition, irregular pressure steps, or folding of the metal front can trap air. Air entrapment pores tend to be larger, less uniformly distributed, and concentrated near the gate or at abrupt section changes.
Corrective actions for hydrogen: Review degassing effectiveness, charge and tool dryness, furnace moisture, and measurement records before changing the melt-treatment plan.
Corrective actions for air entrapment: Where the evidence confirms an entrainment problem and CT has located a trap, evaluate these changes within the approved process and tooling design. Review the filling pressure profile for abrupt steps or pressure spikes; optimize gate geometry for laminar flow; add overflow wells and vents at CT-identified trap locations. Laminar flow is a design objective to validate, not a result established by changing the gate alone.
Improving melt degassing will not fix air entrapment, and optimizing fill profile will not fix hydrogen porosity. Use pore location and morphology together with melt records and a suitable confirmatory examination.
Define pore acceptance separately with the porosity inspection and acceptance guide.
At Bohua
Bohua accepts a reduced-pressure sample when its surface is slightly concave and its cut section is essentially free of visible pores.
For flux-assisted dross removal, Bohua raises the baffle to form a vortex.
For rotary degassing, the baffle is lowered to suppress the vortex.
Use the melt-treatment and reduced-pressure checks alongside the part’s investigation records; this visual sample assessment does not supply a numerical hydrogen content or an LPDC filling-pressure setting.
Shrinkage Porosity: Why Solidification Sequence Matters in LPDC
Shrinkage porosity forms where liquid metal cannot feed volume contraction during solidification. CT shows irregular, angular, or dendritic voids with rough internal surfaces — the clearest distinction from gas porosity — concentrated in the last-to-solidify regions.
In LPDC, if the gate remains liquid while the casting body solidifies, the pressurized melt column feeds shrinkage. This advantage breaks down when:
Solidification sequence is inverted. A thick boss surrounded by already-frozen thinner walls is isolated from the gate before it is fully solid. No holding pressure compensates for a severed feed path.
Holding pressure is insufficient or holding time too short. After fill, the pressure and hold duration must keep feeding effective until the required solidification stage. Dropping holding pressure before the gate solidifies drains the feed path too early.
Die temperature imbalance causes premature gate freeze. If the gate area runs cooler than the casting body it solidifies first and cuts off feed — common when die cooling in the sprue or gate zone is too aggressive.
Corrective actions: Compare solidification evidence with the pressure and cooling records. Review hold duration, gate cooling, and isolated hot spots. Any simulation must represent the actual tooling and boundary conditions.
Micro-shrinkage near the gate requires checking both feed-path continuity and local solidification conditions. Process parameters can reduce severity but rarely eliminate it without die thermal management or geometry changes.
Hot Cracking (Hot Tearing) in Aluminum LPDC: Alloy, Geometry, and Die Factors
Hot cracking forms when a vulnerable, partially solidified region cannot accommodate contraction and restraint in the brittle temperature range (BTR). The following describes typical morphology, not a sufficient diagnosis: Hot cracks are irregular, branching, and oxidized — distinguishing them from cold cracks, which are smoother and form after full solidification. Use formation timing and section evidence to distinguish hot tearing from later cracking; surface oxidation also depends on exposure.
Alloy susceptibility. Review the actual alloy chemistry and melt-treatment records against the material specification. Do not attribute a crack to a modifier without supporting evidence.
Geometry. Hot cracking concentrates at high-constraint features: fillets with insufficient radius, abrupt section changes, thin ribs attached to thick sections, and bosses at the junction of walls cooling at different rates.
Die ejection and die temperature. Premature ejection while the casting is still in the BTR — or ejection pins applying force at a hot partially solid region — cause hot tears. Verify ejection timing against thermocouple data at the crack location. Die temperature asymmetry adds differential contraction stress to the solidifying casting.
Corrective actions: Increase fillet radii at crack-prone junctions; adjust die cooling to reduce temperature differential; delay ejection until the affected area is below a safe threshold (confirmed by thermocouple); review Sr modifier levels; add a radius or wall taper to reduce constraint.
If cracking develops as tooling ages, inspect tool condition, geometry, cooling, and ejection history before attributing it to wear. Inspect with a radius gauge or CMM; if the as-worn radius is below the drawing minimum, die rework is the corrective action.
Diagnostic Methods: Dye Penetrant, X-ray CT, Cross-Section Macroetch, and What Each Reveals
Picking the right inspection method before starting process changes saves time.
Dye penetrant testing (DPT / FPI): Detects surface-breaking discontinuities on suitably prepared, nonporous surfaces. Does not reveal subsurface porosity. Use as a first-pass surface defect screen.
2D X-ray radiography: Reveals internal porosity as density variations. Limited ability to distinguish gas from shrinkage by morphology, and cannot accurately locate a defect spatially through a thick section.
X-ray CT (computed tomography): Provides three-dimensional internal information within the resolution and contrast of the qualified scan. Evaluate pore shape alongside process evidence to identify the mechanism, then assess fatigue acceptance against the part requirements.
Cross-section macroetch: Sectioning, polishing, and etching with Keller's or Barker's reagent reveals grain structure, cold shuts, flow lines, and shrinkage. Destructive but high local detail. Most useful as a confirm step after CT has located the defect.
Establishing acceptance criteria — maximum pore diameter, maximum volume fraction, exclusion zone near critical surfaces — in the control plan before production starts avoids disputes later.
Use these general diagnostic methods to define your investigation needs. For CT or dye penetrant testing, confirm the service route before adding either method to your order.
Source: ASNT: Liquid Penetrant Testing.
Source: ASNT: Radiographic Testing.
Specify radiographic zones and records using the digital radiography RFQ guide.
Frequently Asked Questions
What is the difference between a cold shut and a misrun in LPDC, and does the fix differ?
Yes, the fixes differ. A cold shut is a complete fill where two fronts did not fuse — no missing material, but an unbonded interface. A misrun is an incomplete fill. Cold shut correction focuses on die temperature, metal temperature, and fill pressure ramp rate. Misrun correction focuses on fill pressure, venting, and overflow well placement. Applying the wrong fix typically changes nothing and can introduce a second defect mode.
How do I know if CT porosity is gas or shrinkage — does it matter for the part?
Gas pores are round or slightly elongated with smooth walls; shrinkage pores are angular, branching, or dendritic with rough internal surfaces. These are typical clues, not a definitive separation. Evaluate mixed mechanisms and the local loading before setting acceptance limits.
What filling pressure profile changes reduce cold shuts without increasing gas entrapment?
If records confirm premature freezing during early fill and show that the ramp is too slow, evaluate the following change within the approved process window. Increase the pressure ramp rate during the initial fill phase rather than raising total filling pressure. A faster pressure rise gets metal into thin sections before it chills; a higher absolute fill pressure increases gate velocity, turbulence, and air entrapment risk. Verify the revised profile against the actual controller, tooling, and observed fill behavior.
Why does hot cracking appear on older tools from the same design?
Tool wear is one hypothesis to check. Two nominally identical dies wear differently depending on die steel hardness, coating maintenance, and whether thermal fatigue cracks were dressed but not fully restored to original radius. Inspect with a radius gauge or CMM; below-drawing-minimum radius means die rework.
Is micro-shrinkage near the gate a design or process problem?
Check both. Compare the local solidification sequence with the actual pressure and cooling traces. Where these records confirm premature gate freeze caused by excessive gate cooling or an inadequate feed path, the following explanation applies:
Micro-shrinkage at the gate transition means the gate is solidifying before it has fully fed the casting body.
Extending holding time or increasing holding pressure can reduce severity but rarely eliminates it.
Permanent correction requires reducing die cooling at the gate or a geometry change to improve the feed path to the last-to-solidify region.
Do not apply this diagnosis from defect location alone. Validate the correction against the observed thermal history and feeding path.
How do I write a corrective action for cold shut defects that an automotive SQE will actually accept?
An automotive SQE does not accept a generic statement such as operator training improved. Document measurement-based root cause identification, the specific process change, and verification data. Record the measured parameter, approved limit, adjustment, inspection method, sample size, and acceptance criterion. Connect the corrective action to a measurable process parameter and show the data.
Why Engineers Work With Bohua Casting
Bohua Casting operates under an NQA-certified IATF 16949 quality management system.
Bohua has operated low-pressure casting in-house since 2014. To scope an investigation using our equipment below, send the defect location, process records and inspection evidence needed to verify the suspected cause.
At Bohua
| Item | Confirmed fact (start year; test pressure: bar) | Boundary |
|---|---|---|
| LPDC | In-house since 2014 | Process settings are specific to the drawing and tooling |
| Melt checks | Oxford optical emission spectrometer; vacuum hydrogen analyzer | Specify the required measurements and records |
| Internal inspection | Unicomp UNC-160 and Y.MU2000-D X-ray systems | Agree zones, technique, and acceptance |
| Dimensions | Hexagon Global S and NANO Metrology CMM systems | Specify datums and critical features |
| Leak testing | Air-under-water immersion; test pressure 3 bar or more | Agree pressure in bar, duration, fixture, and acceptance |
The certification covers the 2016 edition and is valid through November 20, 2027. ISO 9001 requirements are incorporated within the IATF 16949 system; Bohua does not currently hold a separate ISO 9001 certificate. Tool design and manufacture are in-house; Bohua uses UG and SolidWorks for design and AnyCasting for casting simulation.
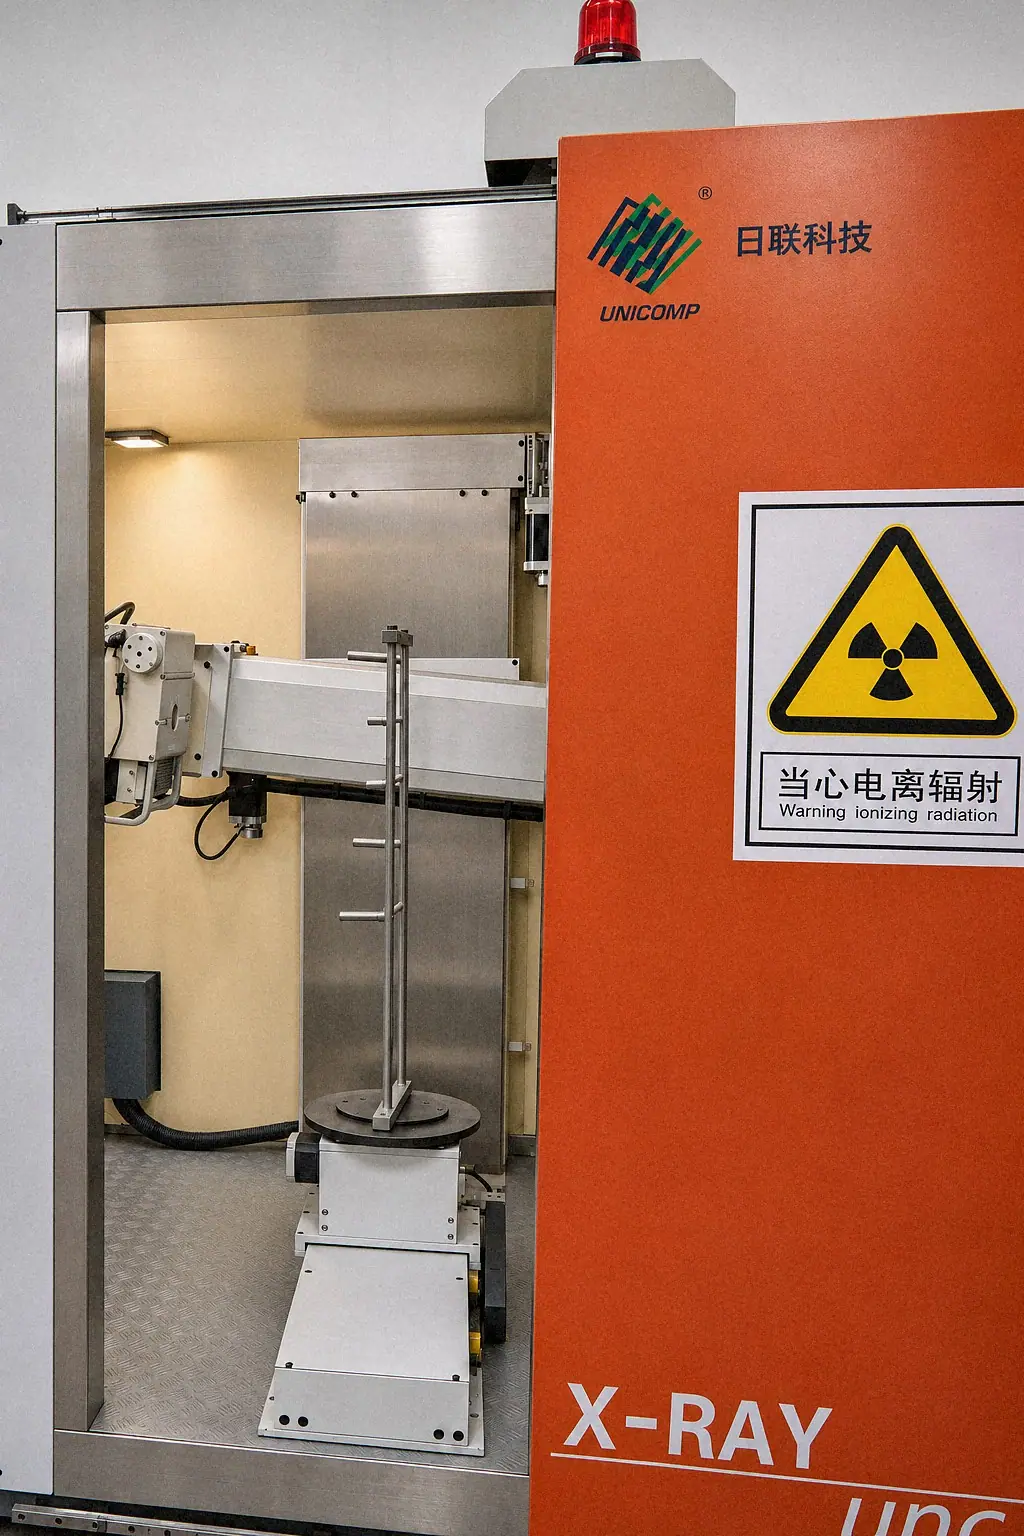
See Bohua low-pressure casting capabilities and quality-control equipment and inspection scope. For coolant water outlet casting review, identify fluid walls and machined sealing zones in the evidence package.
Send a drawing-linked investigation package
Send the drawing revision, alloy requirement, defect photographs with scale, affected location, manufacturing stage, and available pressure, temperature, and inspection records.
Use request a casting review for the project inputs. Use the general casting defect identification guide when the defect type remains uncertain.
Send drawings and inspection requirements
Include the drawing revision, alloy, annual volume, critical zones, and required inspection records. Submit the RFQ details, then email your drawing for a structured quote review. Send the drawing, target alloy, finishing scope, MOQ, and delivery timing. Bohua will review it like a real sourcing project, not a generic contact request. Our engineering team can recommend the right alloy, process, and design optimizations for your specific requirements.
Send your drawing →