Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering resource
Aluminum Casting Supplier Capability Sheet
Bohua supplies aluminum castings from its own factory in Ningbo, with an export team and casting experience since 1994. This capability sheet separates annual shipments from capacity, lists equipment and inspection resources, and states the conditions for tilt-pour ranges. Use it to screen suitability before requesting part-specific approval evidence.
On this page
Bohua supplier capability summary
Bohua is a manufacturer with its own factory and export team in Ningbo, China. Use this sheet for supplier screening, then check the proposed route and acceptance requirements against your drawing.
Sheet revision: November 10, 2026. Scope: company facts, manufacturing resources, and inspection capabilities. For your order, agree the part-approval evidence and production allocation separately after reviewing the drawing and demand.
Share with your quality and engineering team: Bohua supplier capability sheet (PDF).
| Item (unit where applicable) | Bohua fact |
|---|---|
| Legal entity | Ningbo Bohua Mechanical Parts Co., Ltd. |
| Location | Ningbo, Zhejiang, China |
| Operating model | Manufacturer with its own factory and export team; buyers work directly with the plant. |
| Casting and export history (start year) | 1994 |
| Employees (people) | More than 100 |
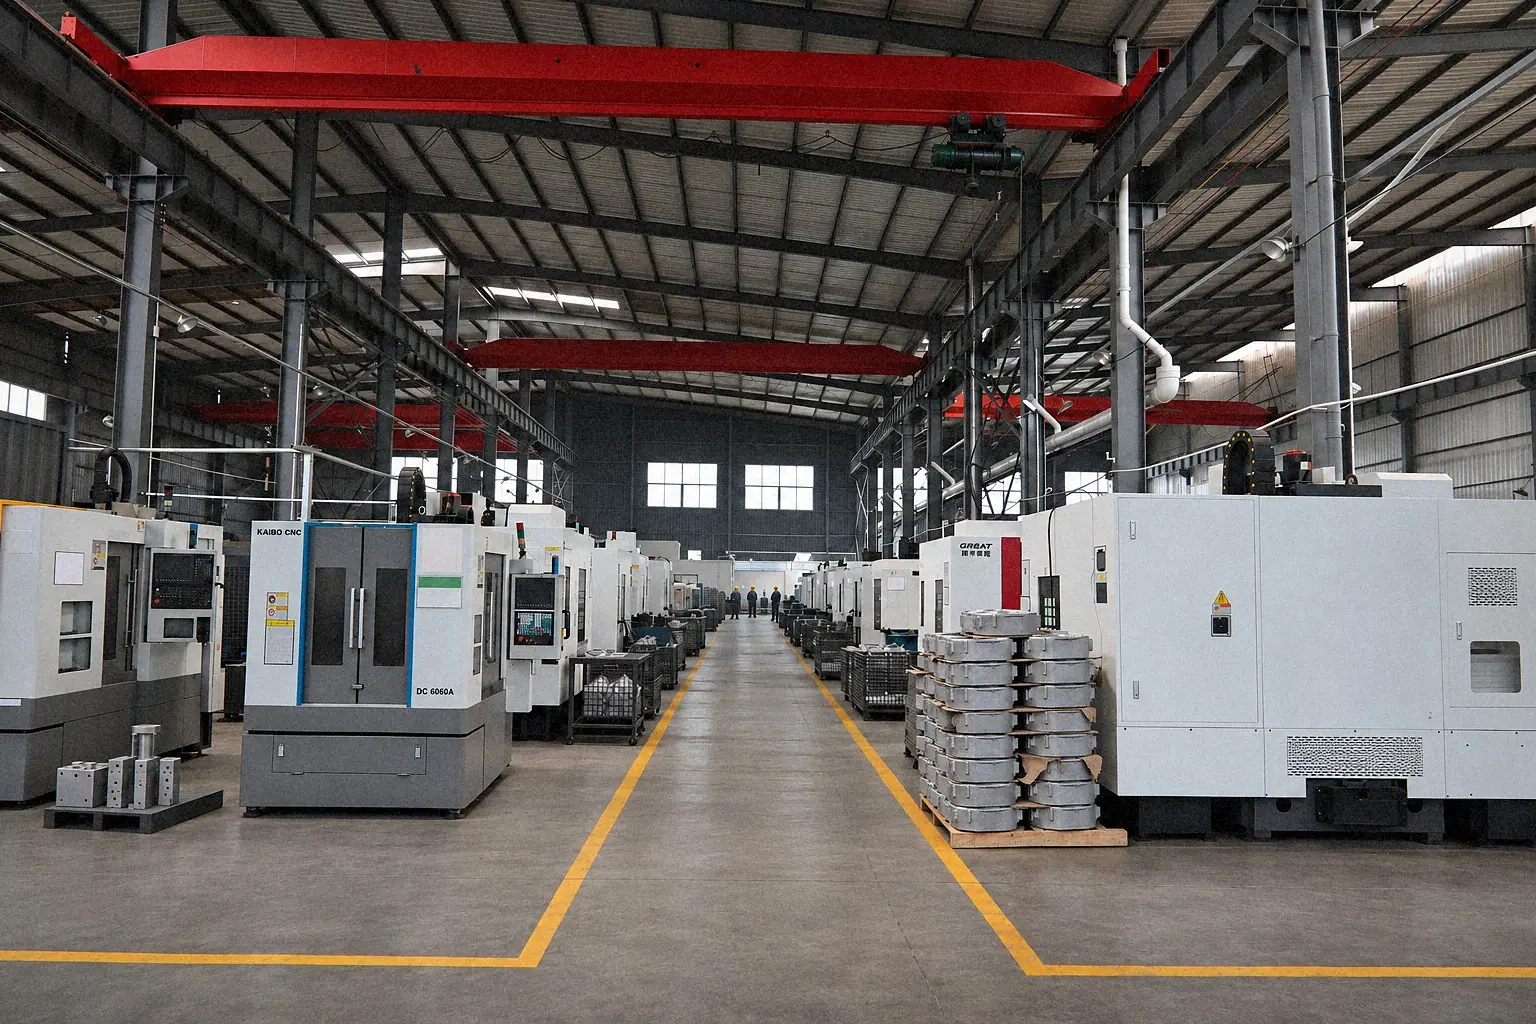
| Site area (m²) | About 16,300; casting, core making, tooling, T5/T6 heat treatment, CNC machining, and inspection share the same site. |
| Annual shipments (parts/year) | About 3–4 million |
| Production capacity (parts/year) | 5–7 million; capacity is separate from actual annual shipments. |
| Export share (% of sales) | About 70 |
| Order basis | Quoted by annual volume; small batches negotiable. |
| Contact | Linda, Export Sales; linda@ningbobohua.com |
Processes, equipment, and in-house operations
Bohua focuses on gravity casting and tilt-pour casting. Use the resources below for supplier screening, then send your demand and target timing so we can review availability for your order.
| Process or resource | Equipment count (machines) | Scope and conditions |
|---|---|---|
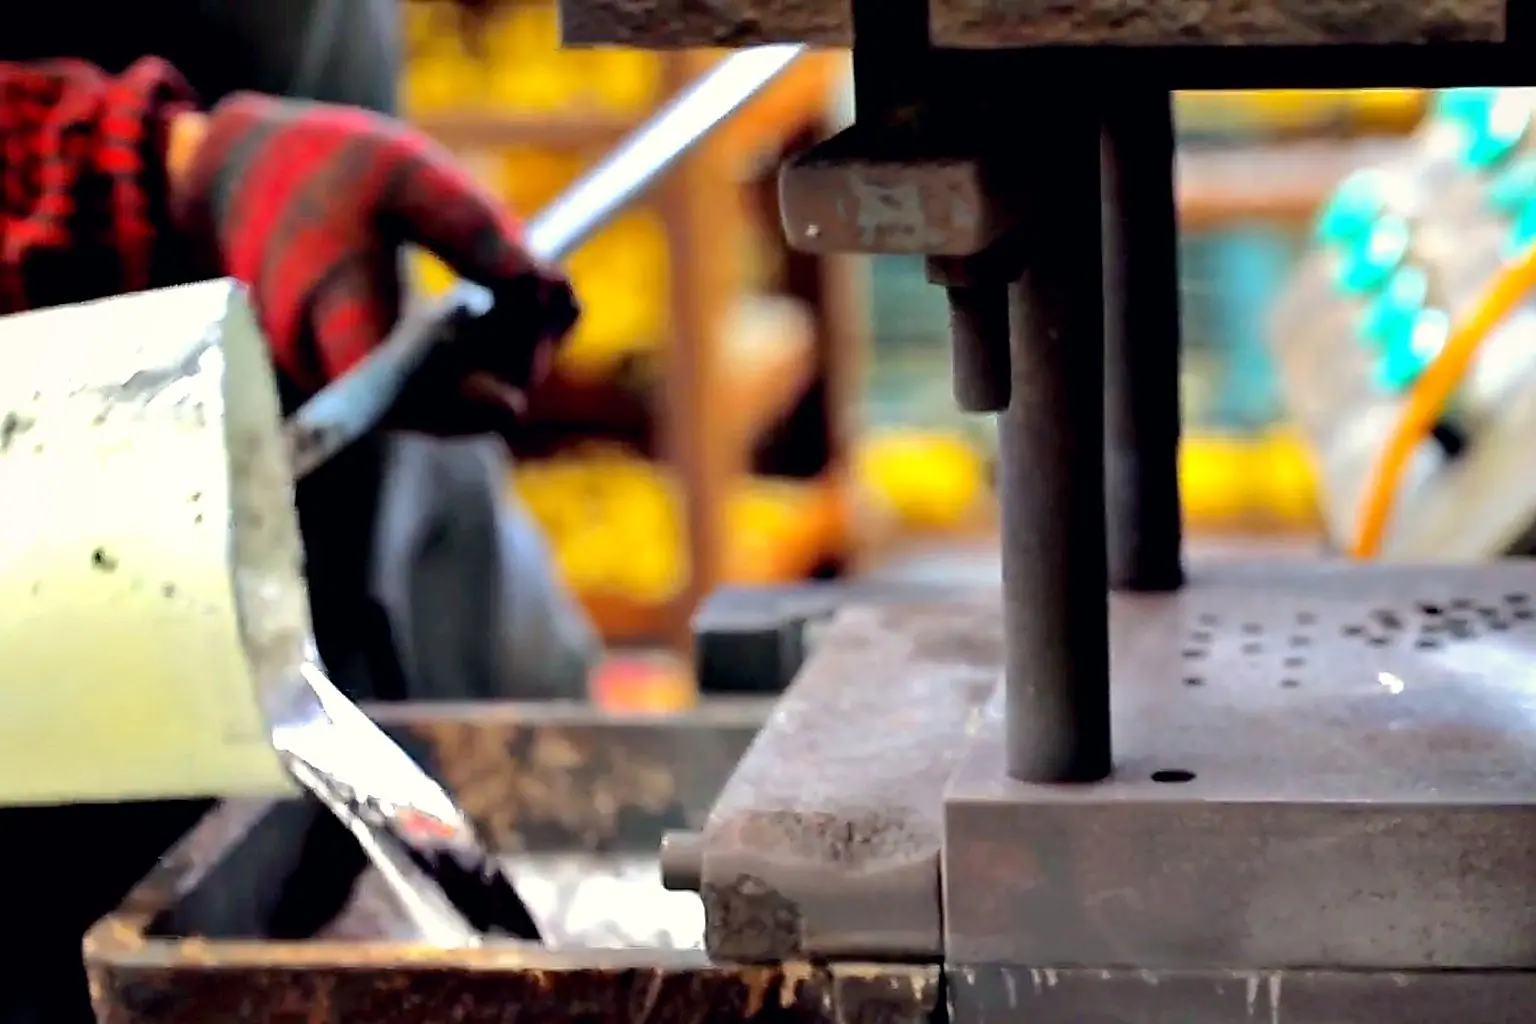
| Tilt-pour casting | 32 | Some machines are designed and built in-house. |
| Upright gravity casting | 10 | In-house gravity casting. |
| Hot-box core shooting | 10 | Sand cores are used for some tilt-pour parts. |
| Die casting | 2 | Machine sizes are listed separately below. |
| Vertical machining centers | 16 | In-house machining. |
| CNC engraving and milling machines | 2 | In-house machining. |
| CNC lathes | 22 | In-house machining. |
| Large lathes | 2 | In-house machining. |
| Tooling workshop equipment | 17 | Molds are designed and made in-house. |
| Machine size (t) | Count (machines) |
|---|---|
| 280 | 1 |
| 450 | 1 |
| Operation | Bohua scope |
|---|---|
| Low-pressure casting | In-house since 2014. |
| Sand casting | Done in-house. |
| Gravity and tilt-pour alloys | A356 and ZL114. |
| Heat treatment | T5/T6 in-house. |
| Mold materials | Mainly GB 45 carbon steel; H13 for more demanding requirements. |
| Design and simulation | UG and SolidWorks for mold design; AnyCasting for casting simulation. |
| Surface finishing | Mirror polishing is available. Specify the required surface and acceptance method in the RFQ. |
| Impregnation | Only with customer approval; performed by a qualified subcontractor. |
See gravity casting manufacturing scope, tilt-pour casting capabilities, and casting and CNC machining scope for process-specific review.
Tilt-pour range and tooling references
The tilt-pour figures below are capability references, not universal design limits. Values stated as “greater than” do not define an upper limit.
| Characteristic | Length or wall thickness (mm) | Mass (kg) | Condition |
|---|---|---|---|
| Mold longest edge | > 800 | Not applicable | Tilt-pour tooling reference. |
| Mass per pour | Not applicable | > 30 | Per pour; separate from finished casting mass. |
| Casting mass range | Not applicable | From < 0.2 to > 30 | Part suitability depends on geometry and requirements. |
| Largest casting longest edge | > 600 | Not applicable | Not a published maximum envelope. |
| Minimum wall thickness | About 3 mm typical; 2.5 mm over small areas near the gate | Not applicable | Tilt-pour reference; review the wall layout for each part. |
Send the complete part geometry so we can review which of these conditions can apply together to your design. Use the gravity casting design guide to prepare geometry and datum inputs.
| Item (unit where applicable) | Bohua reference | Condition |
|---|---|---|
| A356 permanent mold life (shots) | About 20,000–50,000 (GB 45 steel); about 100,000 (H13, with regular maintenance) | A356 permanent molds; review expected life for the individual tool and its operating conditions. |
| Drawing confirmation to first article (weeks) | 5–6 | Covers drawing confirmation to first article only; agree production-release and shipment dates separately. |
| As-cast tolerance grade | CT8 | As-cast condition; define drawing requirements separately. |
| Machined critical dimensional tolerance (mm) | ±0.02 | Applies to critical dimensions after machining only; identify the covered features and agree other tolerances separately. |
Quality system and inspection resources
Bohua's inspection resources support a project-specific acceptance plan. Specify the features, sampling, test conditions, and reports required before comparing quotations.
| Area (unit where applicable) | Bohua fact |
|---|---|
| Quality system | IATF 16949:2016, issued by NQA; valid through November 20, 2027. |
| PPAP submission level | Up to Level 5; agree the project submission requirements. |
| Chemistry and melt checks | Oxford optical emission spectrometer; vacuum hydrogen analyzer. |
| Radiography | Unicomp UNC-160 and Y.MU2000-D X-ray systems. |
| Dimensional inspection | Hexagon Global S and NANO Metrology CMMs; handheld 3D scanner. |
| Immersion test pressure (bar) | 3 or more; air-under-water immersion only. Define the pressure, hold time, test stage, and acceptance criteria for the part. |
| Mechanical testing | WDW-100E tensile testing machine; JB-300B impact testing machine; fatigue testing capability. |
| Corrosion and microstructure checks | YWX-750 salt spray chamber; metallographic microscope. |
| Hardness | HBE-3000A hardness tester; digital Brinell hardness tester. |
| Surface roughness | Mitutoyo SJ-410 roughness tester. |
Review quality certification information and quality control and inspection before requesting project records. The casting supplier evaluation checklist explains how to use the evidence for qualification.
Send a drawing package for the next decision
Send the drawing and acceptance requirements needed to test whether this capability matches your part. Include annual demand and tooling status so the scope can be compared consistently.
| Input | What to include |
|---|---|
| Geometry | Drawing revision, model, critical dimensions, datums, wall sections, and internal passages. |
| Material and operations | Alloy, temper, mechanical requirements, machining, and finishing scope. |
| Approval | Inspection zones, test conditions, acceptance criteria, required records, and approval owner. |
| Demand and delivery | Annual volume, sample quantity, release quantities, tooling ownership, target timing, packaging, and destination. |
For a fluid-path part, use the coolant water outlet manufacturing and RFQ guide. Send your requirements through the casting RFQ page or consult the engineering and buyer resources.
Send a drawing to check capability fit
Include material, annual volume, critical features, tooling status, and inspection requirements. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →