Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Gravity Die Casting Tooling Cost: What to Budget in 2026
Buyers often focus on piece price first and treat tooling as a one-time nuisance. That is a mistake. In gravity casting, tooling cost affects not only launch budget but also porosity risk, dimensional stability, cycle time, maintenance burden, and long-term unit cost.
On this page
- What to Budget in 2026
- What Is Included in Gravity Casting Tooling Cost?
- Bohua tooling facts
- Export-program tooling scope
- The 7 Biggest Cost Drivers
- Why Cheap Tooling Quotes Can Become Expensive
- Tooling Cost vs Piece Price: How Buyers Should Think
- Questions Buyers Should Ask Before Approving Tooling
- How Alloy and Part Function Influence Tooling Decisions
- Freeze the Critical-to-Quality Features
- Conclusion
What to Budget in 2026
Understand gravity die casting tooling cost: mold complexity, alloy, machining, volume thresholds & hidden quote assumptions.
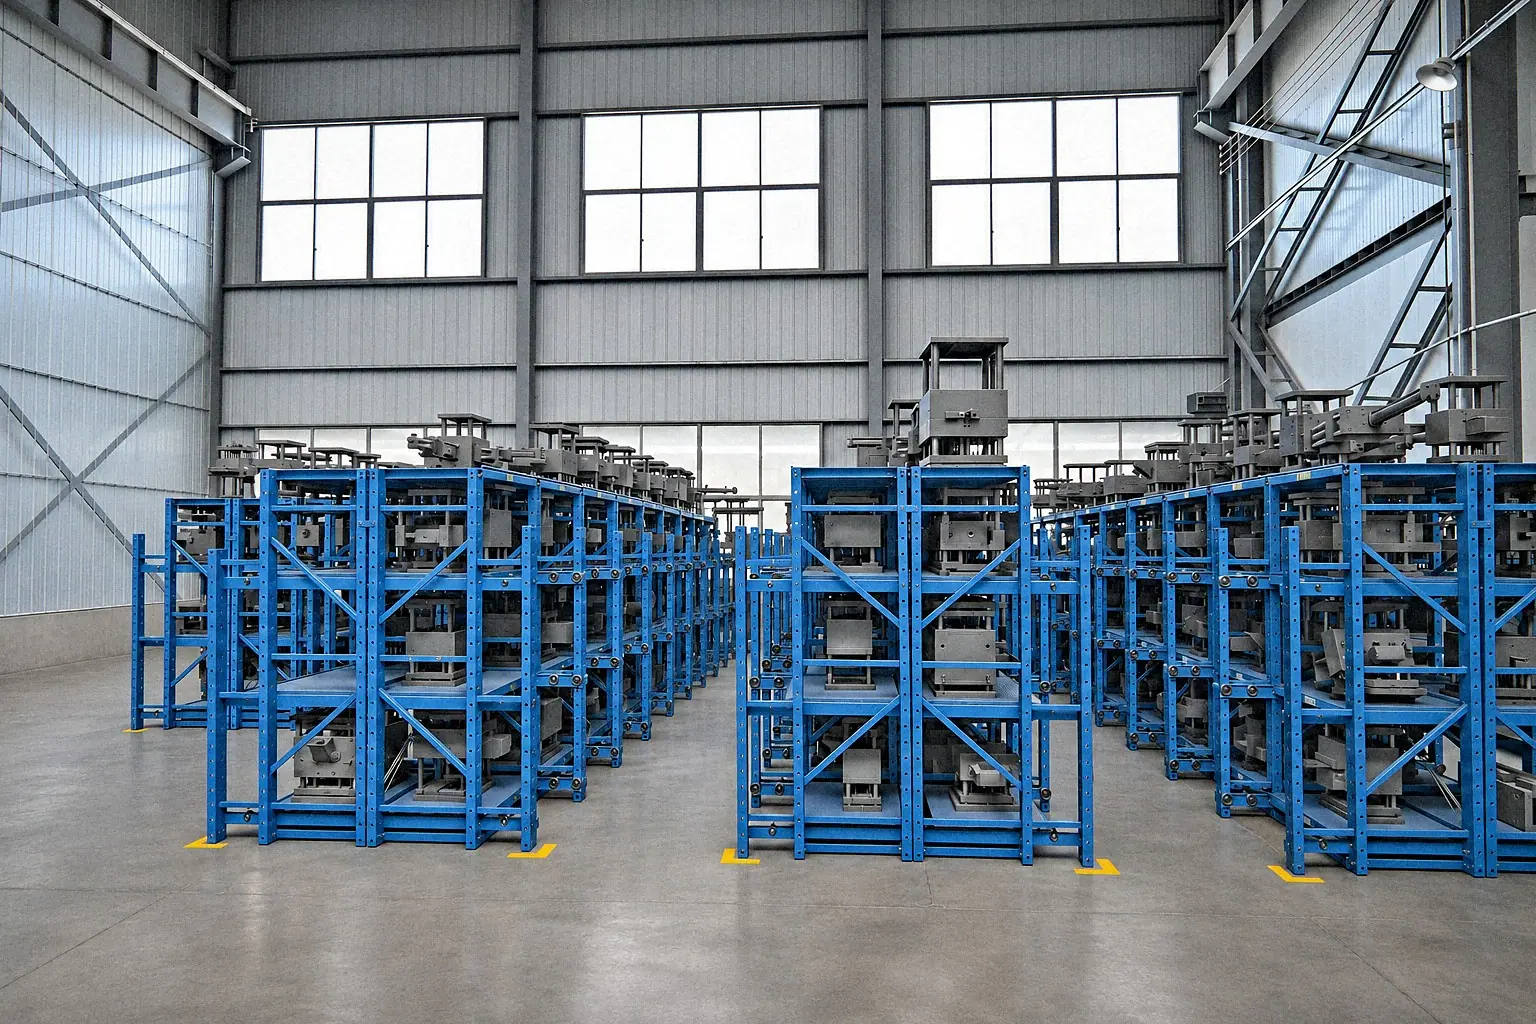
Tooling effort varies with geometry and required scope.
Evaluate tooling as a production asset: by total output quality over the life of the program, not by the lowest initial invoice.
What Is Included in Gravity Casting Tooling Cost?
When a supplier quotes gravity casting tooling, the price normally includes more than just two steel mold halves. The quotation should identify every tool and engineering activity required to reach an approved casting condition.
| Scope group | Items to identify | Buyer decision or evidence |
|---|---|---|
| Permanent mold | Mold body, inserts, parting line, gating, overflows, ejectors, chills, cooling | Steel grade, ownership, expected life, revision |
| Core system | Core boxes, sand cores, metal cores, seats, extraction mechanisms | Core method and replacement scope |
| Downstream tooling | Trim tools, machining fixtures, inspection fixtures, gauges | Included, optional, or buyer-supplied |
| Engineering | DFM, simulation, drawing release, process setup, sample correction | Deliverables and approval path |
| Lifecycle | Maintenance, storage, wear inserts, repairs, transfer terms | Responsible party and records |
Some suppliers quote only the metal mold and then add engineering changes, fixtures, gauges, or sample iteration later. That is why buyers should always ask for a tooling scope breakdown, not just a single lump-sum number.
Use the gravity casting DFM guide to define the drawing inputs that affect the tooling concept.
Bohua tooling facts
Bohua designs and manufactures its casting molds in-house, allowing the mold design, casting simulation, machining, assembly, and correction route to be reviewed against one controlled drawing package.
- Mold-shop equipment
- 17 machines
- A356 mold life
- About 20,000–50,000 shots (GB 45 steel); about 100,000 (H13, with regular maintenance)
- Drawing confirmation to first article
- 5–6 weeks
- Tilt-pour machines
- 32
- Vertical gravity machines
- 10
Tool design and materials
Most Bohua molds use GB 45 carbon steel. H13 is used for higher requirements. Tool design uses UG and SolidWorks, while casting simulation uses AnyCasting.
The stated A356 permanent-mold life is approximately 20,000–50,000 shots. That range applies to GB 45 carbon-steel molds; H13 molds last about 100,000 shots with regular maintenance. Actual life depends on part geometry, thermal loading, maintenance, inserts, operating conditions, and the agreed end-of-life criteria.
Bohua operates 32 tilt-pour machines, some designed and built in-house, plus 10 vertical gravity casting machines and 10 hot-box core shooters. This equipment context matters when the tool concept includes tilt filling, a vertical machine, or sand cores. See the Bohua gravity and permanent mold casting process for the production scope.
Export-program tooling scope
A realistic tooling scope depends on part size, geometry, core strategy, alloy, tolerance expectations, production volume, tool life, and validation risk. For large automotive parts with multiple slides, tight tolerances, and validation work, the cost can rise significantly. Final cost depends on geometry, quality target, and supplier scope.
For export programs, additional cost can come from:
- PPAP or APQP documentation
- extra sample rounds
- inspection fixtures
- CMM programming
- X-ray validation for internal quality
- special core design for hollow sections
The 7 Biggest Cost Drivers
1. Part Size and Weight
Bigger castings need larger mold bases, more machining time, more steel, larger handling equipment, and often slower sample-and-adjust cycles. The drawing should state the casting envelope, target weight, handling constraints, and machine concept used for the quotation.
A 1.2 kg housing and a 9 kg suspension component are simply not in the same tooling category.
Use these illustrative weights to compare tooling categories. For your project and machine-fit review, provide the actual casting weight and envelope.
At Bohua
For a tilt-pour tooling-fit review, Bohua can accommodate molds extending beyond 800 mm along their longest side. A tilt-pour charge can exceed 30 kg, while the casting-weight scope runs from below 0.2 kg to above 30 kg. The reported largest casting envelope exceeds 600 mm along its longest side. The mold envelope, poured charge and finished casting weight are separate inputs to the tooling review.
2. Geometry Complexity
Deep pockets, undercuts, thin-to-thick transitions, sealing faces, and complex flange intersections all increase tooling difficulty. Complexity affects not just machining hours but also how much engineering time is needed to achieve stable fill and feeding.
3. Core Strategy
If the casting can be made with a simple permanent mold, tooling cost stays relatively controlled. If the part needs multiple sand cores, metal cores, side cores, or special extraction logic, tooling price rises. Core-related complexity also increases maintenance cost during serial production.
4. Alloy and Quality Target
A356 and ZL114 gravity castings for structural or heat-treated automotive use usually require tighter process control than cosmetic-only industrial parts. If the tool must support low porosity, heat treatment stability, and reliable machining stock, engineering effort goes up.
5. Tolerance Requirement
A tool for a general industrial cover is different from a tool expected to repeatedly support tight datums before CNC finish machining. If the buyer wants aggressive tolerances, critical locating features, or stable wall thickness in several functional zones, correction work after first samples becomes more extensive.
For context, if you have not defined tolerance expectations yet, our guide on ISO 8062 tolerance guide is worth reviewing before RFQ.
Define which dimensions are cast and which are machined. We specify as-cast CT8 separately from critical machined dimensions of ±0.02 mm. Mark your required tolerances by feature so we can review the casting and machining scope.
6. Expected Tool Life and Annual Volume
A tool designed for 3,000 pieces and a tool designed for 80,000 pieces should not be engineered identically.
Use these illustrative quantities to compare intended tool lives. Confirm order quantities and process selection separately for your project.
Expected life should be stated together with annual volume, lifetime volume, release pattern, maintenance, and end-of-life criteria. Higher annual volume may justify higher-grade tool steel, replaceable inserts in wear zones, better thermal balance features, faster cycle design, and more preventive-maintenance access. This increases initial tooling cost but often reduces unit cost over the full program life.
7. Validation and Rework Risk
If a supplier skips simulation, first-article sectioning, or proper correction loops, they can quote a lower upfront number. The hidden cost appears later in delayed SOP, repeated dimension drift, or porosity found after machining.
Why Cheap Tooling Quotes Can Become Expensive
A cheap tool that needs constant welding repair or produces unstable filling is not cheap at all. A very low tooling quote usually requires a closer review of what is included, excluded, or shifted to later approval. Ask each supplier to explain the technical assumptions behind a lower quotation so you can compare its scope.
- limited engineering review before machining the mold
- minimal allowance for correction after first samples
- lower-grade steel or weak insert design
- poor gating design discipline
- no serious dimensional validation plan
- key production risks shifted back to the buyer later
Review these potential consequences:
- more sample rounds
- delayed project timing
- scrap during ramp-up
- unstable machining allowance
- tool repair charges after launch
- poor casting yield driving up future unit price
This is the same reason a professional RFQ package matters. If your inputs are vague, the tooling quote will either be padded or unrealistically optimistic. Our aluminum-casting-rfq-checklist shows what buyers should send before asking for price.
Tooling Cost vs Piece Price: How Buyers Should Think
Gravity casting is not usually chosen because the tool is the cheapest. It is chosen because it creates a good balance between tooling investment and part integrity.
Request itemized supplier scope when a comparison uses generic low, medium, or high cost labels. Compare one-time tooling separately, then evaluate recurring casting, cores, heat treatment, machining, inspection, finishing, packaging, and logistics at the same annual-volume and release assumptions. If the manufacturing route is still open, use the casting process selection guide before commercial comparison.
If annual volume is moderate and the part needs stronger mechanical performance than typical die-cast ADC12, gravity casting often makes economic sense. That is especially true for A356-T6 or ZL114 programs where internal quality matters.
No payback figure is published here
This page does not publish a payback figure. Ask for quoted tooling and measured scrap before comparing programs.
Label the payback scenario as your buyer model and obtain supplier quotations for its cost inputs. Keep all assumptions visible and use measured scrap and downtime with quoted unit-price figures when available.
The quantities above are hypothetical. Replace them with your project quantities and validate the payback calculation before using it for an order decision.
Compare option A with option B, a candidate tool with better filling balance and replaceable inserts. Use the same delivered-part scope and acceptance criteria.
If option B reduces scrap, improves cycle consistency, and avoids launch delays, it may produce a lower true cost per delivered good part over the life of the program.
For 60,000 parts total, even a small difference in scrap, rework, and downtime can outweigh the initial tooling gap very quickly.
Whether that happens depends on quoted tooling amounts and measured scrap, rework, downtime, and delivered good-part quantities.
You can also compare this against our process article gravity-casting-vs-die-casting if your team is still deciding between manufacturing routes.
Questions Buyers Should Ask Before Approving Tooling
Use these questions during quotation review:
- What exactly is included in tooling price?
- Is solidification or mold-flow analysis included?
- What core method is assumed?
- Which dimensions are controlled by casting, and which by machining?
- What alloy is the tool designed around: A356, ZL114, or another grade?
- What tool life is the quote based on?
- Are inserts replaceable in high-wear areas?
- What happens if first samples need dimensional correction?
- Who owns the tooling and how is maintenance handled?
A serious supplier should answer these directly. If the answer is vague, expect scope creep later.
How Alloy and Part Function Influence Tooling Decisions
For structural automotive components, tooling cannot be separated from final performance requirements. A pressure-related housing needs gating, feeding, machining stock, and inspection planning that follow the drawing's sealing surfaces and acceptance criteria.
- A356-T6 programs often require controlled wall thickness, low porosity, and stable heat-treatment response.
- ZL114 gravity cast parts may need stronger feeding design because of section sensitivity in load-bearing geometry.
- Pressure-related housings need careful gating and machining stock planning to avoid leak paths after finishing.
Material selection belongs in the drawing and RFQ. The A356 casting specification guide explains how to state alloy, temper, test basis, and required evidence without relying on a generic material label.
Freeze the Critical-to-Quality Features
Do not treat every dimension equally. Identify sealing faces, bearing bores, mounting datums, wall-thickness-sensitive zones, and machining reference surfaces.
Align the Tool Design With the Real Production Route
If the final part will be heat treated, leak tested, and CNC machined, the tooling review should reflect that from day one.
At Bohua
Bohua can check tooling-related dimensional features with Hexagon Global S and NANO Metrology CMMs. Its internal-inspection resources include Unicomp UNC-160 and Y.MU2000-D X-ray systems. For pressure-tight parts, the confirmed Bohua method is air-under-water immersion at 3 bar or more.
| Requirement | Resource to scope | Input needed for the quotation |
|---|---|---|
| Dimensions | CMM inspection | Datums, cast versus machined features and report stage |
| Internal soundness | X-ray inspection | Zones, applicable standard edition, sampling and acceptance |
| Pressure boundary | Immersion test and fixture | Cavity map, test pressure, hold and observation times, and bubble criterion |
Use the immersion-test specification to define the fixture and test scope before comparing tooling quotations.
Budget for Engineering, Not Only Steel
They are well engineered. Simulation, sample feedback, section checks, and dimensional correction should be assigned in the quotation scope.
- Freeze references. Confirm the 2D drawing, 3D model, revision, alloy, and temper.
- Mark functional features. Identify datums, sealing surfaces, critical dimensions, cores, and machined stock.
- Define evidence. State dimensional, material, internal-quality, leak-test, and approval records.
- Define lifecycle terms. Record ownership, maintenance, storage, changes, expected life, and transfer terms.
- Separate commercial scope. Keep mold, core boxes, fixtures, gauges, samples, and recurring operations visible.
Conclusion
Gravity casting tooling cost is important, but tooling value is what buyers should really evaluate. A realistic permanent mold budget depends on part size, geometry, core strategy, alloy, quality target, and production volume. Do not select a tool on the lowest quote alone. It is the tool that supports stable production, acceptable scrap, predictable machining, and on-time launch.
Send the controlled package through the casting drawing request form when you need a tooling scope tied to the actual part.
Request a gravity casting tooling review
Send the drawing, annual volume, alloy, critical features, core concept, machining scope, and required approval evidence. Submit the RFQ details, then email your drawing for a structured quote review. Send the drawing, target alloy, finishing scope, MOQ, and delivery timing. Bohua will review it like a real sourcing project, not a generic contact request. Our engineering team can recommend the right alloy, process, and design optimizations for your specific requirements.
Send your drawing →