Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
RFQ
Pump casing RFQ guide for leak-test criteria, CNC machining datums, and pressure-tight quote packages
Use this page when a pump casing quote depends on pressure-tightness criteria, sealing-face machining, CNC datums, tooling status, and inspection records. A comparable RFQ identifies the tested boundary, pressure, duration, acceptance rule, supplied condition, annual volume, and documentation before suppliers price the work.
What Makes a Pump Casing RFQ Quoteable?
A quoteable package defines the pressure boundary, test acceptance, finished interfaces, tooling condition, inspection records, and commercial volume. Send the casting weight together with machining, testing, fixture, and documentation requirements so suppliers can quote the same scope.
- Bohua immersion capability
- 3 bar or more
- Critical machined dimensions
- ±0.02 mm capability
- Vertical machining centers
- 16
- PPAP support
- Up to Level 5
- New-tool first samples
- 5–6 weeks from drawing confirmation to first article
The pump casing image on this page shows a part Bohua has made. For your project, include the required alloy, process, dimensions, pressure rating, tolerance, and test acceptance criteria with the controlled drawing.
Use the pump housing manufacturing capability page when the main question is supplier fit. Use this page when the drawing exists and the main task is defining one comparable pressure-tight quote package.
Minimum Inputs for the First Quote
Send one controlled package that engineering, procurement, and quality can review together. Open decisions may remain, but they should be listed as quote assumptions rather than left hidden.
| Input group | Information to send | What it controls |
|---|---|---|
| Geometry | Revision-controlled 2D drawing and STEP model | Casting, tooling, machining, fixture, and inspection review |
| Function | Fluid or gas, service conditions, pressure boundary, and sealing map | Process and pressure-tightness risk review |
| Material | Alloy, temper, governing specification, and certificate requirement | Material, heat treatment, and verification scope |
| Delivery condition | As-cast, heat-treated, machined, coated, cleaned, or ready for assembly | Final acceptance state and included operations |
| Test requirement | Method, pressure, duration, acceptance, stage, sampling, and record | Fixture, cycle, capacity, and documentation scope |
| Quantities | Sample needs, annual volume, release pattern, and destination | Tooling, production, packaging, and logistics assumptions |
The casting drawing requirements explain how to organize revision, datum, tolerance, and model information. If the process is still open, use the casting process selection guide before fixing the quote route.
Define Pressure-Tightness Acceptance
Turn “leak test required” into a test specification with measurable acceptance criteria. The RFQ must identify what is pressurized, how it is closed, the test condition, what counts as a failure, and which records the buyer expects.
- Mark the boundary. Identify each cavity, gasket face, O-ring groove, port, plug, cover, and temporary closure that forms the tested volume.
- Name the supplied state. State whether the requirement applies before machining, after final machining, after coating, or after assembly.
- State the pressure. Give the value and unit and explain whether it is an inspection, operating, or proof condition.
- Set the duration and acceptance. Define the test period, stabilization rule if applicable, visible-leak rule or other buyer criterion, and disposition for a failure.
- Set frequency and records. Define sampling, traceability, report fields, retention, and approval authority.
- Declare the impregnation rule. State whether impregnation is prohibited or may be considered with customer approval and disclosure.
Confirmed Bohua boundary
Bohua's pressure-tightness method is air-under-water immersion at 3 bar or more. A buyer requirement outside that method or range must be reviewed before quotation. Impregnation is performed by a qualified subcontractor only with customer approval.
The leak-tight aluminum casting page separates casting, machining, testing, and impregnation responsibilities. Keep component testing, complete-pump performance, and regulatory validation as separate requirements, with the responsibility for each stated in your RFQ.
Mark Every Sealing Interface
Flatness and surface requirements must be tied to a named interface and process stage. Tell each supplier whether the cover face is supplied as cast or includes final machining and measurement so the quotations cover the same work.
- Gasket and cover faces: identify the full face or local sealing zone and the stage at which flatness is accepted.
- O-ring features: mark grooves, lands, intersections, and any surface treatment exclusion.
- Ports and plugs: define thread standards, classes, depths, sealing method, gauges, and closure ownership.
- Bolt and dowel patterns: define position tolerances, spotfaces, locating features, and their datum references.
- Surface texture: state Ra or Rz only where the drawing requires it, with the measurement location and report method.
Specify the flatness and surface values required for your pump casing and its mating components. The gasket system, face geometry, clamping design, coating, and final assembly determine the requirement for the controlled drawing.
Define CNC Datums and Functional Bores
Machining and inspection should use an explicit datum strategy. Bearing seats, seal bores, locating pilots, ports, and gasket faces need tolerances and relationships that name the measured feature and its reference.
| Feature | Required RFQ detail | Record decision |
|---|---|---|
| Datum frame | Primary, secondary, and tertiary datums for machining and inspection | Fixture reference and CMM setup |
| Bearing or seal bore | Diameter, geometry, runout or position requirement, and reference datum | CMM, gauge, or buyer-specified method |
| Ports and threads | Machining list, standard, class, depth, and gauge | Characteristics and report frequency |
| Sealing face | Flatness, surface texture, local zones, and final process stage | Measurement method and sample locations |
| Machining stock | Drawing allowance or supplier proposal | Assumption written into the quote |
At Bohua
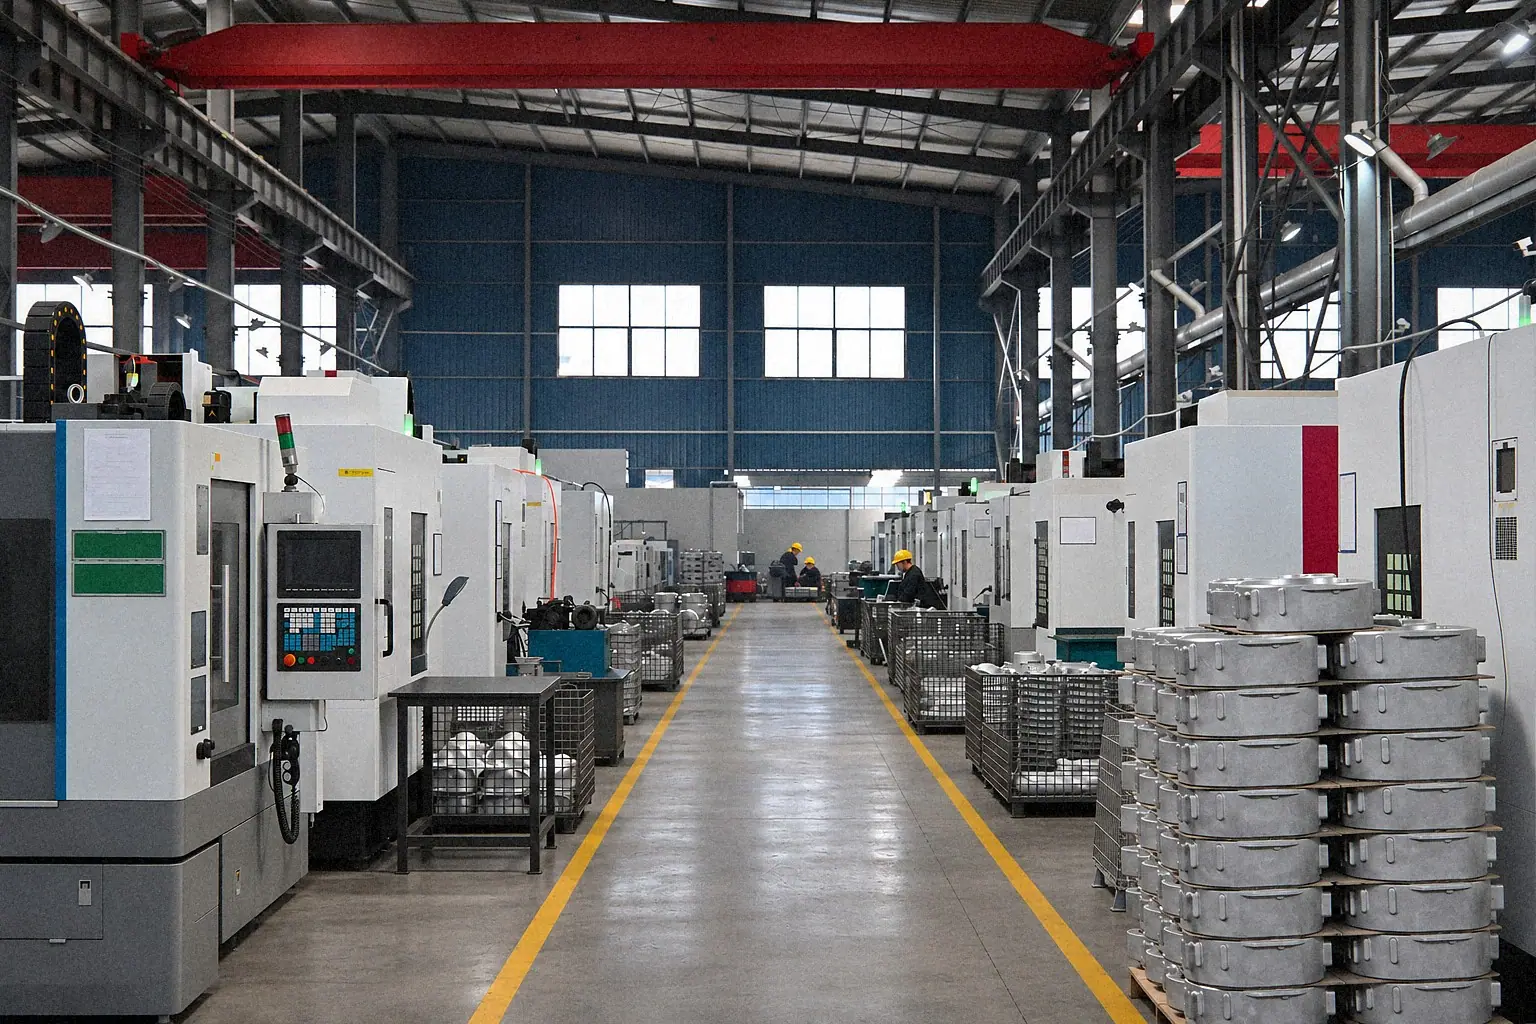
Machining equipment includes 16 vertical machining centers, 2 CNC engraving and milling machines, 22 CNC lathes, and 2 large lathes. Bohua's confirmed general capability is CT8 in the as-cast condition and ±0.02 mm for critical machined dimensions. These are separate capabilities; the drawing review decides whether a specific feature is feasible and how it will be measured.
Review the casting and CNC machining scope before assigning the fixture, final acceptance state, and dimensional record.

State Whether Tooling Is New, Modified, or Transferred
Tooling status changes what a supplier must inspect and quote. A new mold requires design and build scope; a transferred mold requires condition, ownership, interface, and sample-history information before it can be treated as production-ready.
- New tooling: include drawing release status, expected ownership, sample approval path, and correction responsibility.
- Transferred tooling: include current location, mold material if known, maintenance and change history, sample parts, inspection records, and available fixtures.
- Modified tooling: identify the controlled geometry change, affected inserts or cores, and the revalidation scope.
- Machining fixtures: state whether fixtures transfer with the mold or must be designed and validated again.
At Bohua
Bohua designs and makes molds in-house. Most tooling uses GB 45 carbon steel, with H13 for higher requirements. A356 permanent molds typically last about 20,000–50,000 shots. That range applies to GB 45 carbon-steel molds; H13 molds last about 100,000 shots with regular maintenance. From drawing confirmation, first article takes 5–6 weeks.
For an existing mold, use the existing-tool transfer checklist to separate known evidence from assumptions.
Choose the Inspection Record Pack
List the records needed for approval and ongoing supply before the quote is issued. Specify the characteristics, inspection frequency and acceptance criteria for each requested report. Ask us to confirm the included checks and records in the quotation.
| Checkpoint | Bohua capability | Buyer must define |
|---|---|---|
| Material identity | Oxford optical emission spectrometer | Alloy, temper, governing specification, and certificate format |
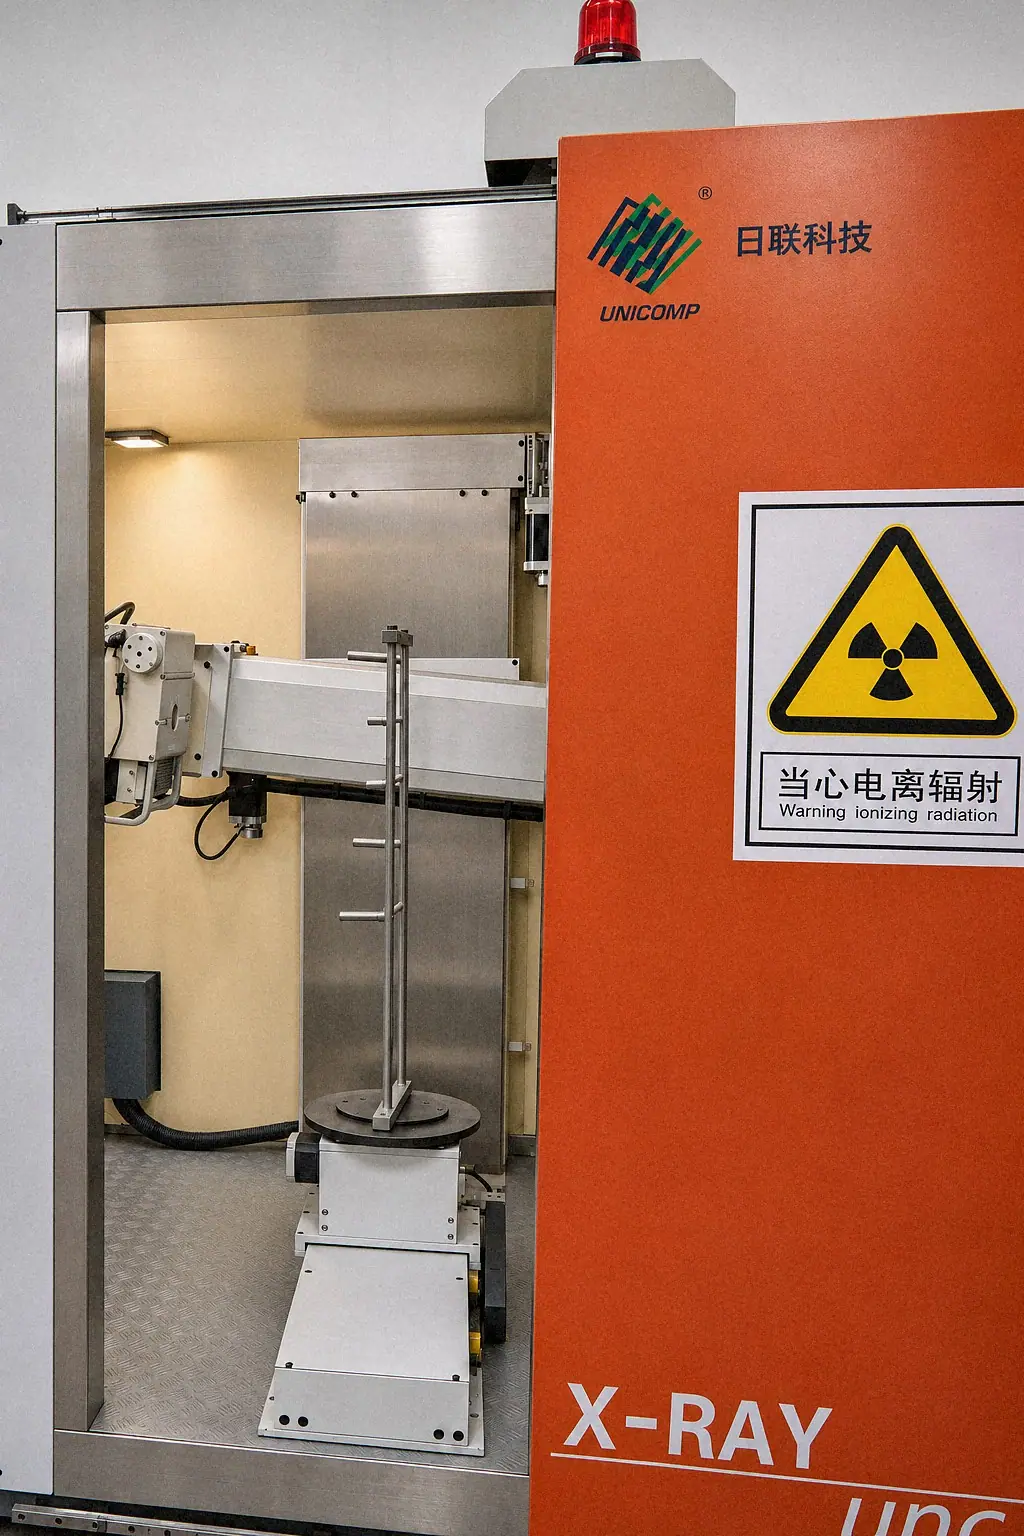
| Internal inspection | Unicomp UNC-160 and Y.MU2000-D X-ray systems | Zones, views, frequency, acceptance reference, and record format |
| Dimensions | Hexagon Global S and NANO Metrology CMM systems | Datums, characteristics, sampling, and report layout |
| Pressure tightness | Air-under-water immersion at 3 bar or more | Boundary, pressure, duration, acceptance, stage, sampling, and record |
| Submission package | PPAP support up to Level 5 | Level, deliverables, timing, and approval authority |
Bohua's quality management system is certified to IATF 16949:2016 by NQA, with the certificate valid through November 20, 2027. Review the wider quality-control and inspection capability when selecting the project record pack.
What to Add When Replacing an Existing Supply Source
Send the available failure evidence with the RFQ so the replacement supplier can distinguish known requirements from unresolved causes.
- Mark the leak or assembly-failure location and the manufacturing stage when it first appeared.
- Include available test settings, failed-sample photographs, dimensional results, and section or internal-inspection records.
- Identify unknown causes and who approves changes to the design, process, repair, or reinspection plan.
For feature-specific preparation, use the pump housing engineering and inspection guide. It covers volutes, wear rings, core position, vacuum interfaces, and the evidence each question needs.
Make Supplier Quotes Comparable
Ask every supplier to list inclusions, exclusions, assumptions, and buyer-owned work in the same order. A lower total may reflect a missing fixture, test, record, or finishing operation rather than a lower cost for the same scope.
| Scope line | Comparison question |
|---|---|
| Tooling | Does the quote include mold design, build, correction, ownership, and maintenance assumptions? |
| Casting and heat treatment | Are alloy, temper, process route, and material evidence stated? |
| CNC machining | Are fixtures, datums, bores, ports, threads, sealing faces, and final cleaning included? |
| Pressure-tightness test | Are boundary, method, pressure, duration, acceptance, frequency, fixture, and records included? |
| Inspection | Are dimensional, material, internal-inspection, PPAP, and traceability deliverables listed? |
| Finishing and shipment | Are coating, protection, packaging, destination, and delivery terms visible? |
Submit the Pump Casing RFQ
After you submit the form, email the controlled drawing package to Linda at linda@ningbobohua.com. Enter the annual volume, delivery condition, tooling status, pressure-tightness criteria, machining scope, required records, destination, and contact details on the form. If important fields remain open, list them as supplier-review questions instead of allowing silent assumptions.
Use the aluminum casting RFQ checklist for a final package review.
Tell us about your part
Only your email address and requirement description are required.
Linda, Export Sales · linda@ningbobohua.com
You can also send your inquiry by email. Include your email address and requirement description, including what the part must do. Add your name, company, material, quantity, annual volume and preferred process if available.
Send drawings by email, or ask about an NDA before sharing drawings.
Pump Casing RFQ Questions
Define the supplied component, test boundary, and required evidence before comparing quotations.
Is “leak test required” enough for a quotation?
No. Define the tested boundary, supplied state, method, pressure with units, duration, acceptance rule, sampling, fixture responsibility, and record format.
Should the RFQ include both casting and CNC scope?
Yes when Bohua is expected to supply the machined casing. The quote should identify datums, fixtures, sealing faces, bores, ports, threads, grooves, surface requirements, cleaning, and the final acceptance state.
What if the buyer requires a test outside Bohua's confirmed immersion method?
State the required method and acceptance criteria in the RFQ. We will review the required method and acceptance criteria before quotation to confirm whether we can meet them for your project.
Can impregnation be assumed in the price?
No. At Bohua, impregnation requires customer approval and is performed by a qualified subcontractor. The RFQ should state whether it is prohibited or may be considered with approval, disclosure, and any required re-test.
Can a pressure-tightness test replace dimensional inspection?
No. A pressure-tightness result addresses the defined boundary under the defined test. Specify separate dimensional checks for gasket-face flatness, bore alignment, port position, thread condition, runout, and other drawing characteristics, with the required records.