Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Aluminum Gravity Casting for Heat Sinks: Alloy & Fin Tips
Aluminum gravity casting can be considered for heat sinks with three-dimensional fins and integrated mounting features. The drawing must allow reliable filling, mold release and contact-face machining. Bohua’s casting and CNC resources support a manufacturing review; the buyer’s thermal targets, operating conditions and agreed validation plan determine whether the finished heat sink is acceptable.
On this page
Aluminum gravity casting is worth evaluating for a heat sink that combines three-dimensional fins, a substantial base and integrated mounting features. Process selection still depends on fin filling, mold release and machining access. Thermal performance must be validated for the specified alloy condition, contact interface and cooling environment.
When a cast heat sink is worth reviewing
Choose the manufacturing route around the heat path and geometry, then compare the complete delivered part.
| Application context | Features to identify | Evidence to define |
|---|---|---|
| LED fixture or lighting housing | Radial fins, mounting pad, lens or reflector mounts | Heat-source location, orientation, outdoor exposure and contact-surface requirements |
| Power electronics or inverter housing | Local contact pads, mounting bosses, connector openings | Heat dissipation, airflow, electrical isolation and final assembly constraints |
| Telecom or industrial controller | Fin field, enclosure walls, fasteners and installation space | Ambient temperature, blocked-airflow conditions and mounting orientation |
A continuous profile may favor an extrusion-based design. A cast design needs its own review of parting, draft and feature access. The casting process selection guide covers the broader comparison; no universal annual-volume threshold selects the route.
A reference photograph can explain a fin pattern or mounting arrangement. For your heat sink, send the alloy condition, thermal-resistance target and acceptance requirements with the drawing.
Define the thermal target and its test conditions
Send the operating conditions with the drawing so the thermal target has a clear meaning.
| Input | Unit or reporting basis | Required condition |
|---|---|---|
| Heat dissipation | W | Continuous and peak load, duty cycle and heat-source location |
| Temperature limits | °C | Ambient, contact-surface or junction limit; identify the measurement point |
| Thermal resistance, if specified | K/W | Define both temperature locations, heat flow and test arrangement |
| Airflow, if forced convection | m³/s or m/s | State whether the value is flow rate or local velocity, plus direction and restrictions |
| Contact interface | Area in mm²; dimensions in mm | Mating part, thermal interface material, clamping method and orientation |
Assign thermal simulation and validation responsibilities before tool release. Use material certificates, CMM reports and casting simulation for their material, dimensional and manufacturing checks. Specify a separate thermal-performance validation for the assembled heat sink. If simulation files are confidential, share permitted boundary conditions and acceptance targets under the agreed disclosure arrangements.
Review fins together with the base and tooling
Fin thickness alone is not a sufficient casting-feasibility rule. Review fin height, gaps, root transitions, fill distance and mold release together.
- Mark fin thickness, height, gap, root radius and base thickness in mm on the controlled drawing.
- Identify functional fin-fill zones, allowable edge damage and cosmetic surfaces.
- Show bosses, threads, inserts and tool access. Define whether inserts are installed after casting or require a separately qualified route.
- Mark proposed parting, draft and machining stock for review. Treat undercuts as tooling decisions, not automatic casting features.
At Bohua
Bohua has 32 tilt-pour casting machines and 10 upright gravity casting machines. Its tilt-pour walls are typically about 3 mm, and small areas near the gate can go down to 2.5 mm. Use this general range as a starting point, then send fin height, spacing and fill distance so we can review the thickness for your heat sink.
Bohua designs and makes its molds in-house. Tool design uses UG and SolidWorks; casting simulation uses AnyCasting. Casting simulation supports manufacturing review. Assign any required CFD and thermal-performance validation separately in your project plan.
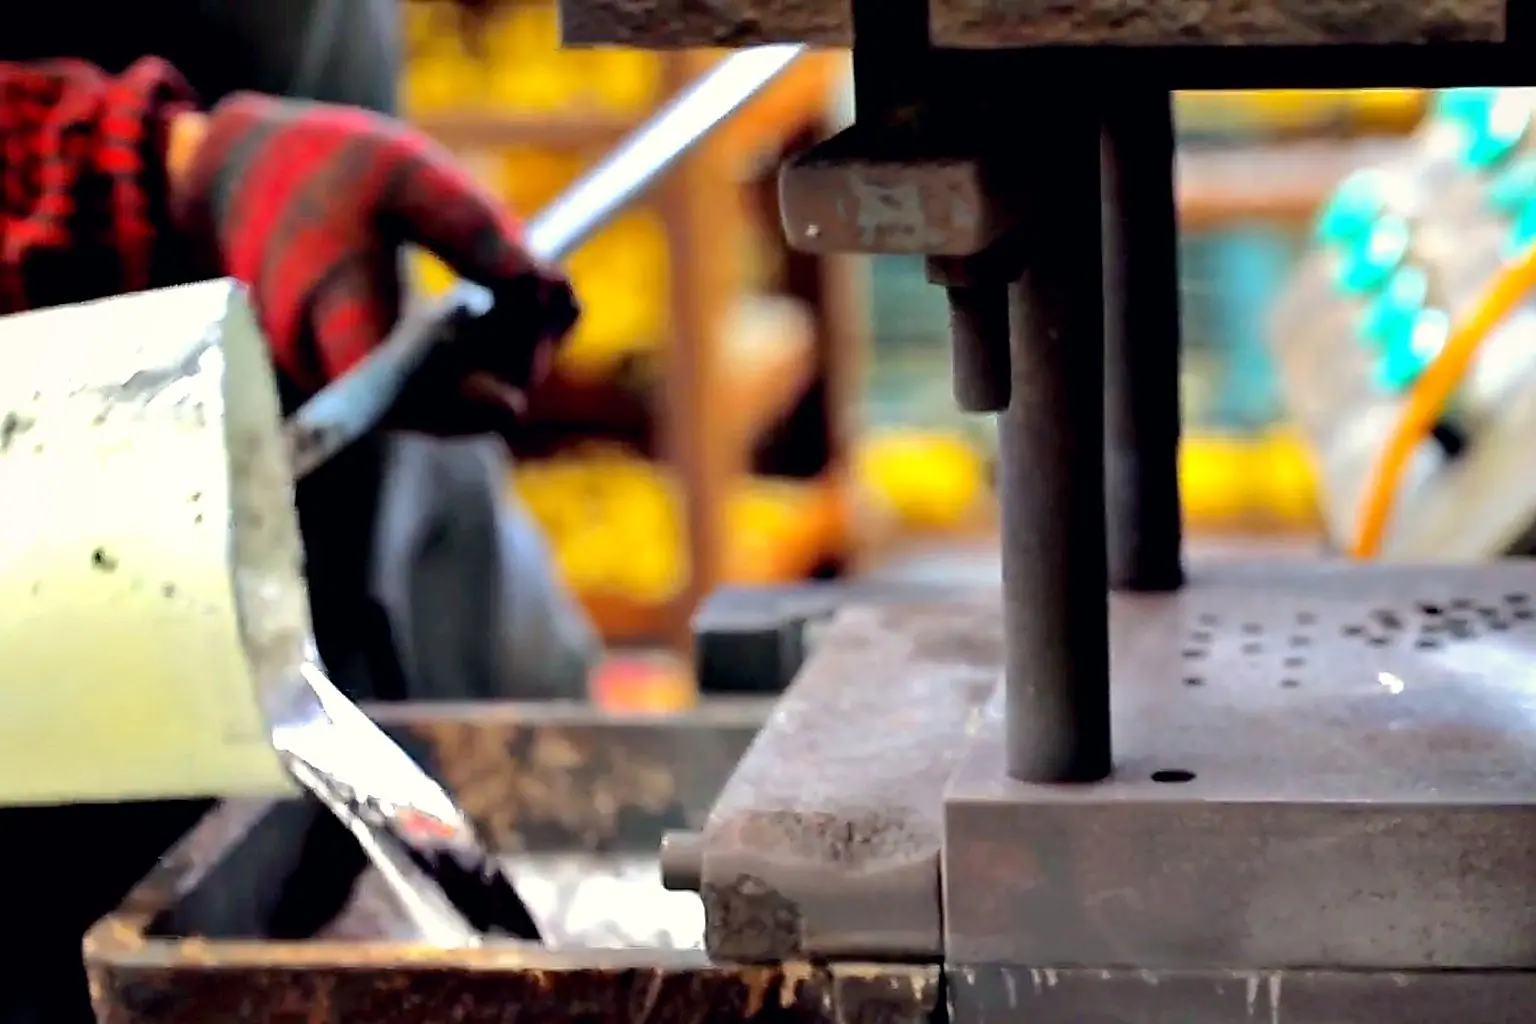
Check the tilt-pour manufacturing range before assuming that a thin or deep fin field fits the process.
At Bohua
Bohua monitors melt temperature continuously with a furnace-mounted probe protected by a silicon carbide tube made to suit the furnace.
Quality inspectors use an infrared thermometer for spot checks of mold-core and mold-wall temperatures.
Review the fin layout and filling distance with the tooling proposal; agree temperatures for the particular part rather than adopting a common setting for every heat sink.
Specify the alloy and delivered condition
Specify the alloy and temper together, using the material requirement and edition on the drawing. Use handbook conductivity for initial material comparison, then validate heat-sink performance under the specified operating conditions.
At Bohua
Bohua uses A356 and ZL114 for gravity and tilt-pour casting. T5/T6 heat treatment is performed in-house.
For an A356 casting specification, define chemistry, required mechanical properties, specimen basis and any thermal-property evidence. Select heat treatment for the approved requirements; do not assume every heat sink requires T6. The alloy, temper, temperature and measurement method must accompany any proposed conductivity value.
Control the contact face and final inspection state
Define each functional contact face, its machining scope and the state in which it will be accepted.
| Feature | Unit or designation | Acceptance input |
|---|---|---|
| Base or local pad flatness | mm | Controlled area, support condition and before/after-coating state |
| Surface texture | Ra in µm, if specified | Measurement method, evaluation conditions and functional surface |
| Mounting holes and datums | mm; drawing-defined geometrical controls | Datum scheme, hole positions, threads and inspection access |
| Coating or finish | µm if thickness is specified | Masking, contact zones, corrosion or insulation purpose and acceptance method |
Separate cast surfaces from machined and coated surfaces. Do not assume all fins need machining or that a general dimensional tolerance establishes base flatness. Protect contact faces and fin edges during packaging.
At Bohua
Bohua has 16 vertical machining centers. Dimensional inspection equipment includes Hexagon Global S and NANO Metrology CMMs. A Mitutoyo SJ-410 roughness tester is available for surface-texture checks.
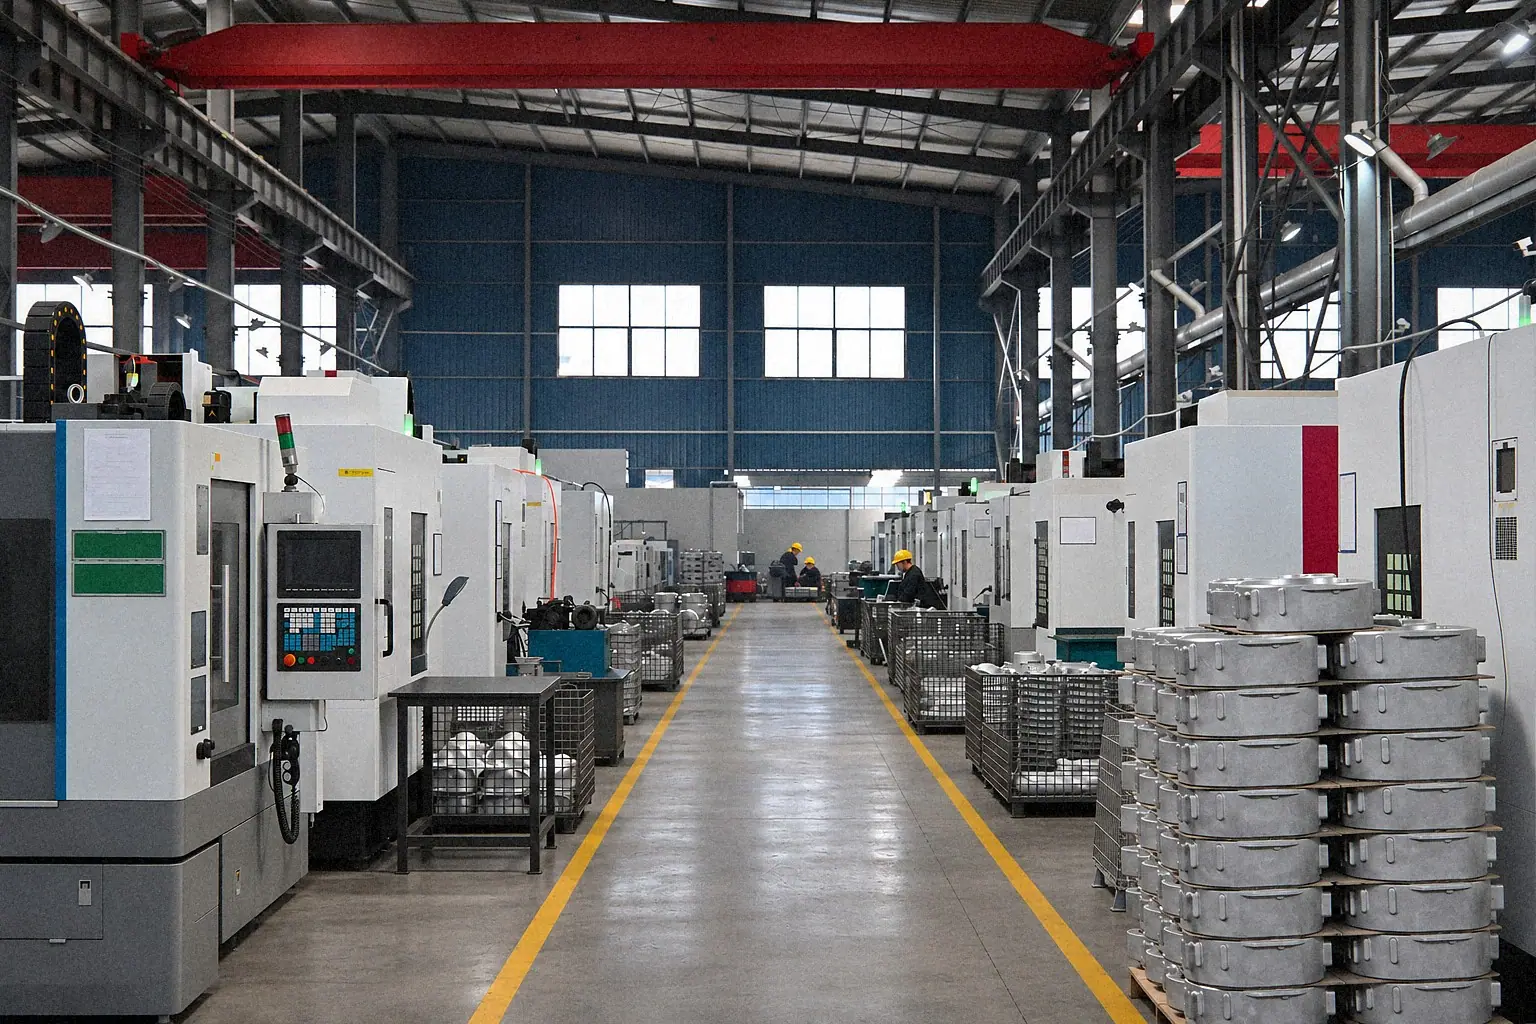
Use the casting and CNC machining scope to identify datums and required operations. Read the surface-texture specification guide when defining contact-face roughness.
At Bohua
Bohua’s dimensional scope separates routine CT8 as-cast dimensions from key machined dimensions that can reach ±0.02 mm.
For the heat-sink contact face, state flatness and measured surface texture separately from size tolerance, then define the condition used for the thermal validation.
Send a heat-sink RFQ with a defined validation owner
A comparable quotation separates manufacturing evidence from thermal validation.
- Controlled 2D PDF and STEP model, revision, heat-source location and cooling conditions.
- Alloy and temper requirements, allowable substitutions and approval responsibility.
- Fin geometry, fill-risk zones, contact faces, datums, holes, inserts and required finish.
- Required material and heat-treatment records, fin-fill acceptance, flatness report and mounting-feature inspection.
- Thermal-test or simulation scope, validation owner and sample acceptance sequence.
- Sample and annual quantities, tool status and ownership, launch milestones, destination, delivery terms and packaging needs.
Request separate scope for tooling, casting, heat treatment when specified, CNC machining, finishing, inspection and packaging. Send that package through the heat-sink drawing and RFQ submission. Include the heat-output and thermal-resistance targets, test conditions and validation owner so manufacturing review and thermal acceptance have clear responsibilities.
Send your heat-sink drawing and thermal inputs
Submit the RFQ details, then email your drawing for a structured quote review. Not sure which process fits? Tell us what the part must do. In a free drawing review, our engineers recommend a process and suggest design changes where needed.
Send your drawing →