Ningbo Bohua Mechanical Parts Co., Ltd. · Linda, Export Sales · linda@ningbobohua.com · www.bohua-casting.com
Engineering guide
Aluminum Casting Defects: 9 Causes & Solutions
Common aluminum casting defects include gas porosity, shrinkage, cold shuts, incomplete fill, hot tears, oxide inclusions, heat-treatment blistering, surface damage and dimensional variation. Begin with the observed symptom and manufacturing stage, then verify the cause. A pore, crack or leak does not by itself identify which process condition failed.
On this page
- Introduction
- Start Here: Match the Symptom to the Next Check
- Why Casting Defects Matter for Buyers
- 1. Gas Porosity
- 2. Shrinkage Porosity
- 3. Cold Shuts (Cold Laps)
- 4. Misruns (Incomplete Fill)
- 5. Hot Tears (Hot Cracking)
- 6. Oxide Inclusions
- 7. Heat-Treatment Blistering
- 8. Surface-Condition Defects
- 9. Dimensional Variation
- Verification Matrix: Match the Method to the Risk
- Bohua equipment and inspection boundaries
- Questions to Ask Your Casting Supplier
- Buyer Evidence Checklist
- Buyer questions
- Record One Problem Before Choosing a Corrective Action
- Technical References and Scope
Introduction
Common aluminum casting defects include gas porosity, shrinkage, cold shuts, incomplete fill, hot tears, oxide inclusions, heat-treatment blistering, surface damage and dimensional variation. Begin with the observed symptom and manufacturing stage, then verify the cause. A pore, crack or leak does not by itself identify which process condition failed.
This guide covers nine recurring defect categories in gravity casting and die casting. The tables below are a troubleshooting reference; acceptance depends on the drawing, function and agreed inspection procedure. For an actual part review, record the location, lot and test conditions before changing the process.
Start Here: Match the Symptom to the Next Check
Use this table to choose what to investigate. More than one mechanism can produce a similar appearance.
| Observed symptom | Possible mechanism | Next evidence to collect |
|---|---|---|
| Rounded pores exposed by machining | Gas-related porosity; mixed mechanisms remain possible | Location and depth, casting route, melt-treatment records and internal or section examination |
| Irregular cavities near a heavy section | Feeding or solidification shrinkage | Section geometry, feeding arrangement and the distribution of internal indications |
| A seam where metal fronts meet | Cold shut or an oxide-associated discontinuity | Fill path, location, surface examination and a suitable confirmatory inspection |
| Missing edges or incomplete thin sections | Incomplete fill | Actual fill conditions, venting, metal quantity and repeated location across parts |
| Crack near a restrained junction | Hot tear or a later handling/thermal crack | When the crack first appears, fracture/section evidence and process history |
| Films or foreign material on a machined surface | Oxide or other inclusion | Cleaned surface images and an appropriate material or metallographic examination |
| Raised domes after heating | Blistering | Before/after images, furnace cycle and internal indication evidence |
| Roughness, flash or damaged edges | Tool, coating, trimming or handling condition | Tool/cavity identity, stage of first appearance and agreed visual limit sample |
| Bore, datum or profile out of tolerance | Core shift, distortion, tooling or machining setup | Drawing revision, measurement state, fixture/datum method and a dimensional report |
Gas porosity or shrinkage?
Pore shape and position are clues, not a final diagnosis. Gas-related pores are often rounded; shrinkage commonly concentrates where feeding is inadequate during solidification. Mixed gas and shrinkage mechanisms can occur. Compare geometry and process records with suitable internal inspection or section evidence instead of deciding from one surface photograph.
For detailed pore acceptance, use the aluminum casting porosity inspection guide.
What if the part leaks but no defect is visible?
First separate the part from the test system: verify the fixture, temporary plugs, seals, stabilization and measurement conditions. Once the leak is confirmed and located, relate it to a casting wall, a machined sealing surface or an assembly interface. See the casting leak-test methods guide before selecting a repair or changing the casting process.
Why Casting Defects Matter for Buyers
A useful defect report separates what was observed, which requirement was not met, and which causes still need testing. Preserve the affected part or sample, a scale photograph, the drawing-zone reference and the manufacturing state. Compare affected and acceptable pieces from traceable lots before accepting a corrective-action explanation.
1. Gas Porosity
What It Looks Like Small, round or spherical voids distributed throughout the casting or concentrated near the surface. Often only visible after machining or X-ray inspection.
Root Causes
- Hydrogen absorption from moisture in the melt environment
- Wet or improperly dried tooling and ladles
- Turbulent pouring that entraps air
- Insufficient degassing treatment
Prevention
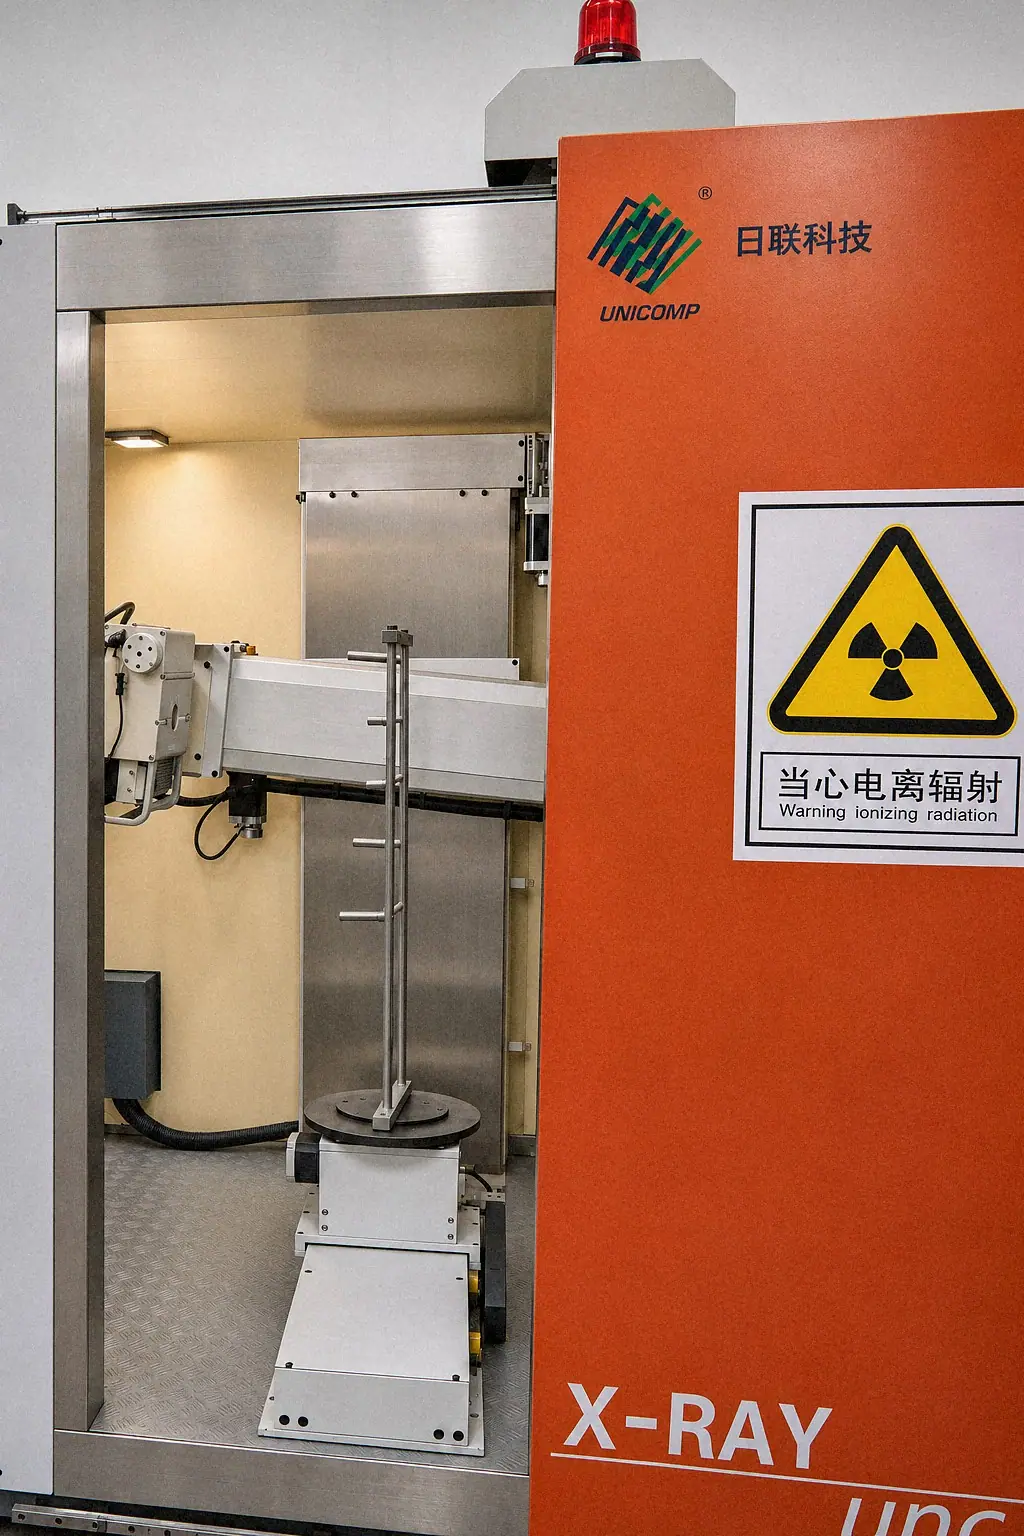
Define melt treatment, temperature control, tooling preparation, and inspection frequency in the project process plan. For project-defined internal inspection, confirmed equipment includes Unicomp UNC-160 and Y.MU2000-D X-ray systems.
Define the inspection zones and acceptance criteria for the project.
At Bohua
Bohua addresses the melt-treatment part of gas-porosity prevention with rotary degassing for 15–20 minutes at 480–520 rpm. The raised baffle supports flux addition and dross removal; lowering it suppresses the vortex for degassing with purge gas. The reduced-pressure sample must have a slightly concave surface and essentially no pores in its cut section to pass Bohua's check. Observed surface flashes are not used to release the melt. The A356 melt-treatment account explains the release checks.
2. Shrinkage Porosity
What It Looks Like Irregular, angular voids typically found in thick sections, junctions or areas that solidify last. Unlike gas porosity, shrinkage voids have rough, dendritic surfaces.
Root Causes
- Insufficient feeding from risers during solidification
- Poor gating design that does not promote directional solidification
- Excessive wall thickness variation in the part design
- Mold temperature too high, delaying solidification
Prevention
During drawing and tooling review, the supplier should identify hot spots, feeding risk, riser placement, gating, and wall-thickness transitions before cutting steel. Any solidification-simulation deliverable should be stated in the project scope rather than assumed as a universal Bohua software workflow.
3. Cold Shuts (Cold Laps)
What It Looks Like Lines or seams on the casting surface where two metal flow fronts met but failed to fuse completely. Often visible without magnification.
Root Causes
- Pouring temperature too low
- Slow fill rate allowing premature solidification of flow fronts
- Poor mold venting trapping air between converging streams
- Overly complex part geometry with long flow paths
Prevention
Controlling pouring temperature within a tight window is critical. In gravity casting, review gating and fill time against the actual flow path and thermal conditions. Mold preheating temperature is adjusted based on part complexity.
4. Misruns (Incomplete Fill)
What It Looks Like The casting is visibly incomplete —thin walls not fully formed, missing features or rounded edges where sharp corners should be.
Root Causes
- Insufficient metal volume poured
- Metal temperature too low for the flow distance required
- Blocked or undersized vents preventing air escape
- Mold coating too thick, insulating and restricting flow
Prevention
Verify the metal quantity, flow distance, vent condition, and coating buildup for the actual tooling.
5. Hot Tears (Hot Cracking)
What It Looks Like Ragged cracks that form during solidification, usually at sharp corners, fillets or where sections change thickness abruptly. The fracture surface appears oxidized and dendritic.
Root Causes
- Mechanical restraint from the mold preventing normal thermal contraction
- Sharp internal corners concentrating stress
- Alloy composition with wide freezing range
- Premature ejection before the casting has cooled enough
Prevention
Review restrained contraction, section transitions, core or die restraint and the timing of part handling. Establish the defect formation stage before changing alloy or process settings. Alloy selection alone does not establish resistance to hot tearing for a particular geometry.
6. Oxide Inclusions
What It Looks Like Thin, irregular films or flakes embedded in the casting. Often found near the surface and exposed during machining. Can cause leak paths in pressure-tight applications.
Root Causes
- Turbulent pouring that folds surface oxide film into the melt
- Dirty or contaminated charge material
- Inadequate skimming before transfer
- Poor gating design that creates splashing inside the mold
Prevention
Review melt handling, free-fall distance, filling behavior, cleanliness and any specified filtration. A gravity-casting label alone does not prove that filling is free of turbulence or oxide entrainment. Confirm the suspected inclusion with an appropriate examination and validate changes on the actual casting route.
At Bohua
Bohua's large-pump volute development involved an A356 casting weighing about 10–15 kg and measuring roughly 0.5 m across. Mold Process Engineer Devin Julia revised the mold and risers several times during that project. Development took more than a year before the castings were accepted and regular cooperation followed.
The investigation linked inclusion indications to incomplete melt cleaning and pinholes to insufficient hydrogen removal. Inadequate feeding remained a possible explanation for other voids. These were project-specific assessments, not a diagnosis rule for every pore. Radiographs and CT images are confidential; the pump-volute case account is a text description.
7. Heat-Treatment Blistering
What It Looks Like Raised surface domes or local swelling that appears during or after solution heat treatment. A blister may indicate trapped gas, local internal discontinuity, or an unsuitable thermal cycle; visual appearance alone does not identify the root cause.
Root Causes to Investigate
- gas or oxide-film defects already present in the casting;
- furnace non-uniformity or a temperature excursion;
- a casting process and pore condition not qualified for the requested solution treatment;
- local wall geometry that responds differently during heating and quenching.
Prevention and Verification
Qualify the casting route and heat-treatment plan together. Link furnace records, heat lot, casting lot, visual findings, and any required section or internal inspection. A blistered part should follow the buyer-approved nonconformance process rather than an assumed universal repair rule. See the T6 heat-treatment guide for the evidence buyers should specify.
8. Surface-Condition Defects
What It Looks Like Surface laps, coating pickup, local roughness, flash, drag marks, or damage that may be cosmetic on one zone and functional on a sealing, coating, or machined zone.
Root Causes to Investigate
- mold coating condition, application, or local buildup;
- worn parting lines, inserts, ejectors, or trimming tools;
- filling or ejection conditions that damage the surface;
- handling, blasting, deburring, machining, or packaging after casting.
Prevention and Verification
The drawing should separate cosmetic zones from functional zones and define the inspection method for each. First-article photographs, visual limit samples, dimensional checks, and surface-finish records can be used when the buyer specifies them.
9. Dimensional Variation
What It Looks Like Parts that pass visual and NDT inspection but fail dimensional checks —out-of-tolerance bores, shifted datums or warped profiles.
Root Causes
- Mold wear or thermal distortion over production runs
- Inconsistent ejection causing part distortion
- Residual stress from uneven cooling or aggressive quenching
- Inadequate fixturing during CNC machining
Prevention
CMM frequency, capability evidence, mold-maintenance records, and heat-treatment verification are defined by the project control plan.
Verification Matrix: Match the Method to the Risk
No single inspection method can prove that every defect type is absent.
| Method | Useful for | Important limitation |
|---|---|---|
| Visual inspection | Surface condition, incomplete fill, obvious cracks or flash | Does not establish internal soundness |
| Dye penetrant | Surface-breaking discontinuities on suitable cleaned surfaces | Does not show sealed internal defects |
| Radiography | Volumetric internal indications in defined zones | Sensitivity depends on geometry, orientation, technique, and acceptance criteria |
| Computed tomography | Three-dimensional internal review and defect location | Cost and scan strategy must match the approval risk |
| Sectioning or metallography | Local destructive confirmation of structure or an indication | Represents only the sampled location |
| Leak or pressure test | Functional leakage under the specified method | Does not identify every root cause or prove mechanical properties |
| CMM, fixtures, or gauges | Dimensional and geometric conformity | Does not establish internal quality |
The RFQ should name the method, risk zone, sampling plan, acceptance criteria, and required record. For pressure-boundary parts, connect the inspection plan to the leak-tight casting route and quality-risk RFQ.
Use this general comparison to select the methods your part needs. For CT or dye penetrant testing, confirm the service route before including either method in your order.
Source: ASNT: Liquid Penetrant Testing.
Source: ASNT: Radiographic Testing.
At Bohua
Routine production typically meets GB/T 11346-2018 Grade 3–4; with tighter process control, sampled parts are around Grade 2; when the customer specifies it, every casting is X-rayed and shipped parts meet Grade 1.
Industrial CT is available through an outside lab.
Agree the inspected zones and acceptance grade for the actual order. A radiographic grade does not replace the specified leak test.
Bohua equipment and inspection boundaries
We have equipment for melt checks, internal inspection, dimensional inspection, and air-under-water immersion testing. Use the project-input column below to specify the checks your part needs.
At Bohua
| Check | Confirmed equipment or test pressure (bar) | Project input |
|---|---|---|
| Melt checks | Oxford optical emission spectrometer; vacuum hydrogen analyzer | Alloy requirement and required records |
| Internal inspection | Unicomp UNC-160 and Y.MU2000-D X-ray systems | Zones, technique, sampling, and acceptance criteria |
| Dimensional inspection | Hexagon Global S and NANO Metrology CMM systems | Datums, critical features, and measurement state |
| Leak testing | Air-under-water immersion; test pressure 3 bar or more | Specify the test pressure in bar, duration, fixture, and acceptance rule |
Bohua has 32 tilt-pour machines and 10 upright gravity casting machines. Impregnation is performed by a qualified subcontractor only with customer approval.

Review Bohua's quality-control equipment and inspection scope and certificate information. Equipment availability and a quality-system certificate do not establish the cause or acceptance of a particular indication; the drawing, approved procedure and part-specific records do.
See Bohua gravity casting capabilities for manufacturing scope.
Questions to Ask Your Casting Supplier
Use these questions during supplier qualification to assess defect prevention capability:
- What degassing method do you use, and how do you validate hydrogen levels?
- Do you run solidification simulation during mold design?
- What is your current internal scrap rate for gravity castings?
- How do you monitor and maintain mold condition during production?
- What NDT methods are available, such as X-ray or air-under-water leak testing?
Buyer Evidence Checklist
Before approving a casting supplier or a corrective action, ask for evidence tied to the drawing and lot:
- defect name and precise location, not only a general scrap label;
- detection method, equipment or procedure reference, and acceptance basis;
- affected heat, tool, cavity, date, shift, and machining stage where traceability permits;
- containment scope and disposition of affected material;
- confirmed root cause versus hypotheses still under investigation;
- corrective action, validation evidence, and ongoing control-plan change;
- photographs, radiographs, dimensional records, or functional-test records required by the buyer.
Buyer questions
Is all porosity automatically rejectable?
No. Acceptance depends on location, size, distribution, function, machining exposure, drawing requirements, and the agreed inspection standard.
Can X-ray find every aluminum casting defect?
No. Detection depends on geometry, indication orientation, technique, sensitivity, and acceptance criteria. Surface-breaking, dimensional, and functional risks may need different methods.
Why do some defects appear only after machining?
Machining can expose near-surface pores, inclusions, or discontinuities that were covered by the as-cast skin. The RFQ should therefore connect machining stock and critical faces to the inspection plan.
Should impregnation be treated as the default porosity fix?
No. Whether impregnation is permitted is a buyer and drawing decision. It does not replace root-cause review, and it must not be used to imply that structural or process requirements have been met.
Record One Problem Before Choosing a Corrective Action
Record the observed symptom, acceptance requirement, affected population, hypotheses, verification method and corrective-action result. Leave an unverified cause marked as a hypothesis.
For a pump housing, connect the defect location to the fluid wall, seal chamber and machined faces. For a valve body, identify the affected passage, port or sealing interface. Use the RFQ preparation worksheet when the investigation becomes a new or replacement casting project.
For a coolant water outlet casting review, mark the fluid wall, machined seals, and defect location on the drawing. For process-specific diagnosis, use LPDC defect troubleshooting. For purchase acceptance, use die casting defect acceptance and inspection planning.
Technical References and Scope
These are technical references, not Bohua customer case results. Confirm the applicable inspection standard and acceptance criteria for the actual part.
Source: ASM Handbook, Volume 15, Casting (2008): Common Defects in Various Casting Processes.
Send drawings and inspection requirements
Include the drawing revision, alloy, annual volume, critical zones, and required inspection records. Submit the RFQ details, then email your drawing for a structured quote review. Send the drawing, target alloy, finishing scope, MOQ, and delivery timing. Bohua will review it like a real sourcing project, not a generic contact request. Our engineering team can recommend the right alloy, process, and design optimizations for your specific requirements.
Send your drawing →